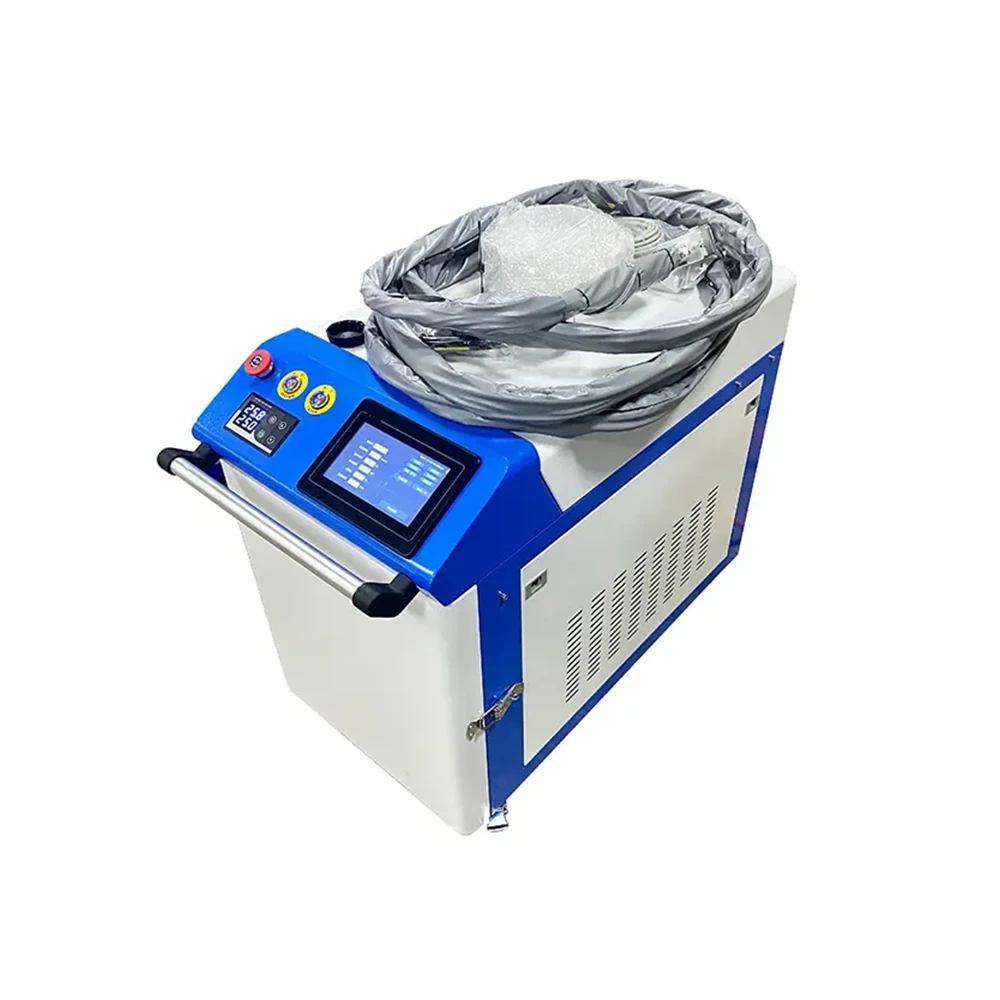
3000W High-Power Laser Cleaner
Half the average power in a water-cooled platform, with a 300 mm beam and a 10 m standard cable.
View modelBuilt for surfaces measured in hundreds of square metres, where a portable cleaner would take weeks. This continuous-wave station delivers 6000W of cleaning power through a beam up to 300 mm wide, stripping multi-layer marine coatings, heavy corrosion and mill scale in a single pass at rates a 2000W or 3000W system cannot approach. A dual-loop chiller keeps it running at 100% duty cycle through the whole shift, with HEPA and carbon filtration capturing the fume on board.
On a hull, a tank farm or a bridge, the schedule is set by how many square metres can be prepared in a shift. Tripling the average power changes what is possible within the same working window.
Indicative rates by contaminant type and thickness. Single-pass figures unless a double pass is noted.
| Contaminant | Typical Thickness | Cleaning Rate (m²/h) | Method |
|---|---|---|---|
| Light surface rust | Under 50 µm | 100–120 | Single high-speed pass |
| Medium rust | 50–100 µm | 65–75 | Single pass |
| Heavy corrosion spots | 100–200 µm | 35–45 | Single or double pass |
| Hot-rolled mill scale | 30–80 µm | 80–100 | Single pass |
| Single-layer coating | 50–150 µm | 40–60 | Single pass |
| Multi-layer coating | 200–500 µm | 20–35 | Single or double pass |
| Marine epoxy coating | 200–400 µm | 25–40 | Single pass |
| Oil and grease film | Surface film | 120–150 | Single high-speed pass |
| Weld discoloration and oxide | Thin | 60–80 | Single pass |
Rates are indicative and depend on material, accessibility and the surface finish required. A free test on your own sample confirms the achievable throughput.
Throughput only counts if it lasts. Every major subsystem is chosen for round-the-clock industrial duty.
Continuous operation through a full shift without the power derating that limits smaller systems on long jobs.
A 12 kW chiller with separate circuits for source and optics holds a steady thermal window at up to 40 °C ambient.
A sealed laser source with active temperature monitoring and fault diagnosis for dusty and humid environments.
Three-stage cyclonic, HEPA and carbon filtration captures fume at source, with pulsed-jet cleaning to extend filter life.
The station is assembled from industrial modules so each part can be serviced without taking the whole system out of production.
A 6000W continuous-wave fiber source with adjustable output from 10% to 100%, M² below 1.3 and stability within ±1.5% over eight hours.
A galvanometer head weighing 3.5 kg with quick-change focus lenses at 200 mm, 300 mm and 500 mm, plus an assist-gas nozzle.
12 kW of cooling capacity with separate circuits for source and optics, holding ±1 °C and shutting the laser down on flow loss.
Cyclone pre-separator, HEPA filter rated to 99.99% at 0.3 µm, and an activated carbon stage for volatile organic compounds.
A powder-coated steel cart on heavy locking castors carries the station, with an integrated cable reel and strain relief to protect the fiber and storage compartments for spare lenses, nozzles and tools.
A 15-inch industrial touch screen runs preset and manual modes with 100 user-configurable job profiles, so a shelf of part numbers can be cleaned without re-entering parameters.
Both processes remove contamination. The difference is whether average power or thermal control matters more on your parts.
| Factor | Pulsed Laser | Continuous Wave (CL-6000-HC) |
|---|---|---|
| Peak Power | Very high, in the megawatt range | Moderate at 6 kW average |
| Average Power | Low to medium, 100–1000W | High at 6000W |
| Heat Build-Up | Minimal | Low, managed by scan speed |
| Material Selectivity | Good | Excellent |
| Speed on Thin Layers | Good | Better |
| Speed on Thick Layers | Limited | Excellent |
| Surface Finish | Lightly textured | Smooth and uniform |
| Sensitivity to Reflectivity | High | Moderate |
| Large Area Suitability | Limited | Excellent |
For delicate parts where a temperature peak must be avoided entirely, choose a precision pulsed model. For heavy coatings on large steel, continuous wave wins on throughput.
Four design choices turn 6000W of power into square metres per hour on the shop floor.
A high-speed closed-loop mirror system rasterizes the beam in a controlled pattern instead of relying on hand movement alone.
Scan width up to 300 mm covers a wide swathe in a single pass, so fewer overlapping strokes are needed.
Focus spot size is matched to the contamination thickness and material so energy is spent on the layer being removed.
Compressed air or nitrogen carries ablated material away, preventing redeposit and keeping the cleaned surface clear.
Three sectors account for most 6000W installations, and each one chooses it for a different reason.
Hull cleaning, deck preparation, ballast tank corrosion removal and weld cleaning. Hull areas run into hundreds or thousands of square metres, and only a high-speed system finishes within the docking window. Zero media means nothing discharges into the dry dock or waterway.
Rolled mill scale, plate rust and weld zone cleaning before coating. Uniform cleaning across large plates gives predictable coating adhesion, and because there is no abrasive contact the material is not thinned.
External pipe cleaning, weld cleaning, flange preparation and coating removal in remote locations where transporting blasting media and water is impractical and zero discharge is a regulatory advantage.
Large systems are commissioned with the customer, and support continues for the life of the machine.
Standard configuration in 15 to 20 working days; premium source or cable options in 30 to 45 working days.
Two to three days of training at delivery covering hazards, PPE, work zone control and emergency procedures.
Two years on the laser source, one year on all other components, with extended warranty options available.
Phone, email and remote diagnostics support for the life of the machine, wherever the system is installed.
The system draws its power from a three-phase 380 V supply. Consumables are limited to the protective lenses, which typically last 500 to 2000 hours, the fume extraction filters, and an annual water change with filter cleaning on the chiller. There are no abrasive media, no chemicals and no process water to buy or dispose of.
Yes. The CL-6000-HC is designed for both indoor and outdoor work, and its IP65 sealed laser source resists dust and moisture while the scanning head is weather resistant. For extended outdoor use we recommend an additional protective canopy.
All operators must complete laser safety training covering hazard identification, personal protective equipment, work zone control and emergency procedures. We provide comprehensive training at delivery over two to three days and recommend an annual refresher.
A standard configuration ships in 15 to 20 working days. Premium configurations such as an IPG or JPT laser source and longer cables may take 30 to 45 working days.
The laser source is covered for two years and all other components, including mechanical, electrical, cooling and fume extraction parts, for one year. Lifetime technical support is provided by phone, email and remote diagnostics, and extended warranty options are available.
Yes. We offer a free sample test. Send us your material and we will clean it with the CL-6000-HC, provide a video of the cleaning process and return the cleaned sample so you can evaluate the result. There is no obligation.
Large industrial surfaces where area coverage per hour matters: ship hulls, decks and ballast tanks, storage tanks, bridges, pipelines, offshore platforms and wind turbine towers, including surface preparation for coating, welding or inspection.
If the surface area is smaller or the parts are more delicate, these models from the same range may fit better.
Half the average power in a water-cooled platform, with a 300 mm beam and a 10 m standard cable.
View model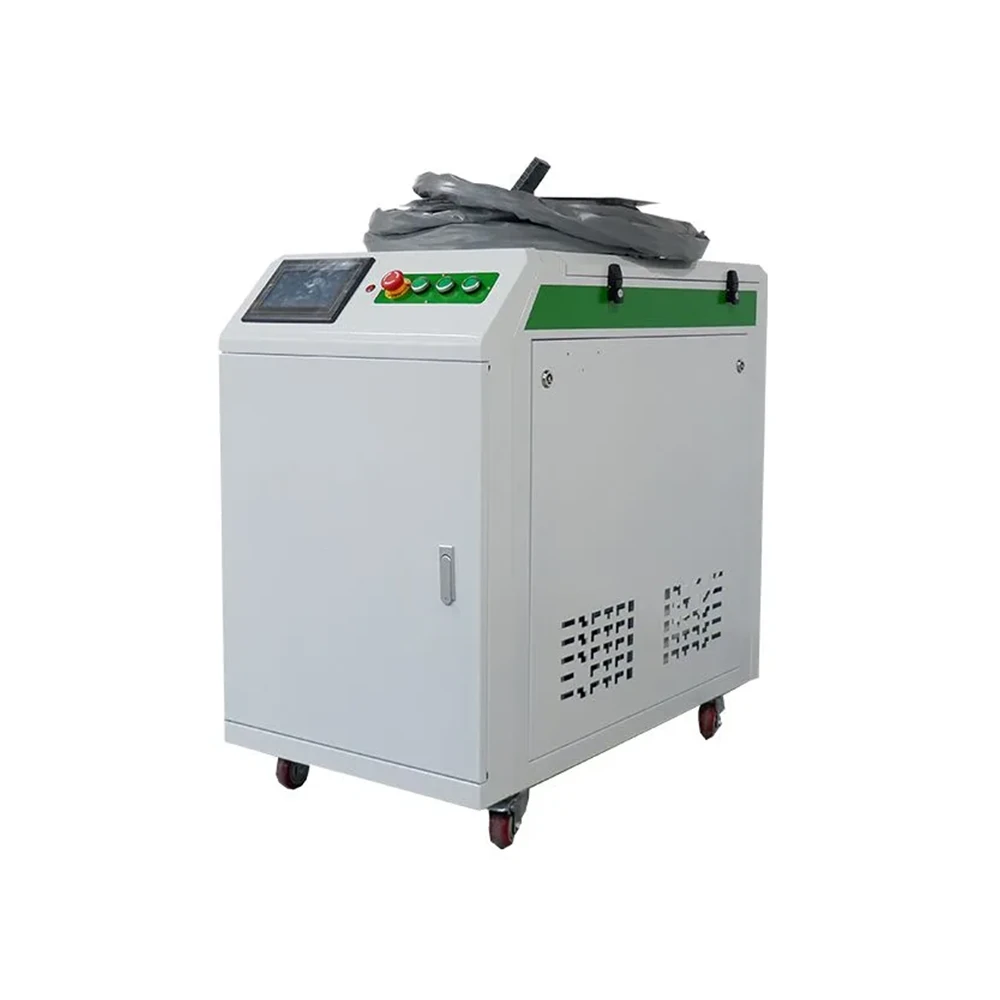
Pulsed 500W to 1000W output for parts where thermal influence must be avoided completely.
View model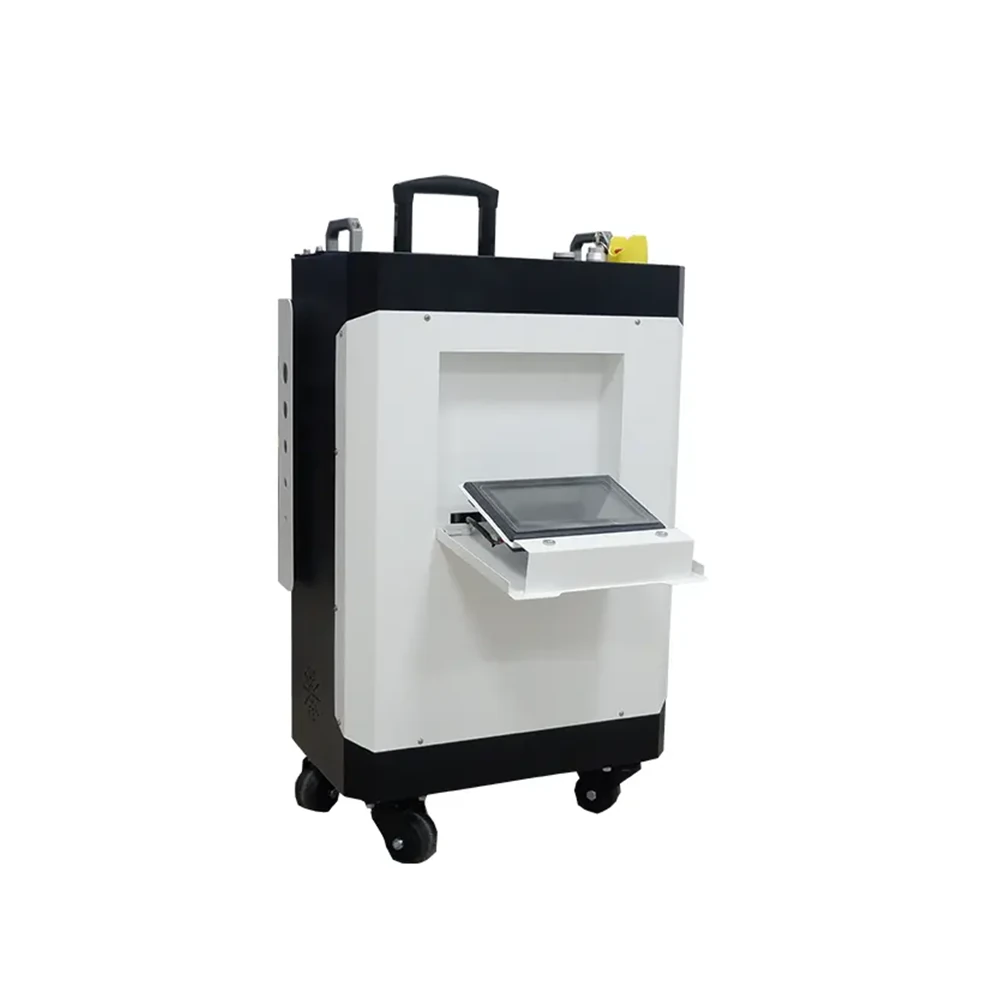
A 0.85 kg pull-rod gun for pipes, dies and flanges that the wide head cannot enter.
View model