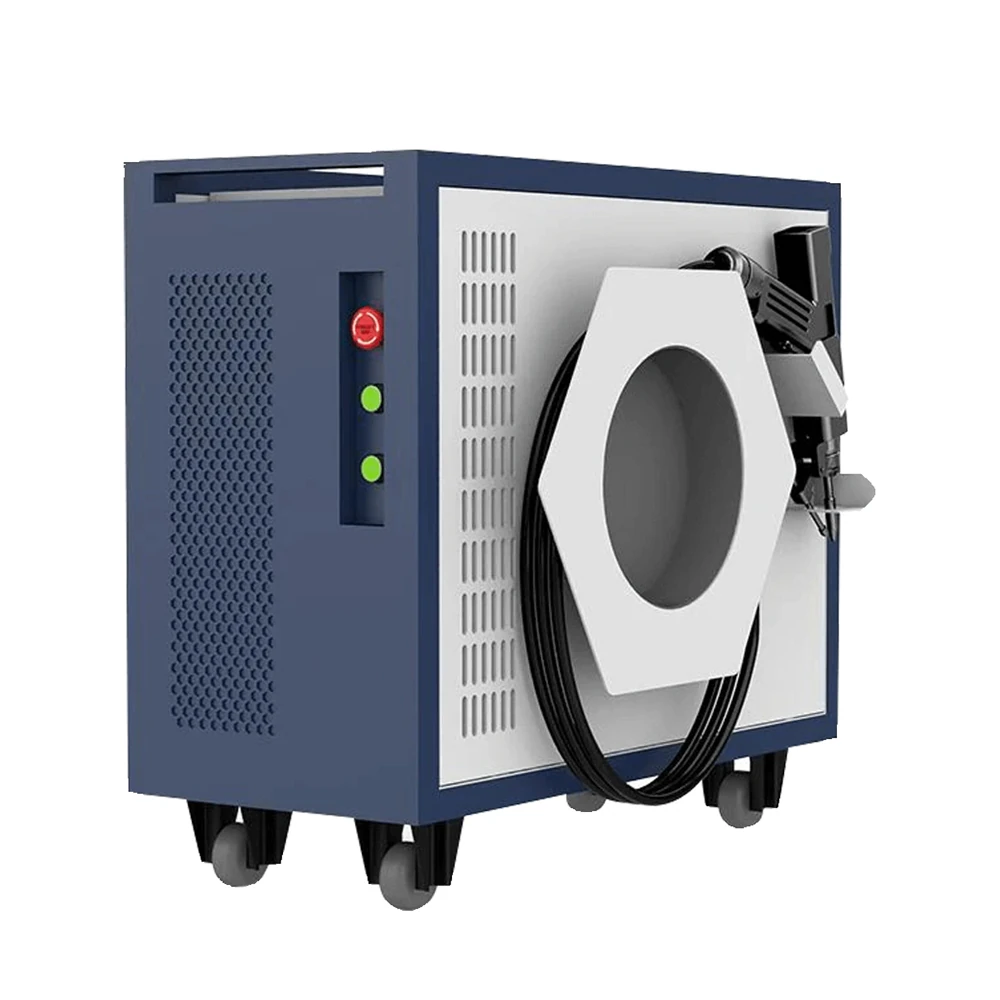
Air-Cooled Handheld Laser Welding Machine
800W to 2000W with a fan-and-heatsink cooling loop instead of a chiller. The lightest four-in-one build at 55 kg, made for field welding and site repair.
View detailsOne 1080 nm fiber source, four tools, one cabinet. These four-in-one systems weld, clean, cut and finish a seam without sending the part to a second machine — so a fabricator can buy one platform instead of four. Choose a handheld build for reach, a split-cabinet build for cooling headroom, or an air-cooled build for site work.
A weld is never a single operation. The joint is cleaned before the beam touches it, welded in one pass, and dressed afterwards so the seam matches the surrounding surface. Four-in-one systems keep all of that in one work envelope instead of moving the part between a welder, a grinder and a cleaning booth.
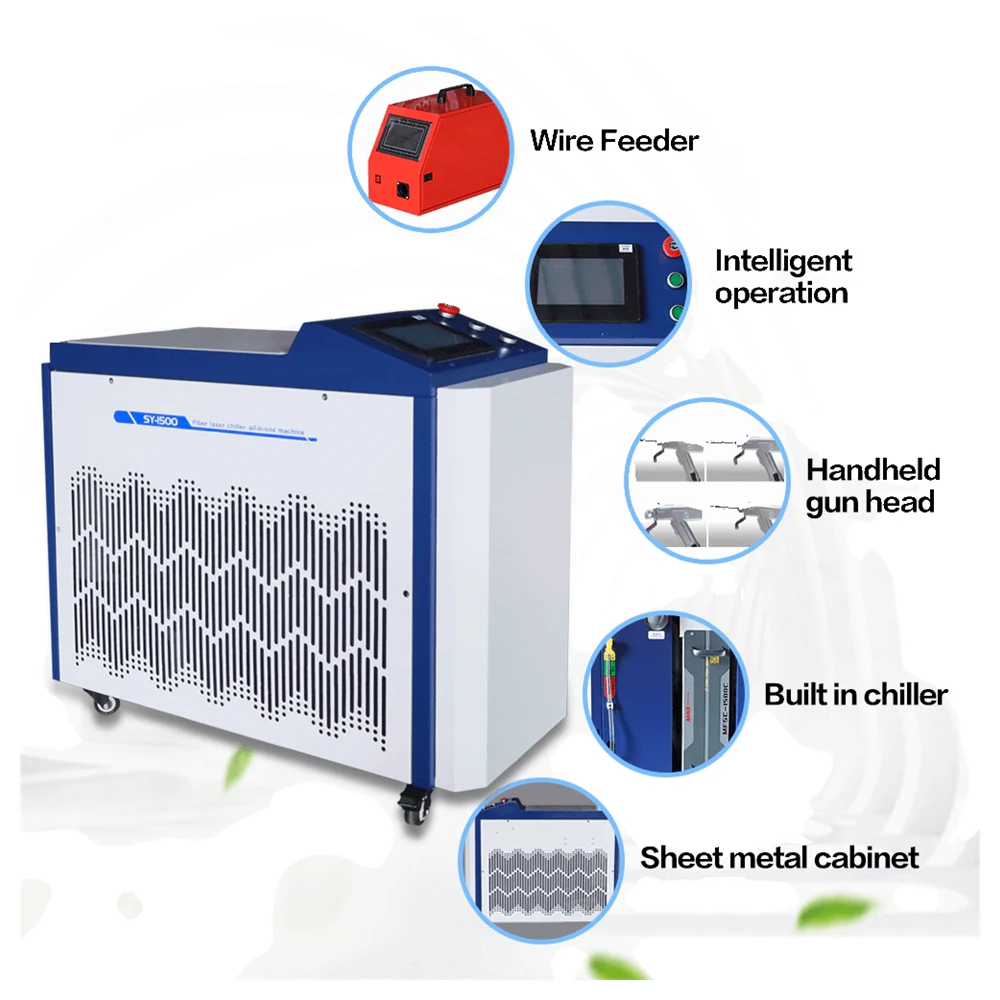
Strip rust, oil and coating from the joint line with the cleaning head before welding.
Lay the seam with the wobble head, adding filler wire where the joint calls for it.
Trim, slot or free thin sheet with the cutting head when a part needs shaping.
Dress the seam with the seam-cleaning head to remove tint and spatter.
Every unit below shares the wobble head, wire feeder and four-function platform. They differ in cooling, cabinet layout, weight and the level of customisation.
800W to 2000W with a fan-and-heatsink cooling loop instead of a chiller. The lightest four-in-one build at 55 kg, made for field welding and site repair.
View details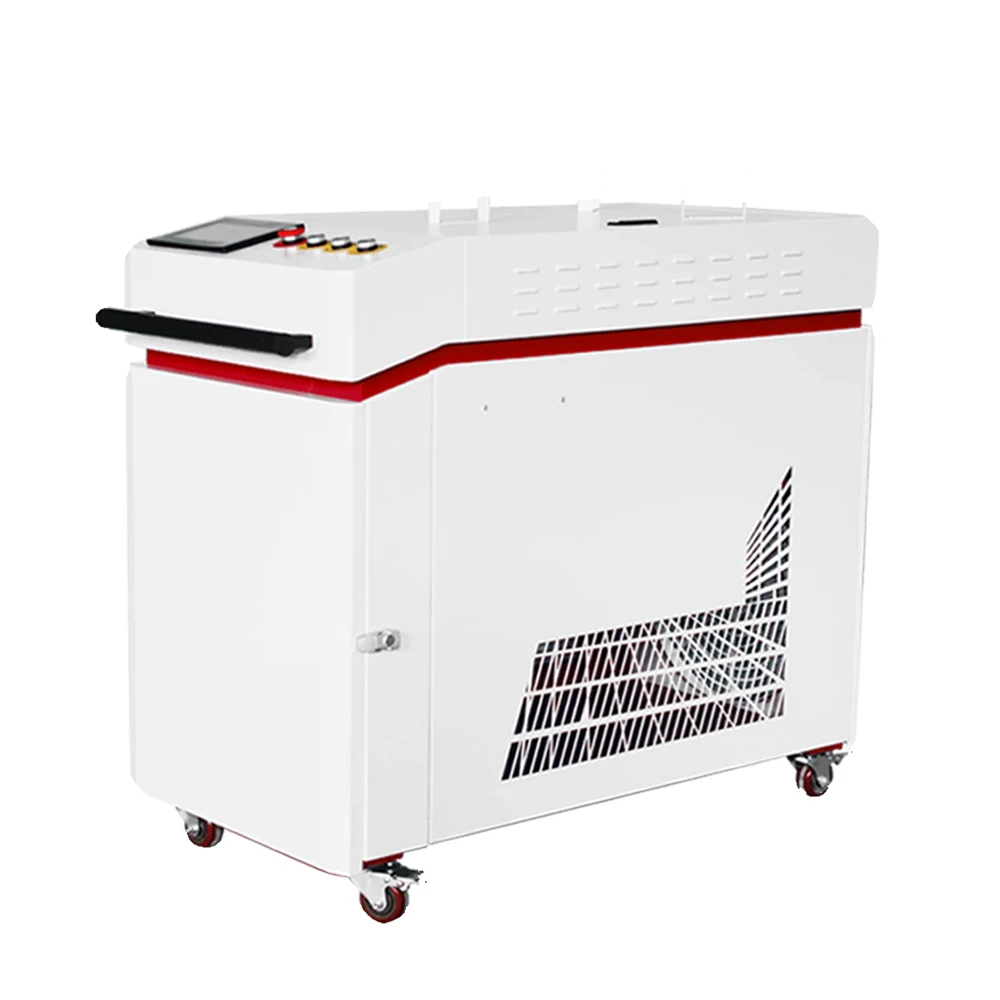
Source and water chiller sit in separate cabinets for cooler continuous duty and easier service access. 1 kW to 2 kW, 125–134 kg.
View details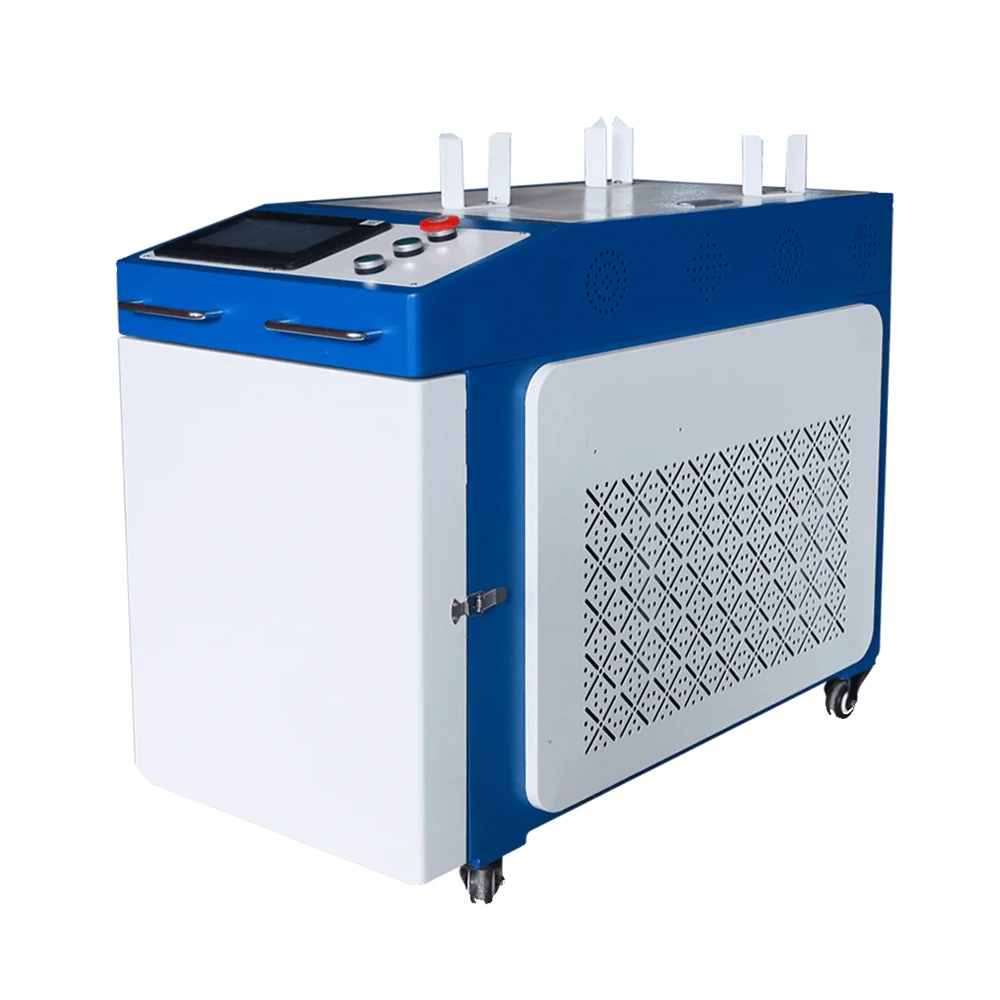
The value build: a water-cooled four-in-one from 1500W to 3000W with single or dual wire feed and a 19-language control system.
View details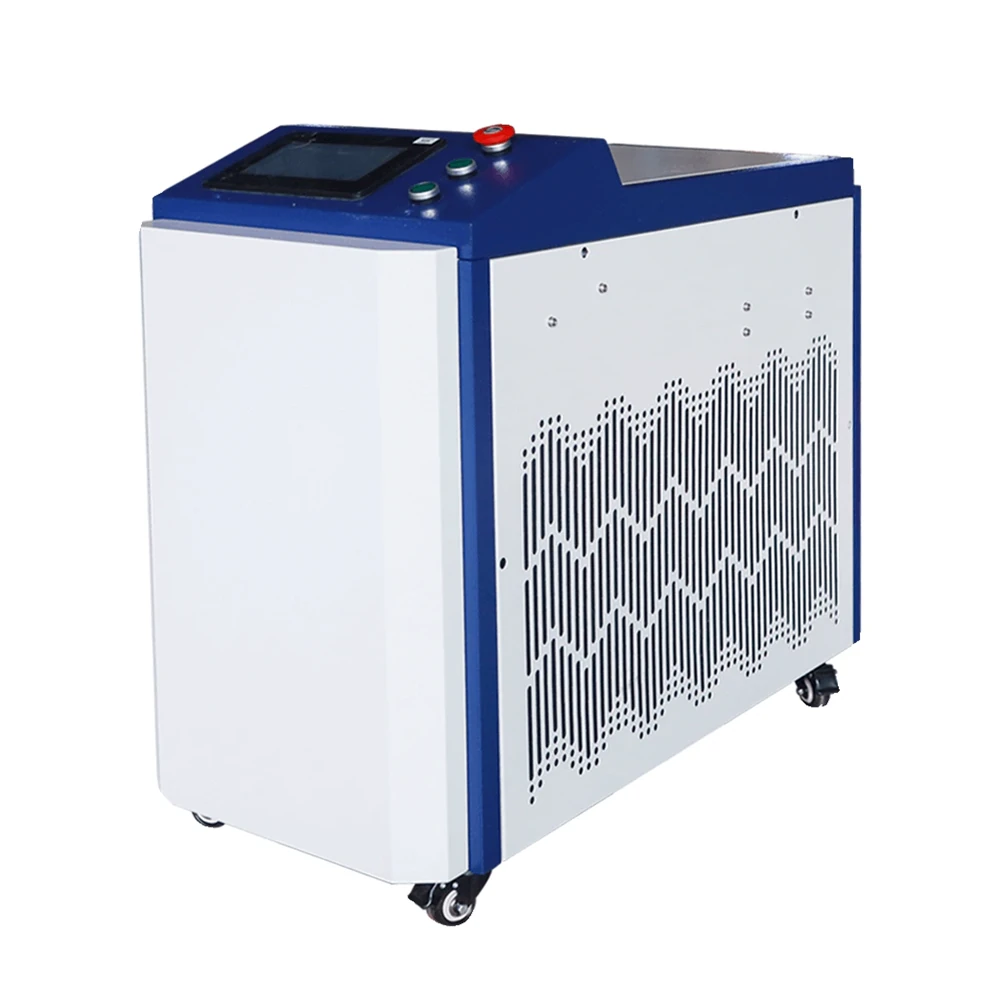
Hanli chiller integrated inside the cabinet, three wobble scan modes and a smart optical-path protection system. 65 kg.
View details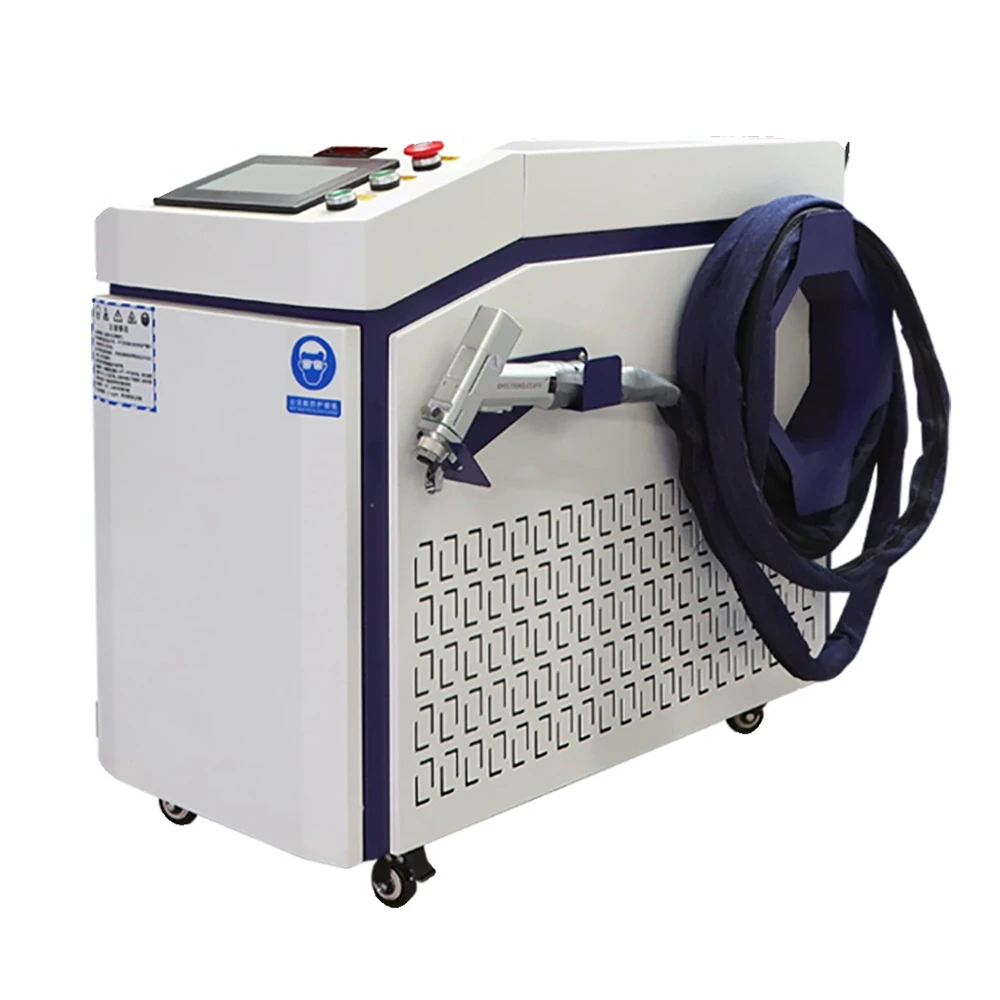
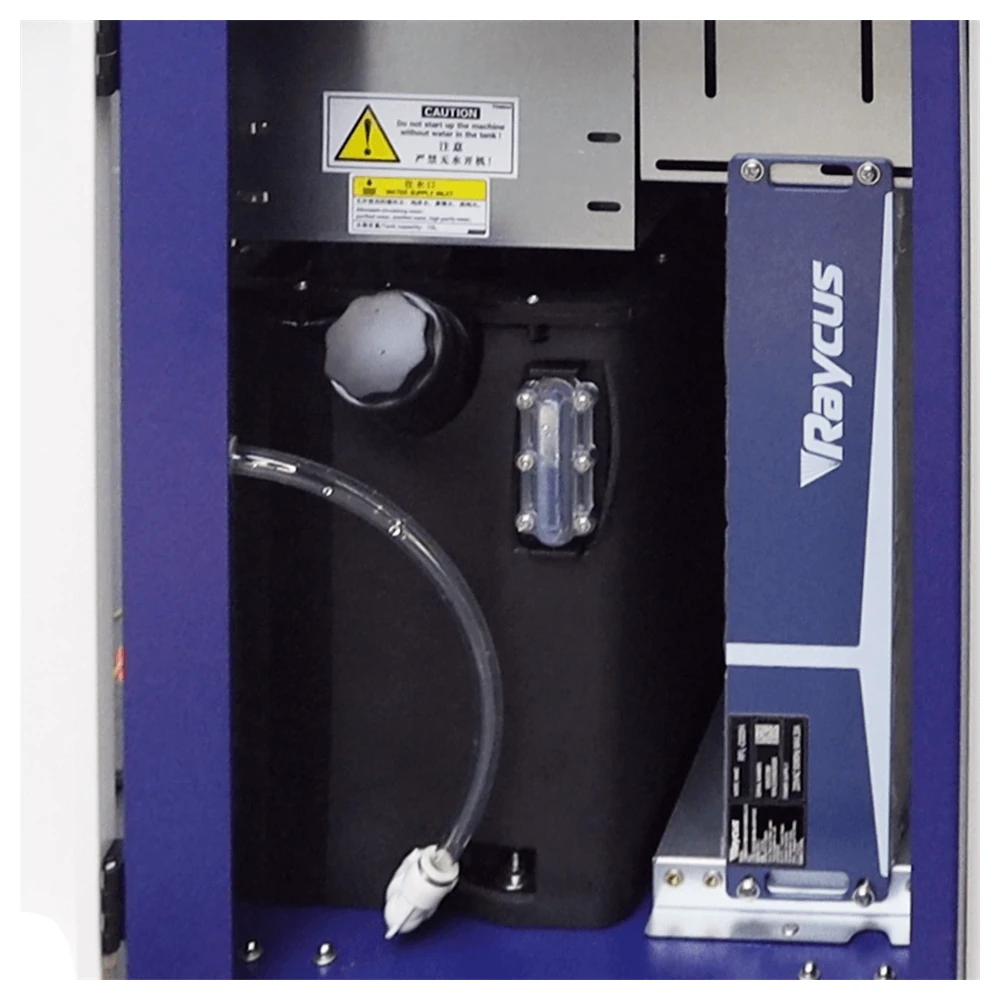
An S&A CWFL dual-circuit chiller holds the loop within about half a degree for stable, all-day welding. 77 kg cabinet.
View details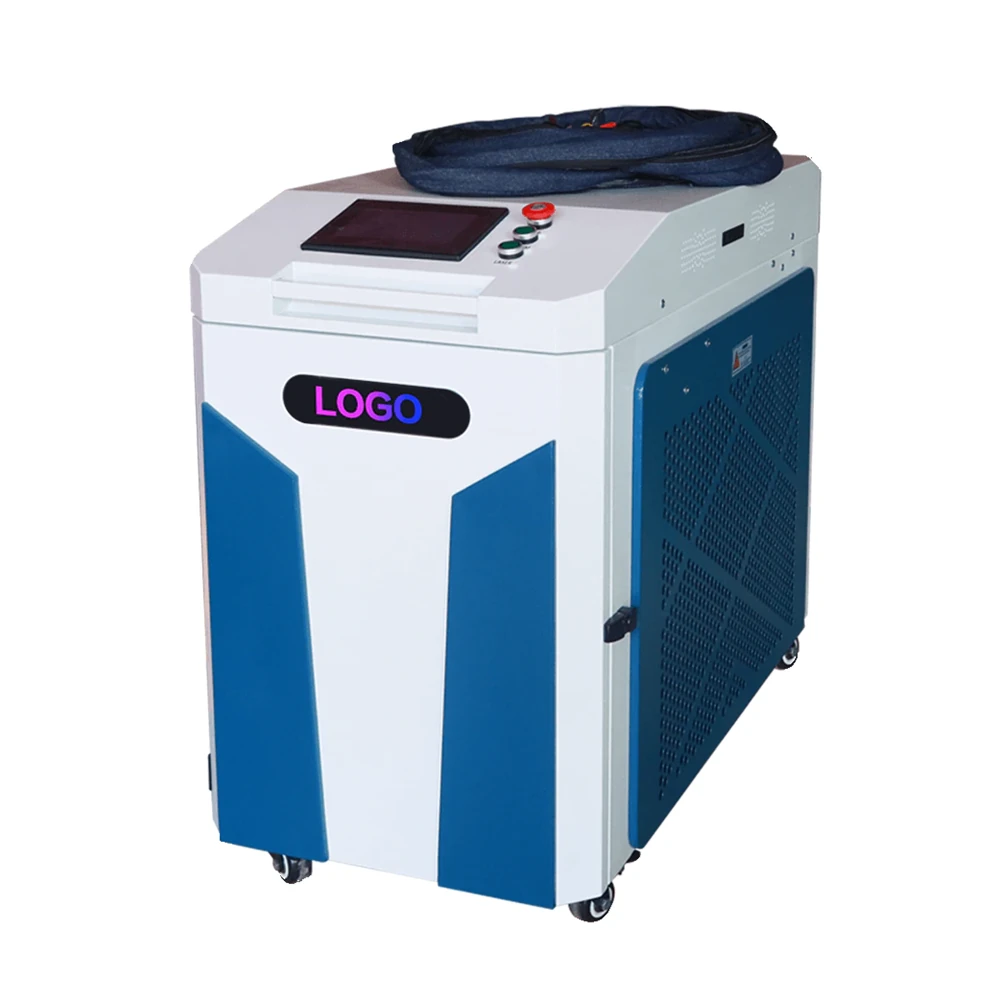
Built around your brand: an illuminated logo, custom nameplate, housing colour and interface language on a 1500W to 3000W platform.
View detailsPick the row that matches your work, then confirm the power level against the material thickness you weld. Figures below come from the machine datasheets.
| Parameter | Air-Cooled Handheld | Split-Type | Economical | Hanli Handheld | S&A Handheld | Customizable |
|---|---|---|---|---|---|---|
| Model series | KR-LW800A – 2000A | KR-LW1500S – 3000S | KR-LW1500E – 3000E | KR-LW1500H – 3000H | KR-LW1500S – 3000S | KR-LW1500C – 3000C |
| Laser power | 800W / 1200W / 1500W / 2000W | 1000W / 1500W / 2000W | 1500W / 2000W / 3000W | 1500W / 2000W / 3000W | 1500W / 2000W / 3000W | 1500W / 2000W / 3000W |
| Laser source | BWT / Raycus / Max | Raycus / MAX / BWT | Raycus / Reci / BWT / Max | Raycus / Reci / BWT / Max | Raycus / Reci / BWT / Max | Raycus / Reci / BWT / Max |
| Cooling method | Air-cooled | Separate water chiller | Water-cooled | Hanli water chiller | S&A dual-circuit chiller | Water-cooled |
| Cabinet layout | One compact cabinet | Source and chiller in two cabinets | Chiller inside the cabinet | Chiller inside the cabinet | Chiller inside the cabinet | Chiller inside the cabinet |
| Machine weight | 55 kg / 58 kg | 125 kg / 134 kg | 109.2 kg | 65 kg | 77 kg | 80 kg |
| Welding gun weight | About 1 kg | Handheld gun included | 0.75 kg | 0.75 kg | 0.75 kg | 0.75 kg |
| Wire feeding | Single wire | Single or dual wire | Single or dual wire | Wire feeder included | Single or dual wire | Single or dual wire |
| Functions | Four-in-one: laser welding, laser cleaning, laser cutting and weld-seam cleaning on one platform | |||||
| Standout feature | No chiller, 55 kg portable | Best cooling headroom and service access | Lowest entry to 3000W water-cooled welding | Three wobble scan modes with optical-path protection | Tightest temperature stability for continuous duty | Full brand customisation with illuminated logo |
Air-cooled output is listed as 800W, 1200W, 1500W and 2000W from the datasheet, while the top model is named KR-LW2000A. Filler wire, fiber length and gun configuration are confirmed per order. Ask us for a datasheet matched to your material and thickness.
The same wobble head covers most joint types by changing the oscillation pattern, the travel speed and the wire feed rate. Nothing about the cabinet changes.
A linear or circular wobble spans the joint, so a gap of up to 0.5 mm is bridged in a single pass with a flat, bright bead.
A wider rectangular wobble spreads energy across the fillet leg; wire feed builds the throat without slowing travel.
Short timed pulses tack thin sheet without burn-through, then a continuous pass finishes the run.
Low heat input limits distortion when steel meets aluminium or brass, with wire matching the joint requirement.
Four functions matter most where cleaning, welding, trimming and finishing already happen in the same cell.
Body panels, brackets and exhaust work, where pre-clean and a bright finish matter as much as the weld itself.
Kitchen equipment, railings and tanks that must ship bright, with the seam-cleaning head replacing acid pickling.
Cabinets, panels and covers, where the cutting head trims and slots and the welding head closes the corner.
Thin-walled and heat-sensitive assemblies that need low distortion and a repeatable, code-controlled bead.
Frames, tubes and structural parts welded at 2000W to 3000W, with dual wire feed for thicker sections.
Installed equipment and site repairs, where the air-cooled build travels and needs no water circuit.
One 1080 nm fiber source drives four tools: a wobble welding head, a cleaning head for pre-weld surface preparation, a cutting head for thin sheet, and a seam-cleaning head that removes discolouration after welding. You change the head and the recipe while the main cabinet, chiller and wire feeder stay in place.
The wobble head oscillates the focused spot at up to 20,000 mm/s in a circular, rectangular or linear pattern. That stirs the melt pool, widens the seam, reduces porosity and lets one pass bridge a joint gap of up to 0.5 mm, so parts need less fit-up work than with a fixed spot.
Add filler wire when the joint has a gap, when you are welding thicker sections, or when you want a built-up fillet. Single wire suits standard butt and lap welds, while dual wire feeds two wires at once to raise deposition on thick material.
Yes. Argon or nitrogen shields the melt pool from oxygen, which keeps the seam bright and prevents porosity. Flow is set per material and thickness, and the gun delivers gas concentrically around the beam.
Air-cooled units use fans and heatsinks, weigh around 55 kg and suit site work, maintenance and light sheet. Water-cooled units use a closed chiller loop, hold temperature to within about half a degree and support higher power for continuous, all-day production.
Stainless steel, carbon steel, aluminium, copper and galvanised sheet are all supported. Aluminium and copper reflect more of the beam, so they are usually welded at higher power with a slightly different focus and gas setting.
Standard production is about five working days, with express transit adding roughly four to six working days. Every machine carries a 2-year warranty with free replacement parts, English online support and lifetime technical help. Volume terms are agreed per order.