CNC Router & Engraving Machines
Gantry routers and stone engraving machines for wood, panel, acrylic, composite and stone. 3–9 kW spindles, 1300–2000 mm X travel, vacuum and T-slot tables, 4th-axis rotary option. 6 models.
View the rangeOne CNC platform, four ways to remove material. Gantry routers and stone engraving machines shape sheet, panel and stone; vertical machining centres and gantry mills hold tolerances on hardened metal; flat-bed and 45° slant-bed lathes turn shafts and discs; plasma, flame and bevel cutting platforms profile steel plate. Every line shares the same house standard — servo drives, preloaded ball screws, industrial CNC control and a measured accuracy report before shipment.
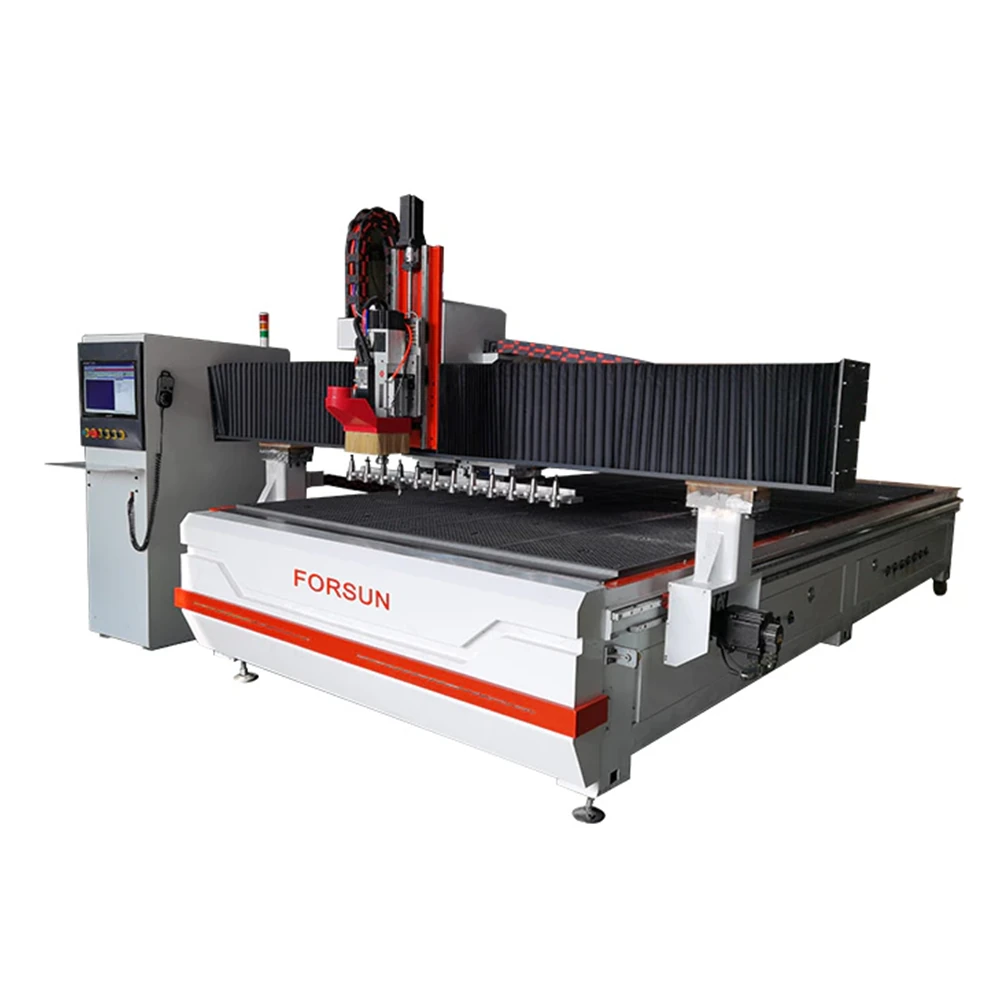
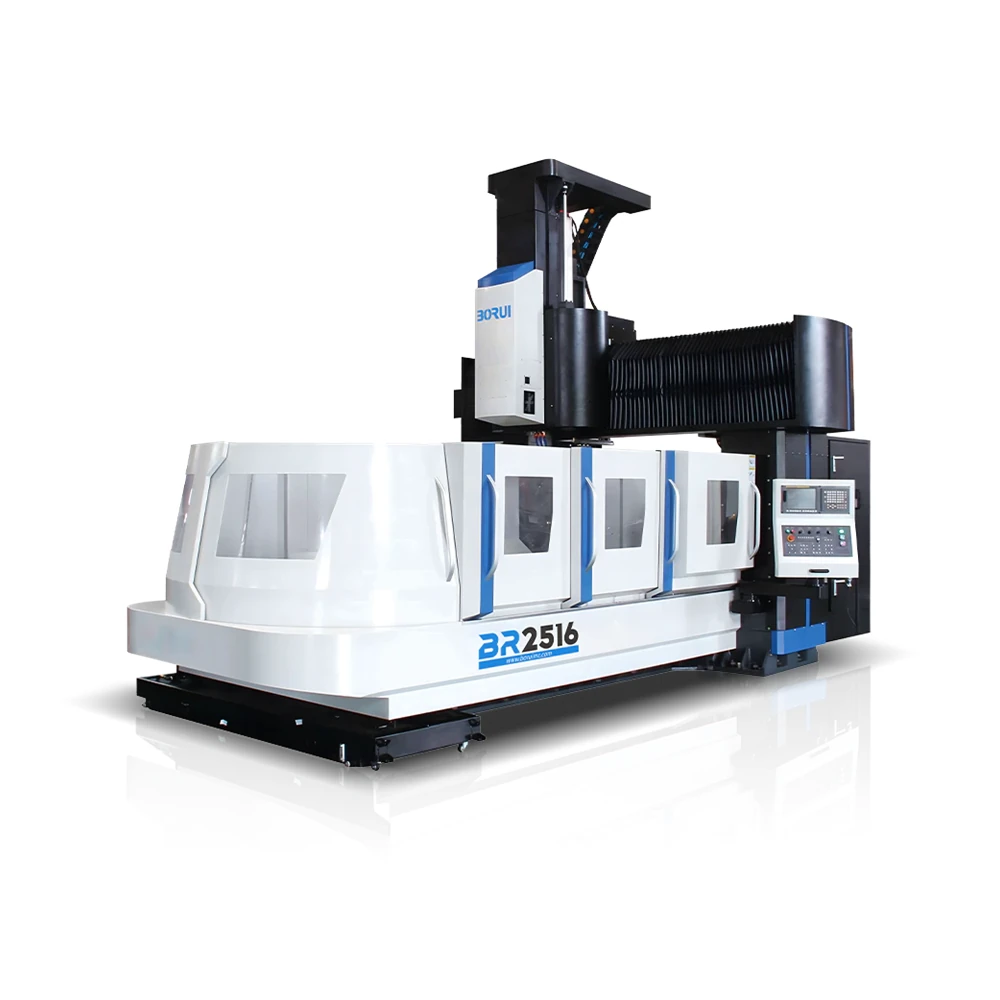
The four lines are not rebadged versions of each other. A router carries a moving gantry over a vacuum table; a machining centre carries a spindle head on hardened linear guides inside an enclosure; a lathe turns the work against a turret; a cutting platform moves torches over a plate bed. What they do share is the drive train, the metrology and the documentation.
Choose the line by the part you have to make. Within each line the travel, spindle, tool magazine and control can be re-specified against your drawing.
Gantry routers and stone engraving machines for wood, panel, acrylic, composite and stone. 3–9 kW spindles, 1300–2000 mm X travel, vacuum and T-slot tables, 4th-axis rotary option. 6 models.
View the rangeVertical machining centres, bridge-column mills, drilling and tapping centres and gantry mills. 600–4000 mm X travel, BT40 and BT50 tapers, 16 to 24 tool magazines. 7 models.
View the rangeFlat-bed and 45° slant-bed turning centres for shafts, bushings, fittings and hydraulic parts. 400–600 mm swing, 4–8 tool stations, hydraulic chucks and turn-mill options. 4 models.
View the rangeFlame, plasma, bevel and rotary multi-torch platforms for steel plate from 1 to 300 mm. Nesting software, automatic gas control and optional marking heads. 4 models.
View the rangeSix gantry machines covering two very different jobs: nesting and carving sheet material with vacuum tables and automatic tool changers, and driving a high-torque water-cooled spindle through marble, granite and ceramics. In between sit multi-head machines that double output per cycle and a four-axis machine for cylindrical and full 3D forms.
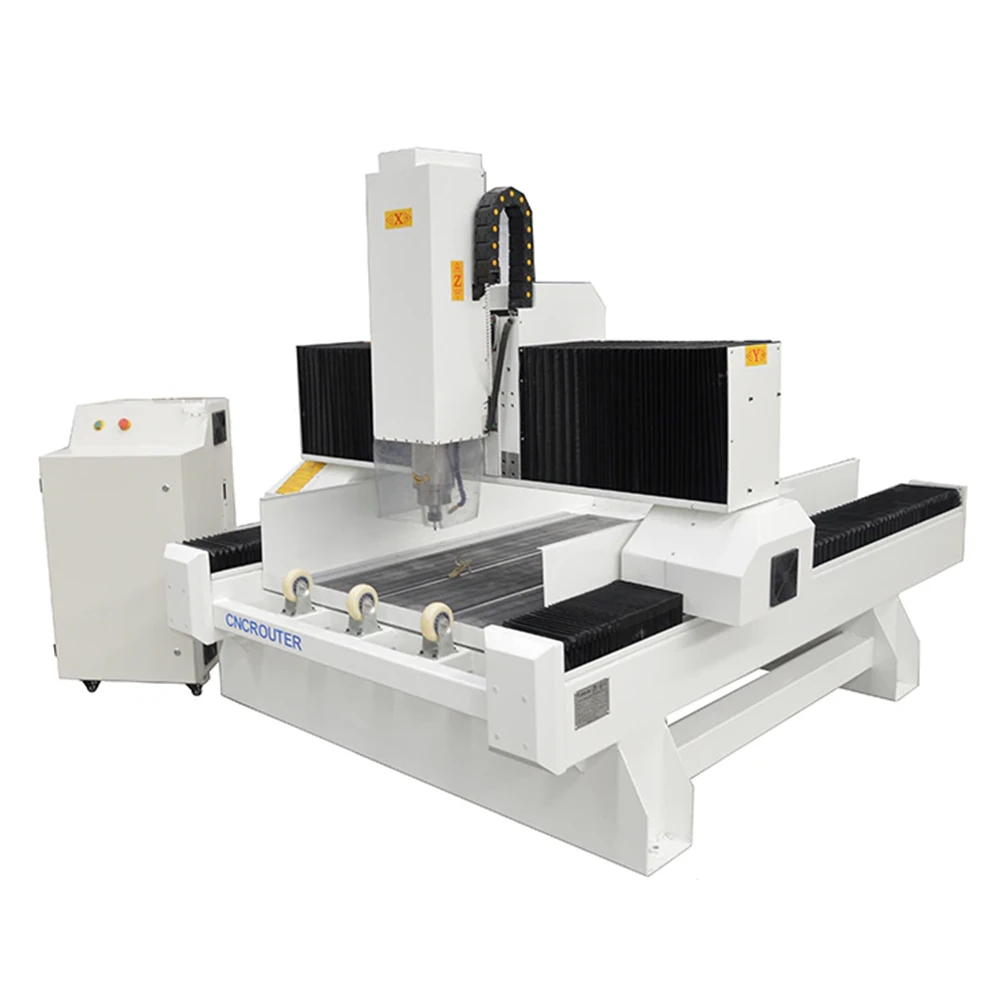
1300×1300 mm stone bench with a 5.5 kW 24,000 rpm spindle, constant-power cutting and inward and outward tool cooling for lettering and reliefs.
View details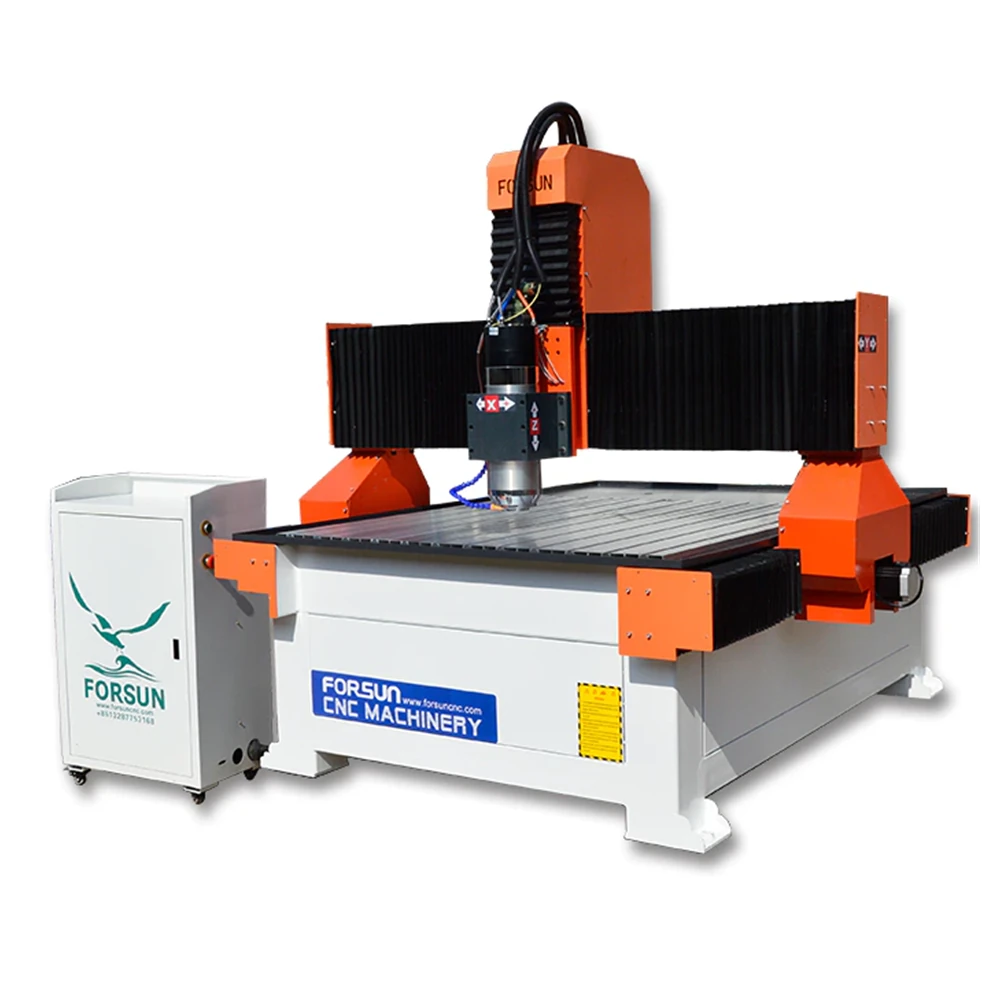
Reinforced frame and stone spindle on a 1300×2500 mm table with 7.5-inch gantry clearance, two safety laser curtains and an optional ATC head.
View details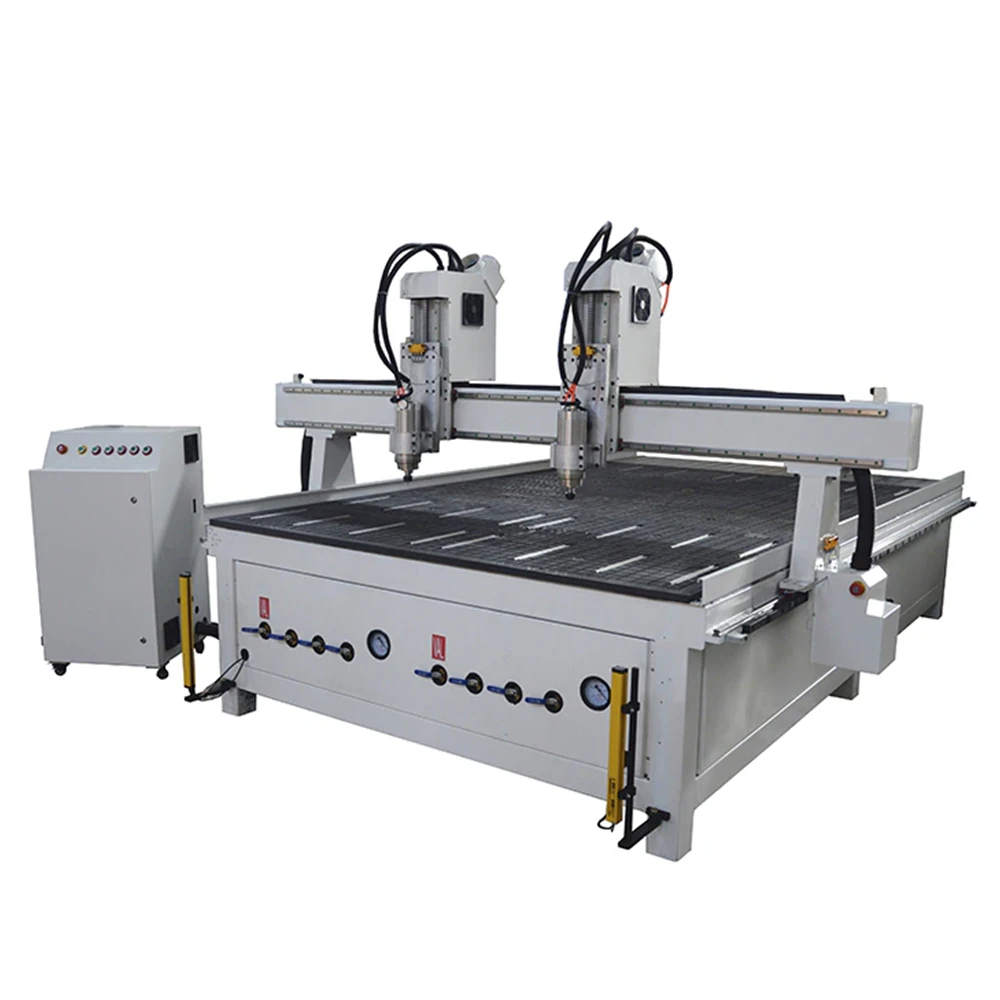
Twin 4.5 kW heads cutting the same pattern at once to roughly double small-part output, or running independently for mixed batches.
View details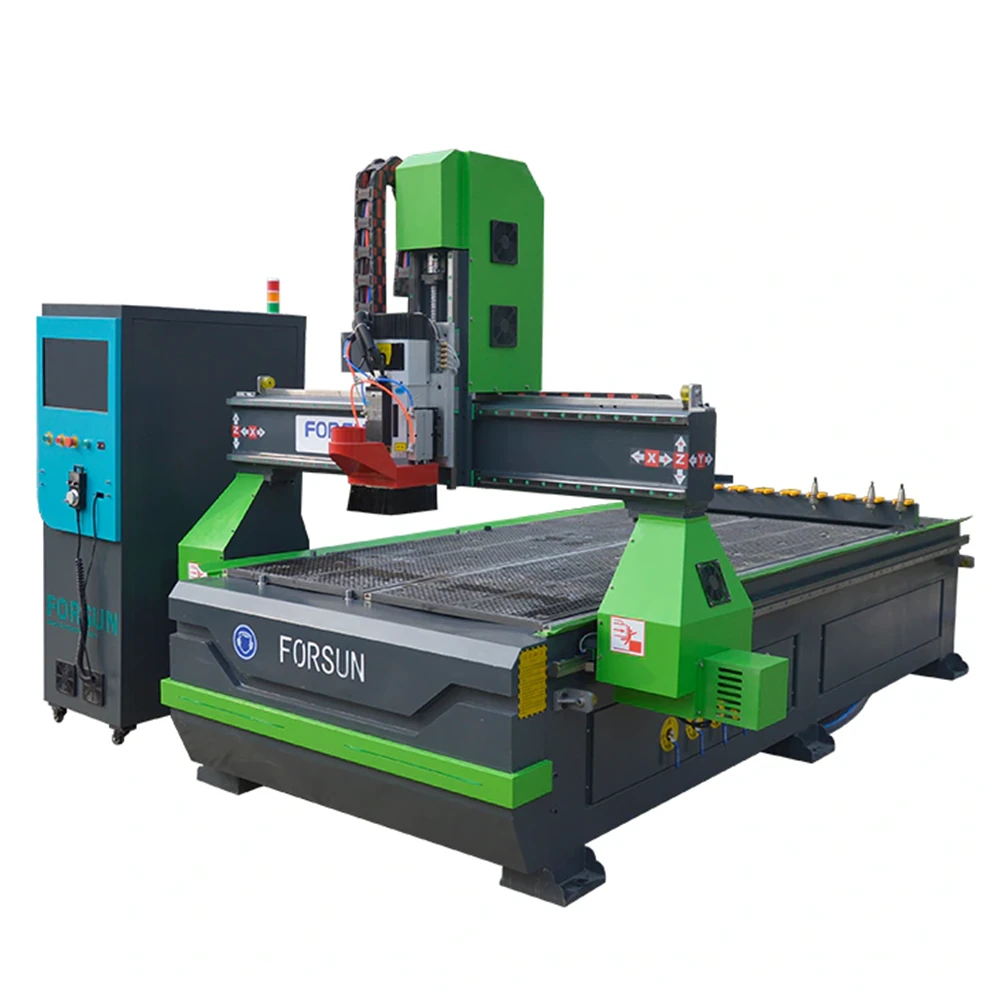
Value-focused 4×8 ft ATC router with a 10-station linear magazine, 9 kW spindle and a dual vacuum plus T-slot table for batch panel work.
View details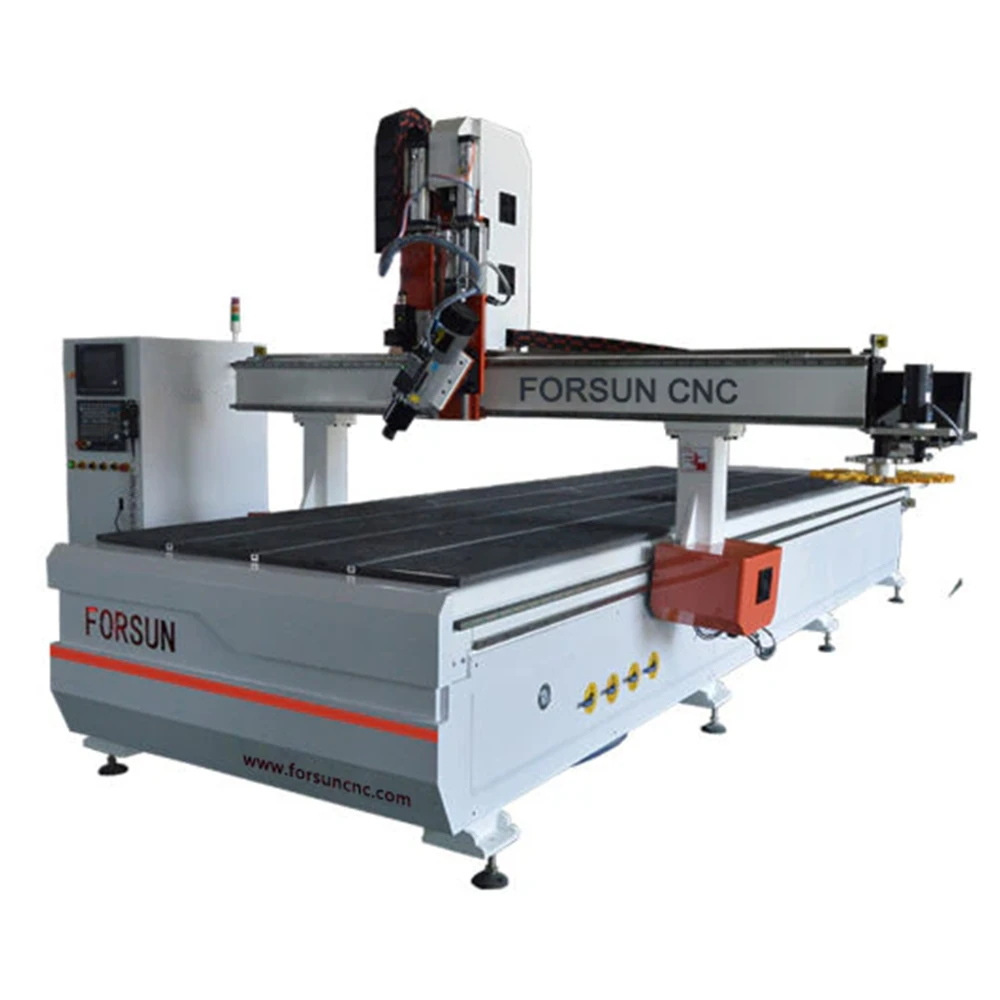
1500×3000 mm machine with a rotary head to ±90° for cylindrical and 3D carving, driven by Yaskawa servos and an Italian HSD 9 kW ATC spindle.
View details
2000×4000 mm furniture router with a 9 kW 24,000 rpm spindle, 10-station linear magazine, 80,000 mm/min rapid and vacuum workholding.
View detailsSeven machines that all remove metal, scaled from a 20,000 rpm drilling and tapping centre for small aluminium parts up to a 22 kW moving-column gantry mill that machines a 5 t casting. Choose by the largest part envelope first, then by spindle taper and tool magazine.
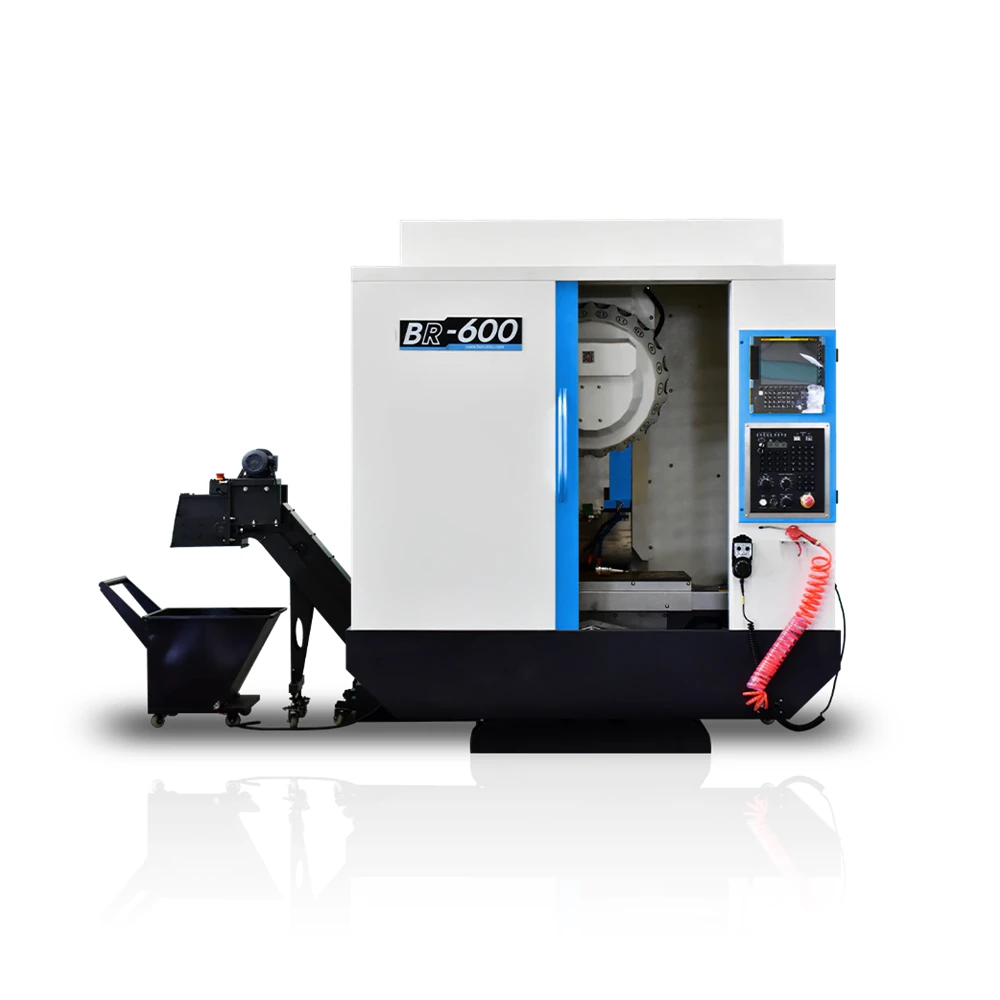
High-speed 20,000 rpm spindle and a 1.6 s tool change for drilling, tapping and light milling of aluminium, electrodes and small steel parts.
View details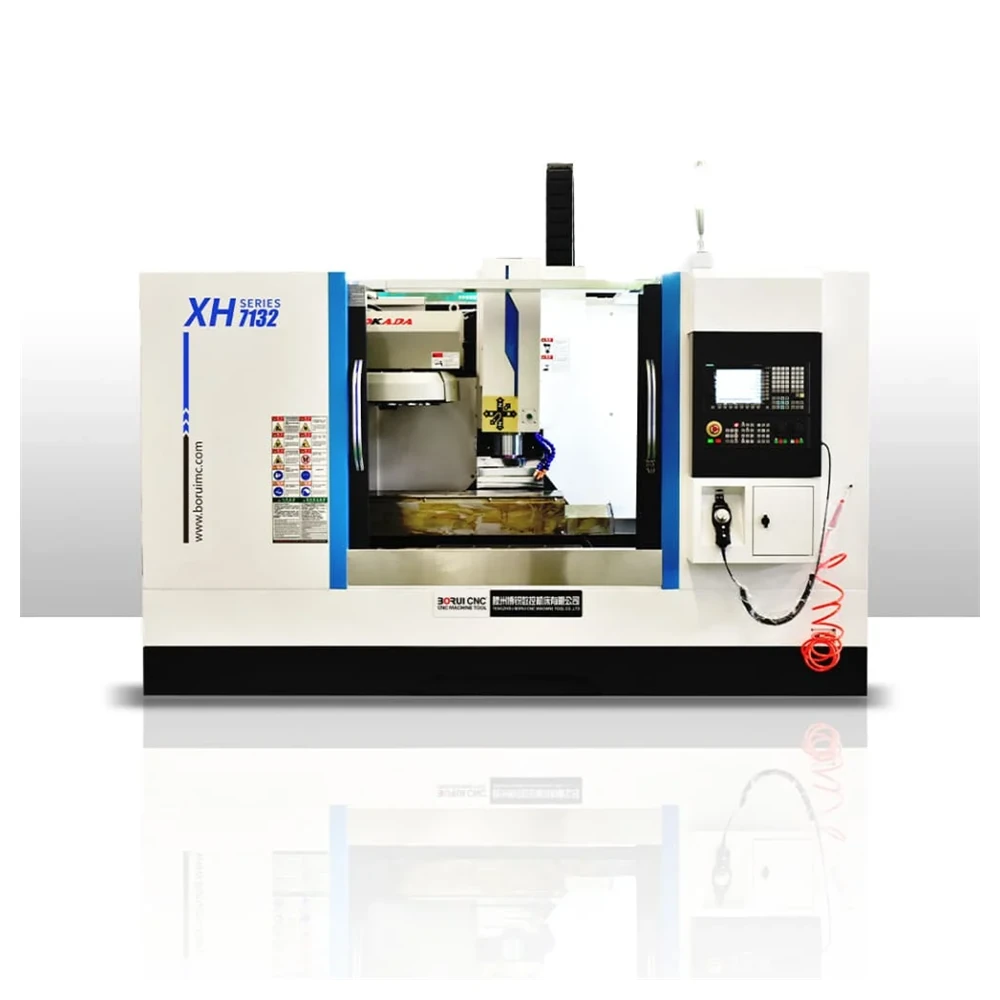
Bridge-column vertical mill with hardened box ways and pre-tensioned ball screws, offered with an optional 10/12-tool umbrella ATC.
View details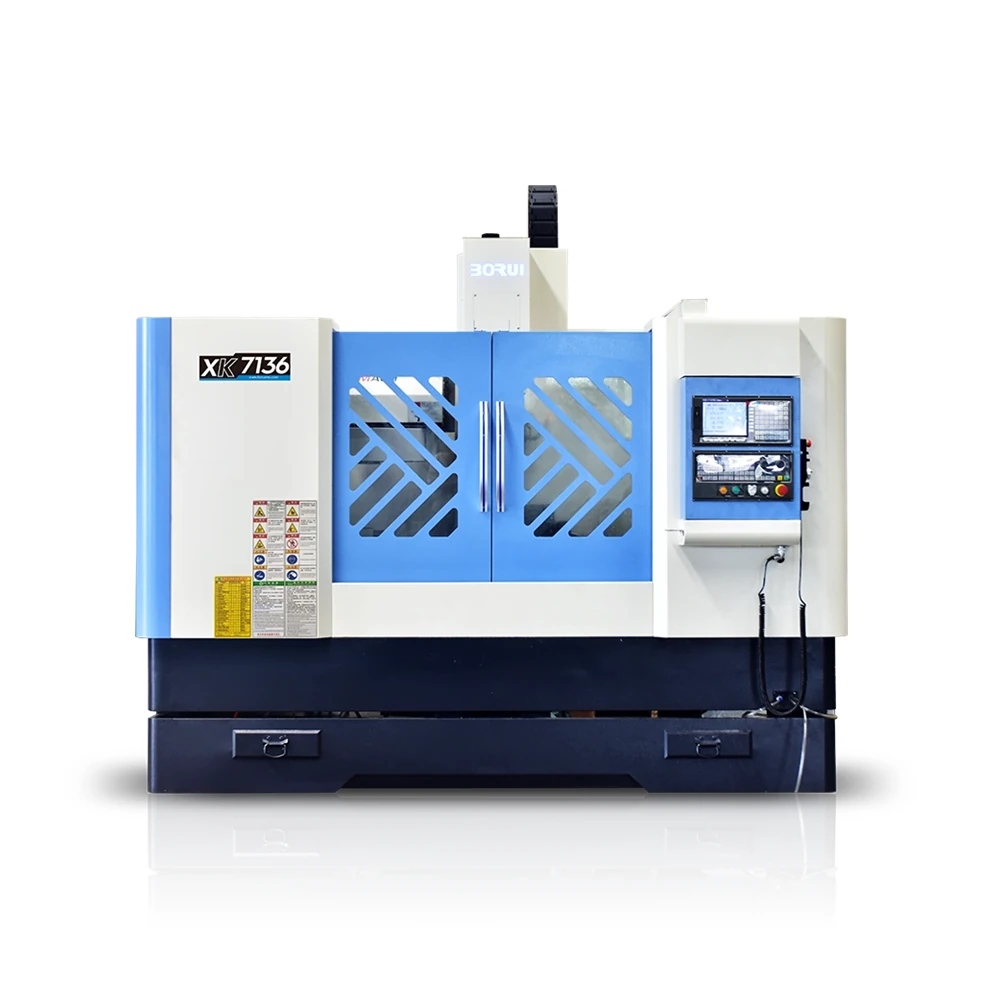
Longer 1250 mm table and 860 mm X travel for elongated parts, with a servo spindle, 10,000 rpm top speed and 16-station umbrella ATC option.
View details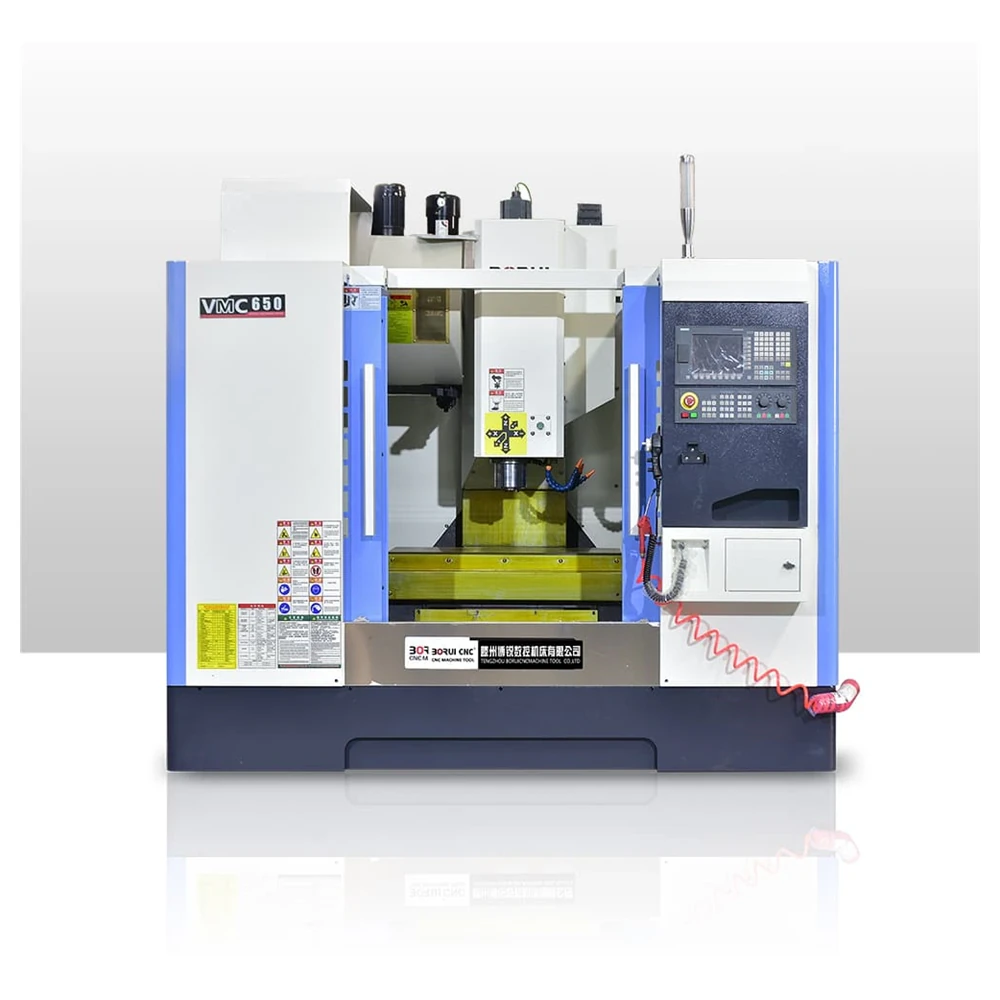
Compact four-axis machining centre for moulds and small steel components, with HIWIN linear guideways and a 16-station disc magazine.
View details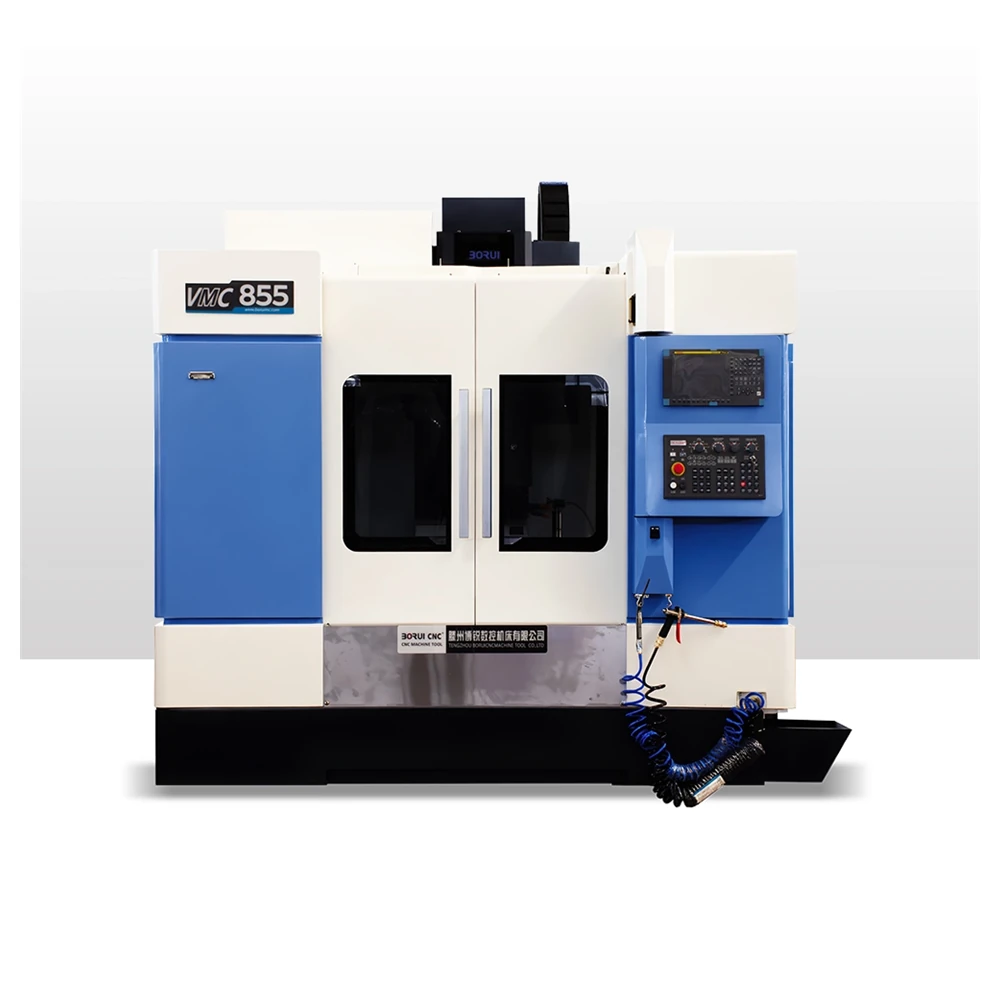
Wider 1000×500 mm table and a 24-station disc magazine with a 1.9 s change, ready for a fourth or fifth axis for multi-face work.
View details
Double-layer resin-sand casting with a 2500×1300 mm bed carrying 5 t, a 24-station disc ATC and 15/18.5 kW of BT50 spindle power.
View details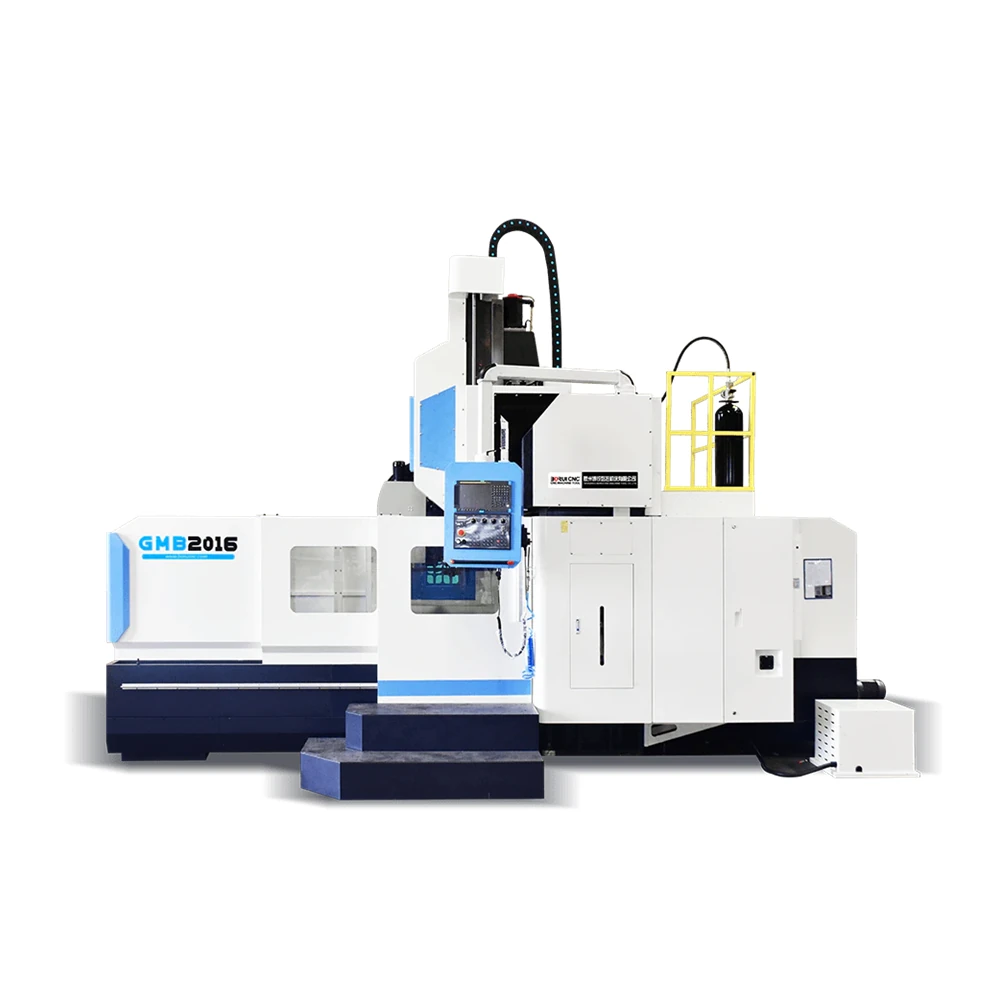
Moving-column gantry with 3000×1800 mm and 4000×2070 mm builds, a 24-arm ATC, gas-balance cylinder and up to 22 kW BT50 spindle.
View detailsLong shafts and heavy disc work want a level bed, a long travel and a tailstock you can trust. High-volume production wants a 45° slant bed that sheds chips, keeps the tool close to the spindle and holds repeatability across a full shift. This range covers both.
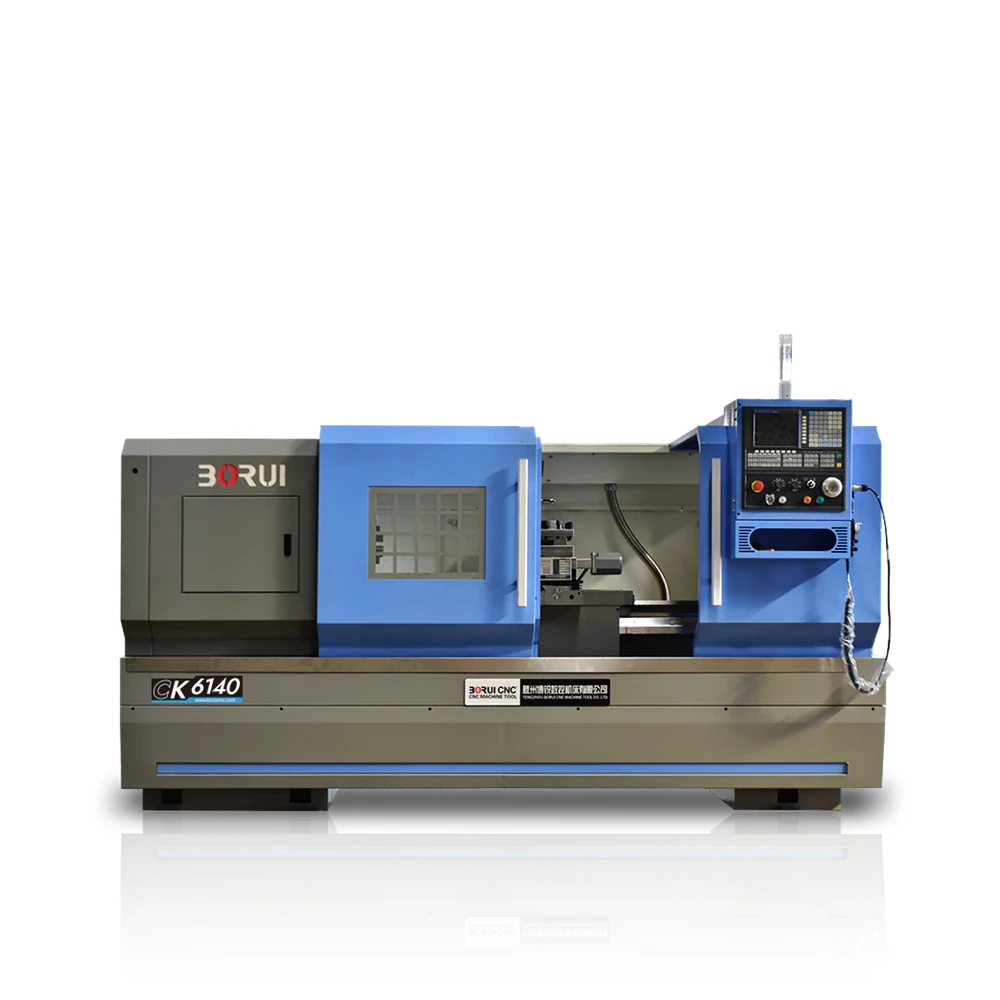
400 mm swing and 750 to 2000 mm between centres. High-rigidity bed and a widened saddle for heavy cutting, with a 52 mm spindle bore as standard.
View details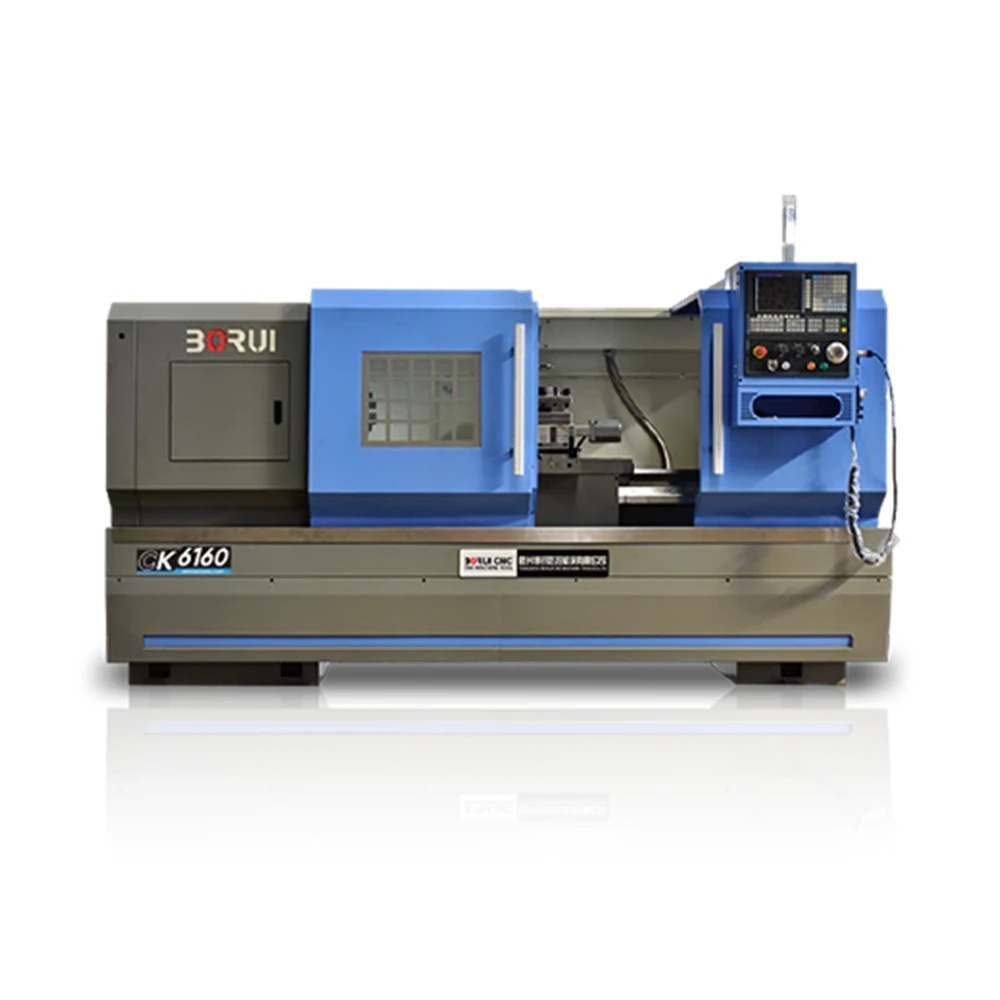
600 mm swing and high spindle torque for disc and shaft parts. GSK control, brand-name ball screws and forced automatic lubrication with low-oil alarm.
View details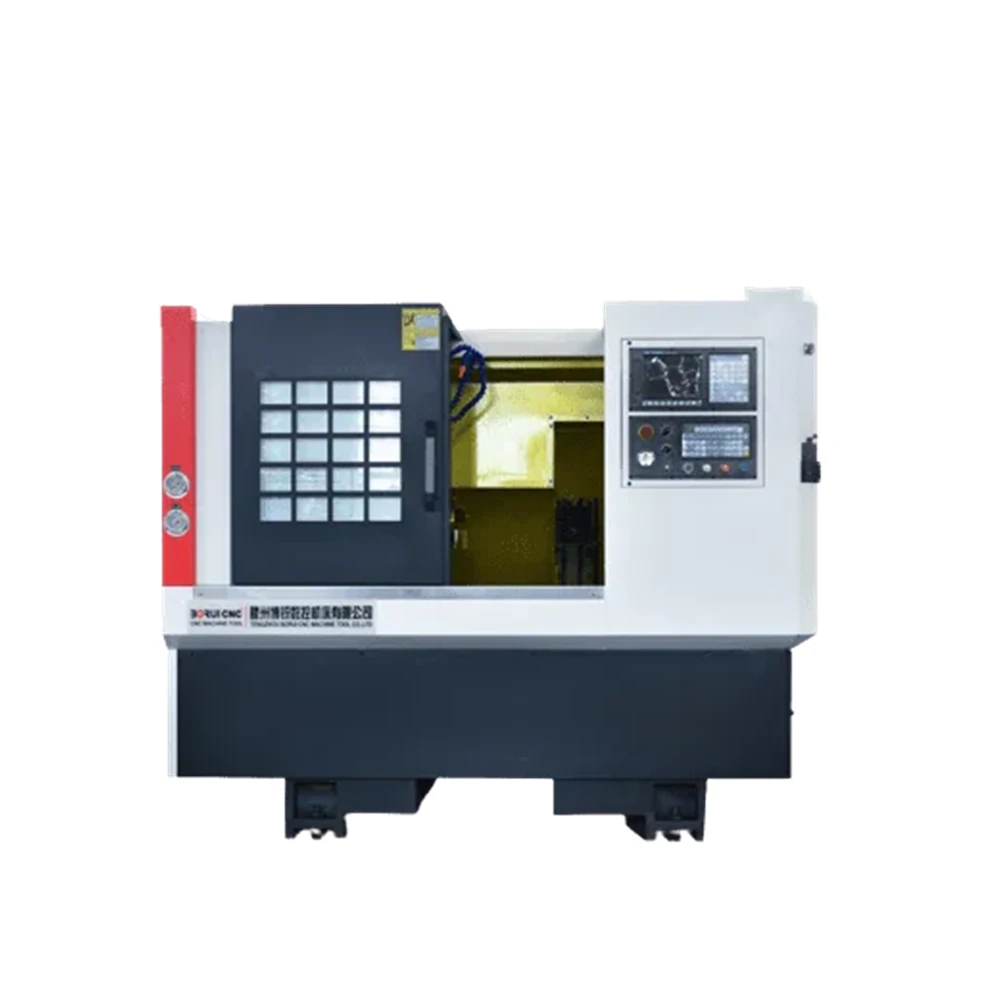
45° integral bed and a high-precision spindle unit in heavy-cutting or high-speed form. Taiwan linear guides and a spindle nose kept close to the operator.
View details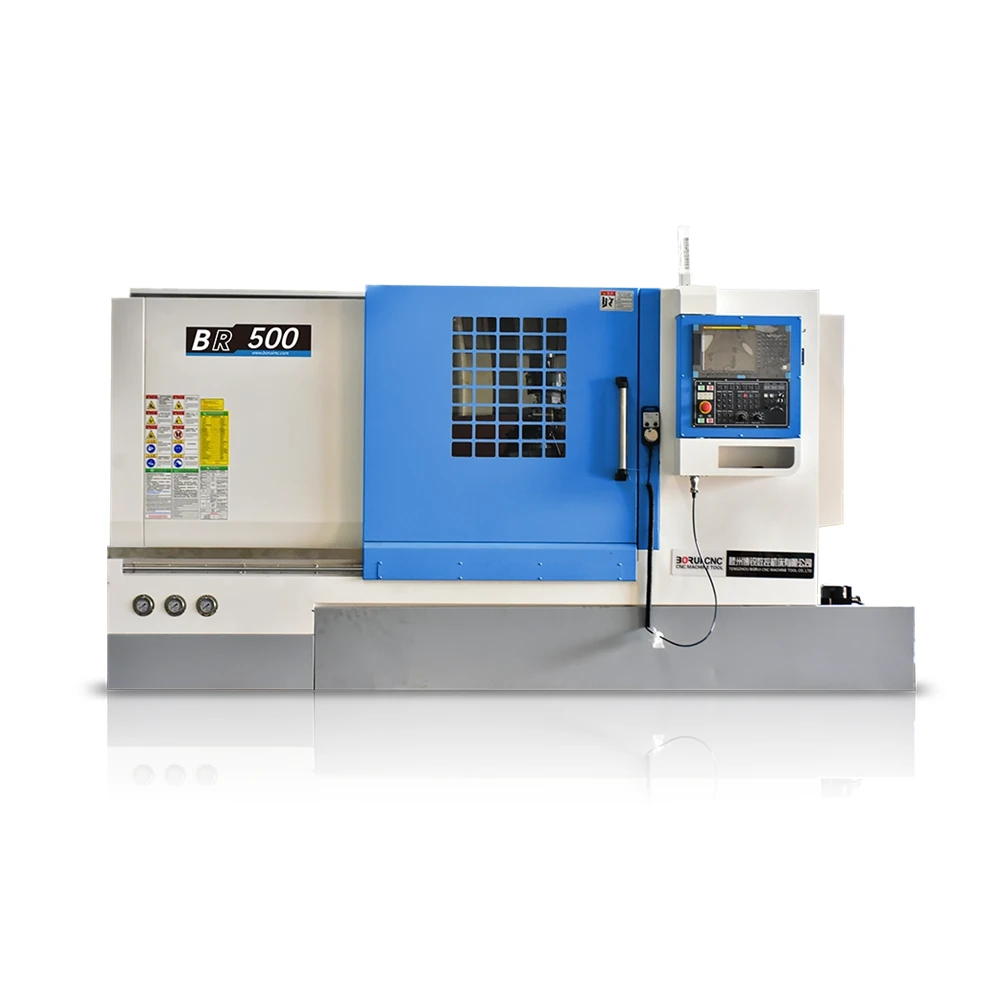
Full-function 45° turning platform with a 7.5 kW servo spindle, 8-inch hydraulic hollow chuck, 8-station servo turret and 20 m/min rapids. Can be built as a turn-mill machine.
View detailsFour thermal cutting platforms for steel plate from 1 to 300 mm. Flame machines handle thick carbon steel economically, plasma machines cut faster on thinner plate, and bevel or rotary multi-torch builds add weld-preparation edges directly at the cut. All are driven by nesting software with automatic gas control.
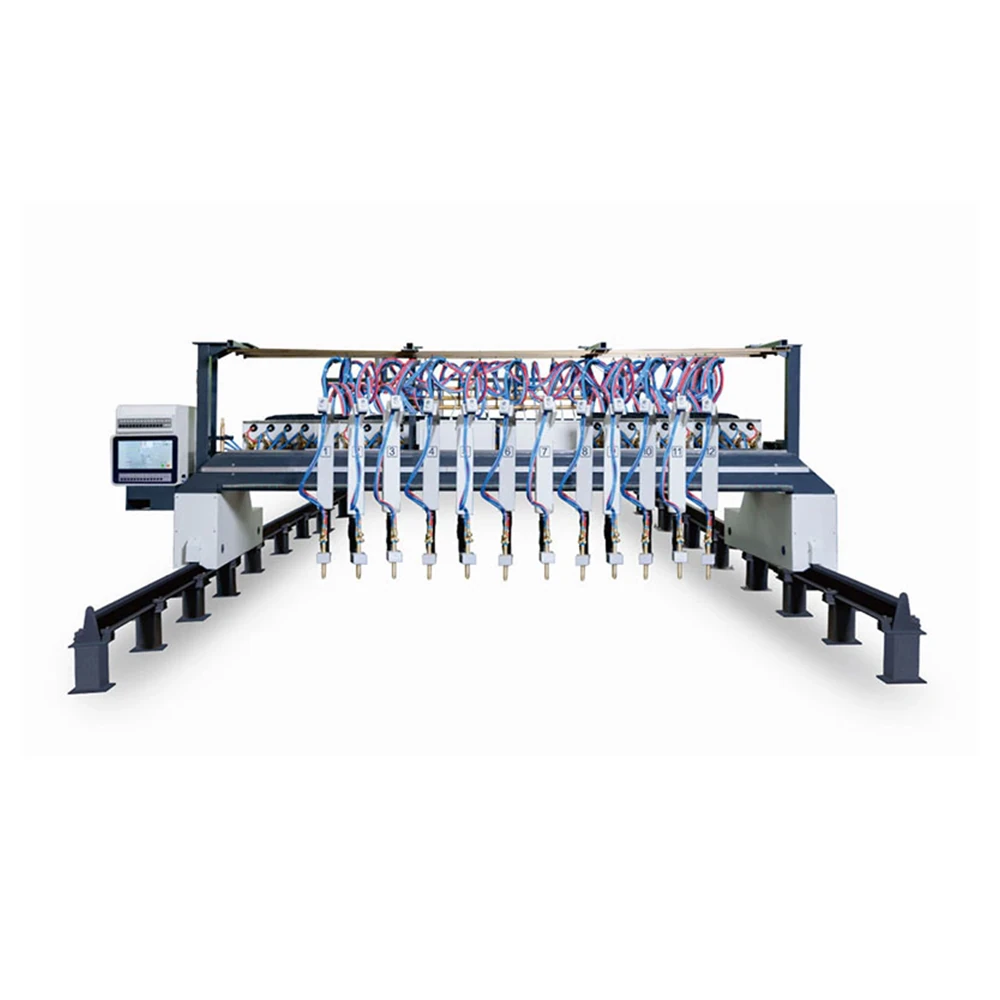
The BDIF intelligent cutting platform: automatic process selection by plate type, thickness and nozzle, with gas control that holds the edge consistent.
View details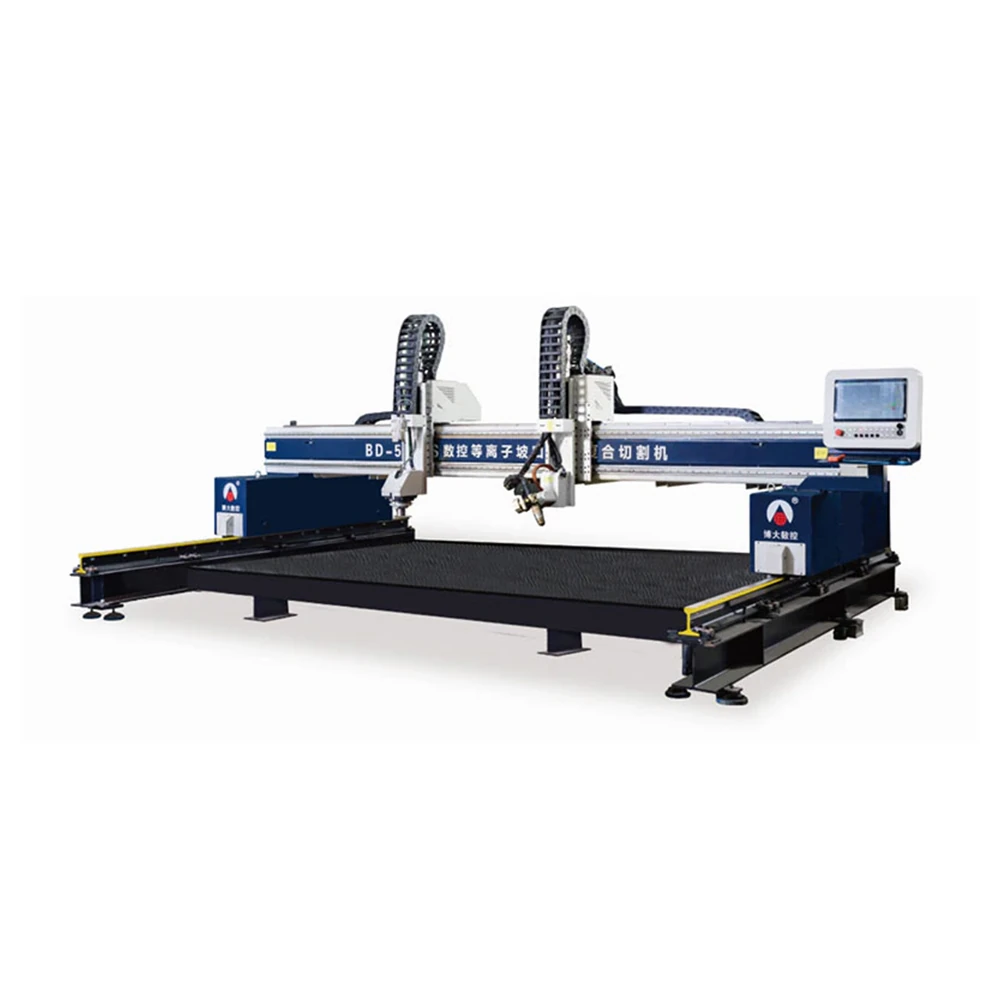
Fifth-generation bevel platform with 15 years of bevel-cutting experience behind it. Straight and bevel cutting on carbon and stainless plate, with an optional marking device.
View details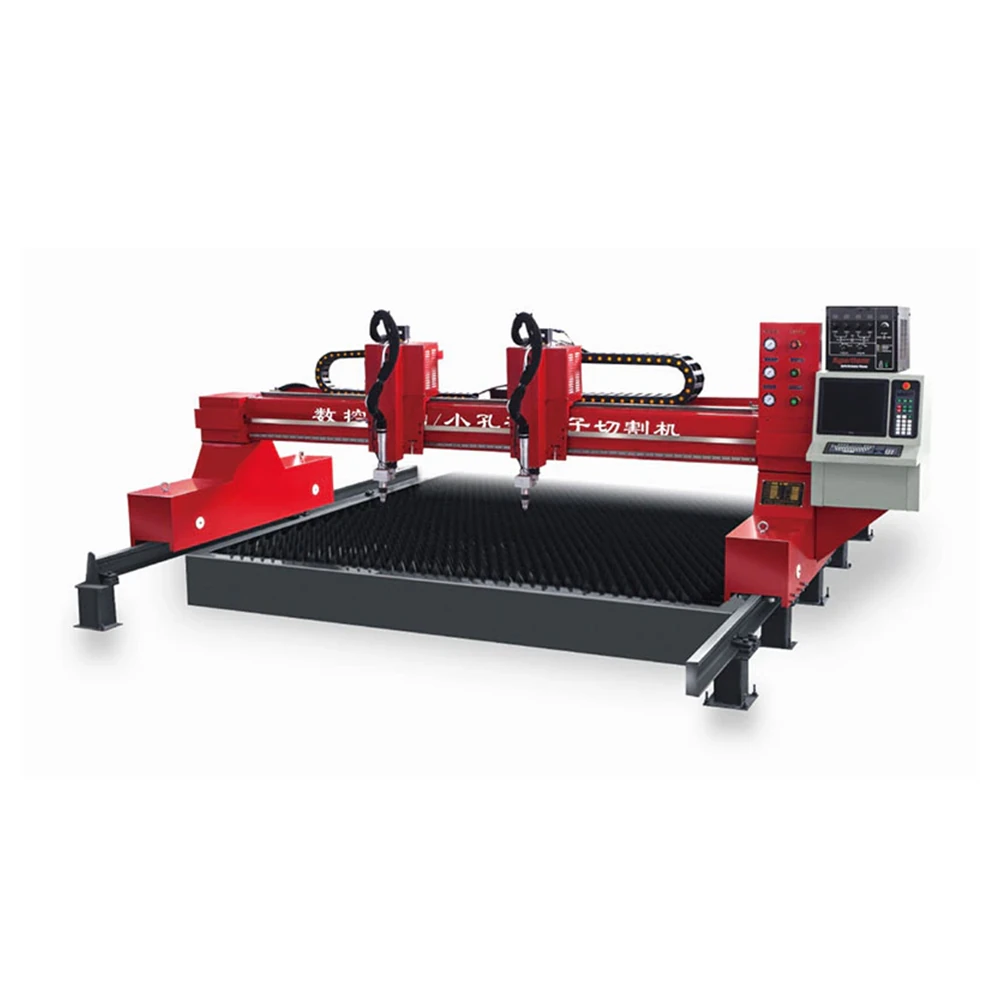
BDPC series high-precision platform that carries two plasma heads for parallel profiling, cutting flat parts such as arcs, slots and irregular outlines at roughly double the output.
View details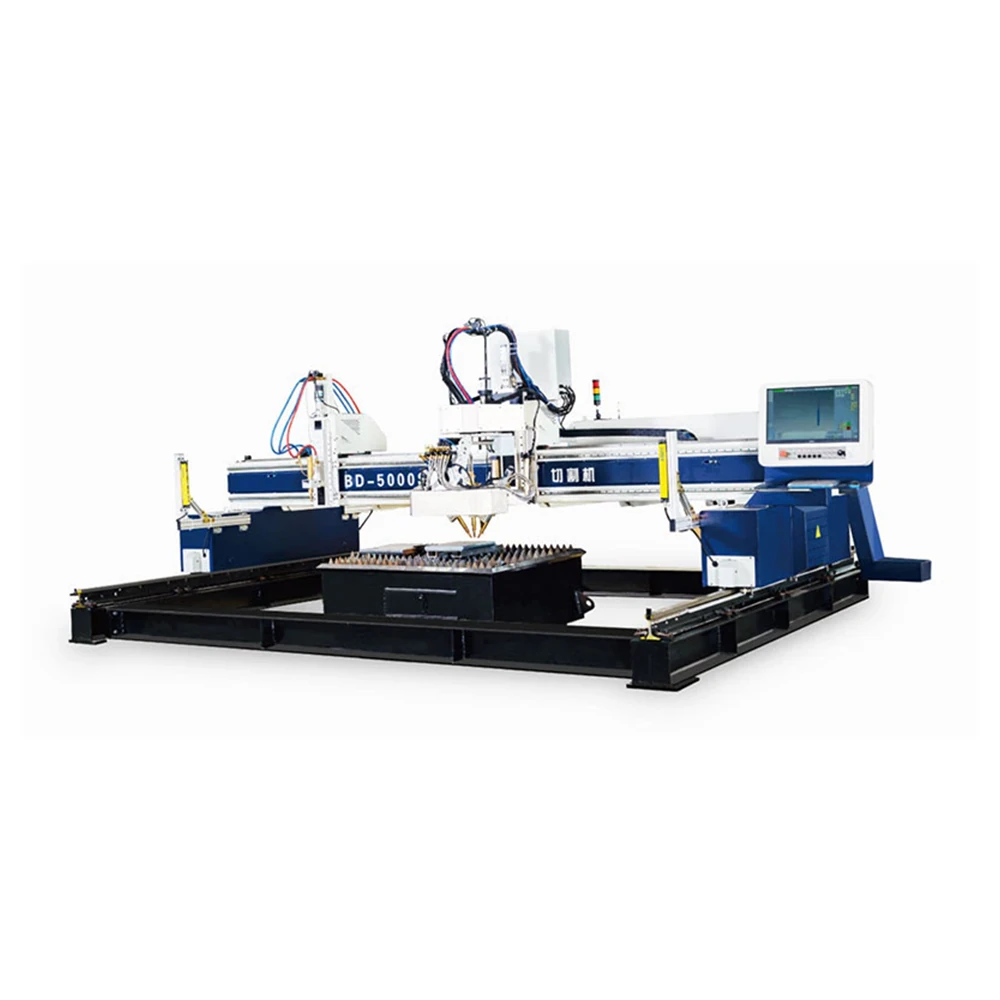
Rotary triple-torch flame platform for thick plate at volume. Three torches cut together and rotate for bevel work, with automatic gas control and optional marking.
View detailsNinety per cent of the decision is made by the largest part envelope, the material and the batch size. Compare the four lines on the parameters that actually drive the choice.
| Parameter | Router & Engraving | Milling | Lathes | Plate Cutting |
|---|---|---|---|---|
| Typical part | Panel, sheet, stone slab, relief, signage | Mould, plate, bracket, casting, electrode | Shaft, bushing, fitting, hydraulic part | Steel plate profile, structural part |
| Materials | Wood, MDF, acrylic, composite, marble, granite | Steel, stainless, aluminium, cast iron, brass | Carbon steel, stainless, alloy, brass, aluminium | Carbon steel, stainless, low-alloy plate |
| Working envelope | 1300×1300 to 2000×4000 mm | 600×400×350 to 3000×2200×1000 mm | 400–600 mm swing, up to 2000 mm centres | Plate 1–300 mm thick, table built to order |
| Spindle or process power | 3–9 kW, up to 24,000 rpm | 7.5–22 kW, BT40 / BT50 | 4–7.5 kW, 4 to 8 tool stations | Plasma, flame or multi-torch; 1–3 heads |
| Clamping | Vacuum table, T-slot, rotary 4th axis | Machine vice, fixture plate, 4th or 5th axis | Hydraulic or manual chuck, tailstock, collet | None needed; plate sits on the cutting bed |
| Best batch profile | One-off carving through to nested batch panels | Single-part job work to full-shift production | Repeat turning of families of round parts | Nested plate runs and structural fabrication |
| Control options | Mach3, DSP, Syntec | Syntec, Fanuc, Siemens, GSK | GSK, Syntec, Fanuc | Dedicated CNC with nesting software |
| Accuracy reference | ±0.05 mm positioning, ±0.01 mm repeat | ±0.005 mm positioning, ±0.003 mm repeat | 0.006 mm repeat positioning | ±0.5 mm bevel, ±1 mm flame edge |
Accuracy figures are factory test references measured on a laser interferometer before shipment. The achievable tolerance on your part also depends on material, clamping and tooling, and is confirmed against a sample test.
The same four lines are specified by furniture factories, signage shops, stone yards, job shops, mould makers and structural steel fabricators.
Nesting, drilling, grooving and edge profiling on 4×8 ft panels, with vacuum workholding and an automatic tool changer to run mixed batches without stopping.
Acrylic, PVC, composite and foam cut and engraved with a polished edge, plus stone lettering on the granite and marble variants of the router line.
High-torque water-cooled spindles with inward and outward tool cooling for gravestones, architectural stone, countertops and carved reliefs.
Vertical machining centres and gantry mills hold tolerance on hardened cavities, inserts and electrodes, with fine-step finishing passes and 24-station tool changers.
Flat-bed and slant-bed lathes turn shafts, bushings, fittings and hydraulic components, with hydraulic chucks and turn-mill configurations for completed parts.
Flame, plasma and rotary multi-torch platforms profile thick plate and cut weld-preparation bevels directly, so parts go from the cutting bed to the welding jig.
Send the drawing, material, tolerance and daily output target. We confirm the machine class, travel, spindle, tool magazine, control and workholding, and put it in writing before production starts.
Where a sample can be sent, we run it on the matched machine and return a measured report with the cut parameters, cycle time and surface result, together with the post-processor for your CAM software.
Stress-relieved structures are machined in one setting, assembled with servo drives and preloaded screws, then checked on a laser interferometer for positioning and repeatability before packing.
Machines ship with English manuals, parameter files and tooling lists. We support commissioning over live video or on site, train your operators, then provide lifetime remote technical support.
Choose by the part: panel and sheet work suits a CNC router; hardened metal parts suit a milling machine or vertical machining center; round parts suit a CNC lathe; plate cutting suits a plasma, flame or laser cutting machine. Travel is set by your largest part plus clamping clearance. Spindle power normally runs from 3 kW on light routers to 24 kW on heavy milling spindles. Send us a drawing and batch size and we will confirm the correct configuration.
Standard positioning accuracy is ±0.005 mm with ±0.003 mm repeatability on servo-driven models, measured on a laser interferometer before shipment. Rigidity comes from the machine structure: our milling and lathe models use stress-relieved cast iron or heavily ribbed steel weldments, hardened and ground linear guideways and preloaded ball screws to hold accuracy under cutting load.
It depends on the machine class. Entry routers and light engraving machines are available with Mach3 or a DSP controller. Production routers, milling machines and lathes are usually specified with Syntec, Fanuc or Siemens CNC systems with servo drives, tool offsets and macro programming. We match the control to your operator skill level and integration requirements, and all systems are delivered with an English interface and parameter set.
Yes. We supply part-specific fixtures and vacuum tables, rotary 4th axes for cylindrical work, and automatic tool changers with 8, 12, 16 or 24 stations depending on the model. Tool holders, collets, clamping kits and vacuum pumps can be included in the same shipment so the machine is production-ready on arrival.
Standard models ship in 15 to 30 working days after deposit; customized travel, spindle or control configurations take 30 to 45 working days. Every machine is geometrically tested and run before packing. We provide English manuals, parameter files, live video commissioning and operator training, plus lifetime remote technical support.
Yes. We customize travel, spindle power and speed, control system, tool changer capacity, table and clamping method, voltage and machine color, and we build OEM/ODM units under your own brand. A customized or OEM machine is confirmed against a signed drawing and build sheet before production starts.