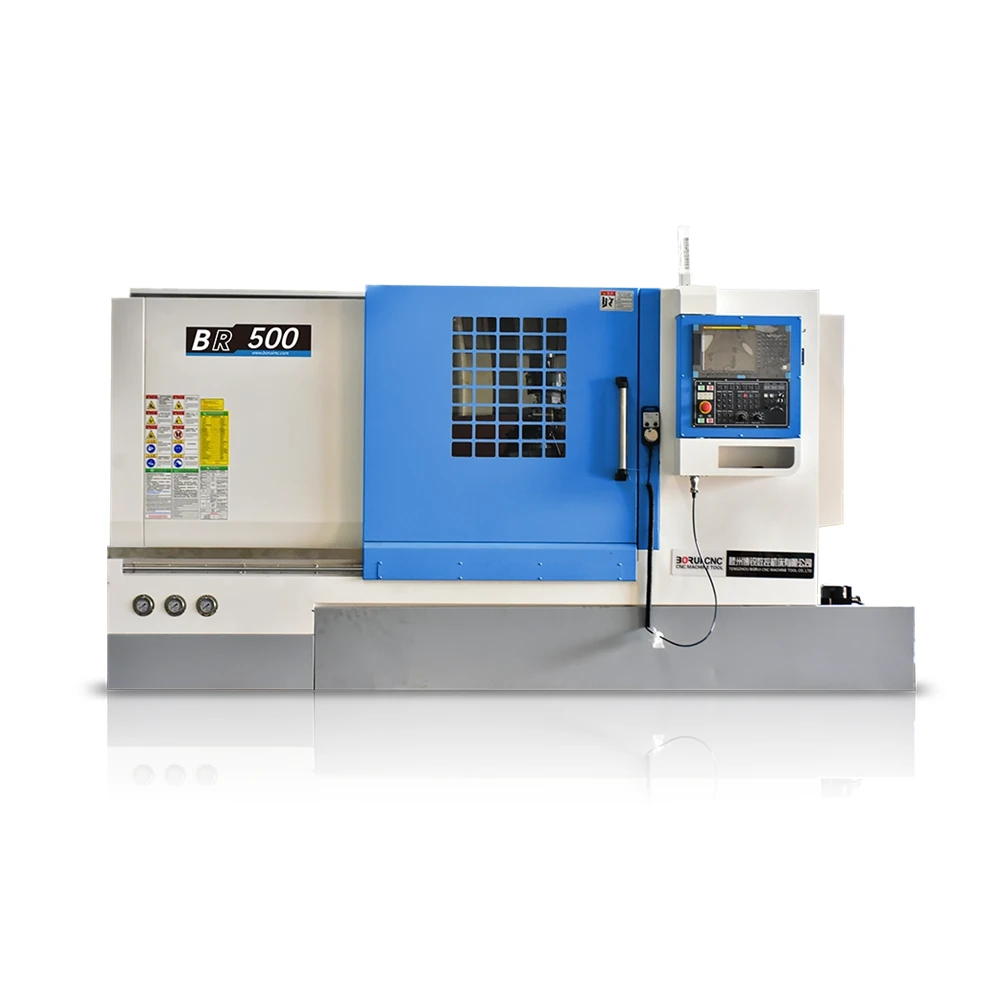
Slant-Bed CNC Lathe BR-500
The larger slant-bed platform with a 7.5 kW spindle, hydraulic hollow chuck and 8-station servo turret.
View modelThe TCK6340 is the small-part specialist of the turning range. A 45° integral bed and Taiwan linear guides give it the rigidity of a bigger machine, the spindle centre sits close to the operator for fast loading, and the spindle unit itself is chosen to suit the work — a heavy-cutting unit for bearing and gear parts, or a high-speed unit for fine finishing.
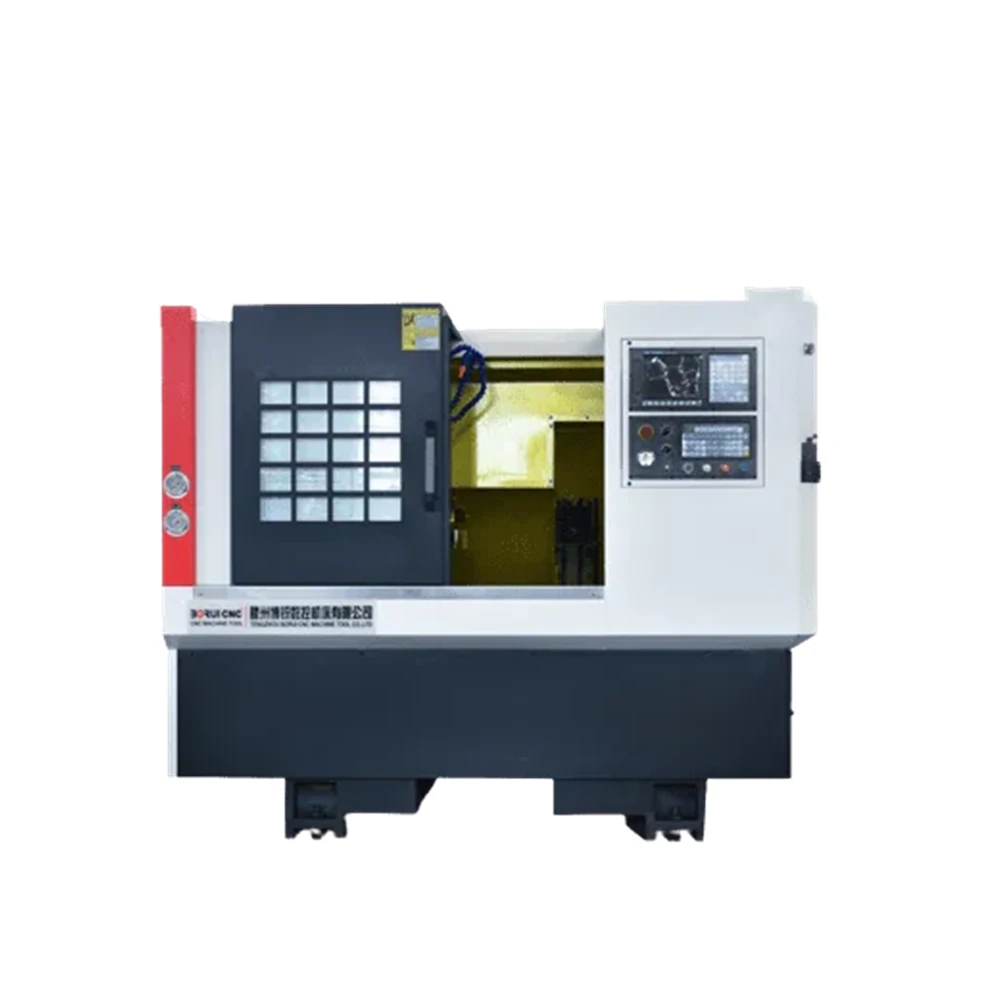
Everything on the TCK6340 serves one goal: turning small and medium parts quickly and accurately, cycle after cycle. The bed angle, the guideway type and the spindle position all point the same way.
A single high-rigidity casting, angled so chips clear the cutting zone and the tool stays close to the work.
High-precision linear guideways under the saddle and turret give the whole machine its stiffness and repeatability.
The spindle centre is placed close to the operator, so loading, unloading and gauging take less reach and less time.
The same machine can be built for stock removal or for finishing. The choice is made at order against the part family you run, not changed on the shop floor.
| Item | Heavy-cutting spindle unit | High-speed spindle unit |
|---|---|---|
| Built for | Bearing and gear type parts | High-speed finishing |
| Priority | Stock removal and rigidity | Surface finish and cycle time |
| Typical part | Rings, blanks and heavier round parts | Small precision shafts and fittings |
| Bed and guides | 45° integral bed with Taiwan linear guides | 45° integral bed with Taiwan linear guides |
| Speed control | Stepless, 50–3500 rpm | Stepless, 50–3500 rpm |
| Spindle motor | 5.5 kW | 5.5 kW |
If the first operation takes a heavy bite from a forging or blank, specify the heavy-cutting unit.
If the part is near net shape and the priority is finish and speed, specify the high-speed unit.
The bed, guides, chuck and tooling envelope are unchanged, so the choice does not disturb the machine layout.
Every figure below comes from the TCK6340 column of the machine datasheet. Options are confirmed on the build sheet.
| Parameter | Specification |
|---|---|
| Max swing over bed | 400 mm |
| Max swing over cross slide | 140 mm |
| Max machining length | 200 mm |
| Max bar through diameter | 45 mm |
| Max disc turning diameter | 400 mm |
| Spindle nose | A2-5 |
| Spindle bore | 56 mm |
| Spindle speed range | 50–3500 rpm, stepless |
| Spindle motor power | 5.5 kW |
| Chuck | 8-inch hydraulic or manual chuck |
| Rapid traverse | 24 m/min |
| Servo motor torque per axis | 6 N·m |
| X-axis travel | 400 mm |
| Second-axis travel | 300 mm |
| Guideway type | Linear guides |
| Tool post | Gang tool post, optional turret |
| Tool shank size | 20 × 20 mm / Φ25 mm |
| Tailstock | Hydraulic tailstock, standard |
| Total rated power | 10 kW |
| Total rated current | 21 A |
| Net weight | 2300 kg |
| Overall dimensions | 2200 × 1530 × 1780 mm |
The datasheet publishes the second linear axis as Y rather than the Z used on most lathes; the axis convention is confirmed with the drawing at order. The same table also lists the wider TCK family, and the figures above are taken from the TCK6340 column only. Positioning and repeat positioning accuracy are verified by a geometric test on each machine before shipment rather than quoted as a single figure. GSK control is standard with Siemens, Fanuc and Mitsubishi options. A chip conveyor is optional.
Four figures that decide whether this machine fits the part.
A compact working length matched to the small and medium parts the machine is designed to run.
Shaft parts can be supported without manual quill adjustment, which keeps the cycle consistent.
Reaching 45 mm means fewer parts have to be fed as blanks rather than bar, which simplifies the process.
Four design points that keep the TCK6340 accurate on short cycles and thin tolerances.
A single 45° casting rather than a bolted assembly, so vibration is damped and finish stays stable.
The bed material and wall sections are chosen for damping, which shows up in surface finish on small diameters.
Lubrication is delivered centrally, so the screws and guides stay protected without a manual routine.
High-precision linear ways give the machine the stiffness to hold tolerance across a fast cycle.
A gang tool post keeps tool-to-tool moves short on small parts, with an optional turret for more stations.
GSK standard with Siemens, Fanuc and Mitsubishi options, so the machine fits the programming habits on site.
Short travels and hydraulic workholding keep the cycle tight on small parts.
Bar up to 45 mm is fed through the 56 mm bore and held in the hydraulic chuck, or a blank is loaded for disc work.
Load the gang tool post with 20 by 20 mm and 25 mm shank tools and enter the offsets for the program.
The stepless spindle runs the profile with threads, arcs and cones, at up to 24 m per minute between features.
Check the first part, then run the batch; the integral bed holds the setting across the run.
The industries below all turn small and medium round parts in volume, which is exactly the TCK6340 envelope.
Fittings, stems and threaded bodies produced to repeatable threads and radii for assembly without hand fitting.
Small precision parts turned at high spindle speed, where finish and dimensional consistency carry the assembly.
Bushings, pins and small housings turned in volume, with the heavy-cutting spindle unit handling rougher stock.
Rings and blanks turned to tight runout, which is the part family the heavy-cutting spindle unit is matched to.
Small threaded parts run from bar, with the gang tool post keeping tool changes short across the batch.
Small stepped shafts supported on the hydraulic tailstock and finished in a single program.
Configuration is agreed before production and support does not depend on shipping the machine back to us.
The machine ships in a container on a braced skid, with the chuck, tailstock and tool post secured.
Levelling, spindle run-in and trial cut are covered by drawings and remote video commissioning.
Parts covered, with free replacement components and lifetime engineering support for the life of the machine.
The heavy-cutting or high-speed spindle unit is confirmed against your part family before the build starts.
The TCK6340 can be specified with one of two spindle units on the same 45-degree bed. The heavy-cutting unit is configured for bearing and gear type parts, where stock removal and rigidity matter most. The high-speed unit is configured for high-speed finishing, where surface finish and cycle time matter most. Tell us the part family and we match the spindle unit to it.
It suits small and medium shafts and disc parts, turning threads, arcs, cones and internal and external surfaces of rotation. With a 400 mm swing over the bed, a 400 mm disc turning diameter, a 200 mm machining length and 45 mm bar capacity, it covers the parts that fill valves, electrical, instrument, automotive, motorcycle and bearing production.
Moving the spindle centre towards the operator shortens the reach for loading and unloading, which matters on short cycle times where a second saved per part changes daily output. It also keeps the part and the tool in clear view, so gauging and adjustment are quicker.
It is fitted with a gang tool post as standard, taking 20 by 20 mm and 25 mm shank tools, and an electric or hydraulic turret can be specified as an option. A hydraulic tailstock is fitted as standard so shaft parts can be supported without manual quill adjustment.
GSK control is standard, with Siemens, Fanuc and Mitsubishi available as options. Control choice is matched to your operator skill level and the programs you already run, and every machine ships with an English interface and parameter set. Chucks can be domestic or Taiwan hydraulic units, or manual.
Standard builds ship in roughly 30 to 45 working days, with the spindle unit choice, turret option or control adding to that. Every machine is assembled, aligned and trial cut before packing, and we provide English manuals, a parameter file, video commissioning and remote operator training, with lifetime support after delivery.
For larger parts or longer shafts, compare the BR-500 and the flat-bed range. Or see all CNC lathes.
The larger slant-bed platform with a 7.5 kW spindle, hydraulic hollow chuck and 8-station servo turret.
View model
Level-bed turning with a 400 mm swing and up to 2 m between centres, for long shafts and general work.
View model
600 mm swing with high spindle torque, hardened ways and forced automatic lubrication for disc and shaft parts.
View model