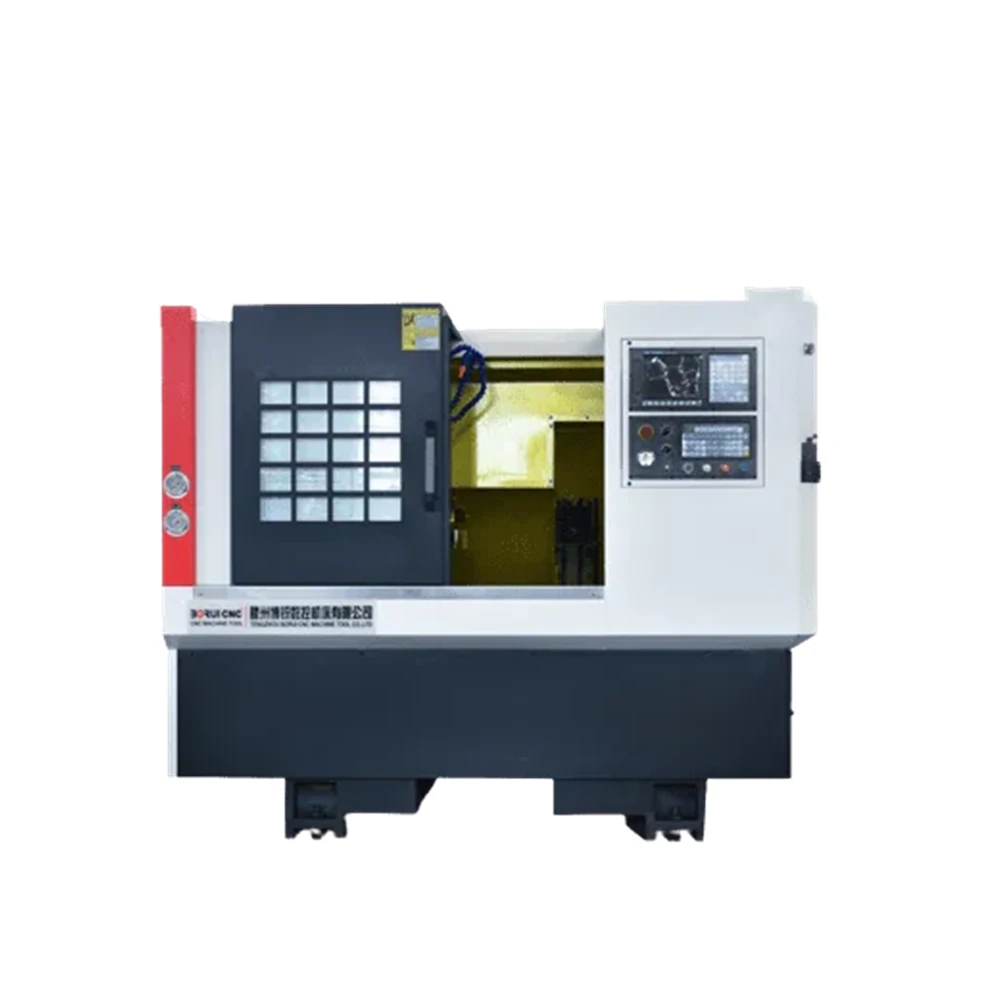
Slant-Bed CNC Lathe TCK6340
45° integral bed with a selectable heavy-cutting or high-speed spindle unit and 24 m/min rapids for small and medium parts.
View modelThe BR-500 is the full-function machine of the turning range. A 45° bed sheds chips and stiffens the load path, a 7.5 kW servo spindle drives an 8-inch hydraulic hollow chuck, and an 8-station servo turret indexes in seconds with 20 m/min rapids. It holds IT6 and Ra 0.8 as a production routine, and with a Y-axis powered turret it becomes a turn-mill machine.
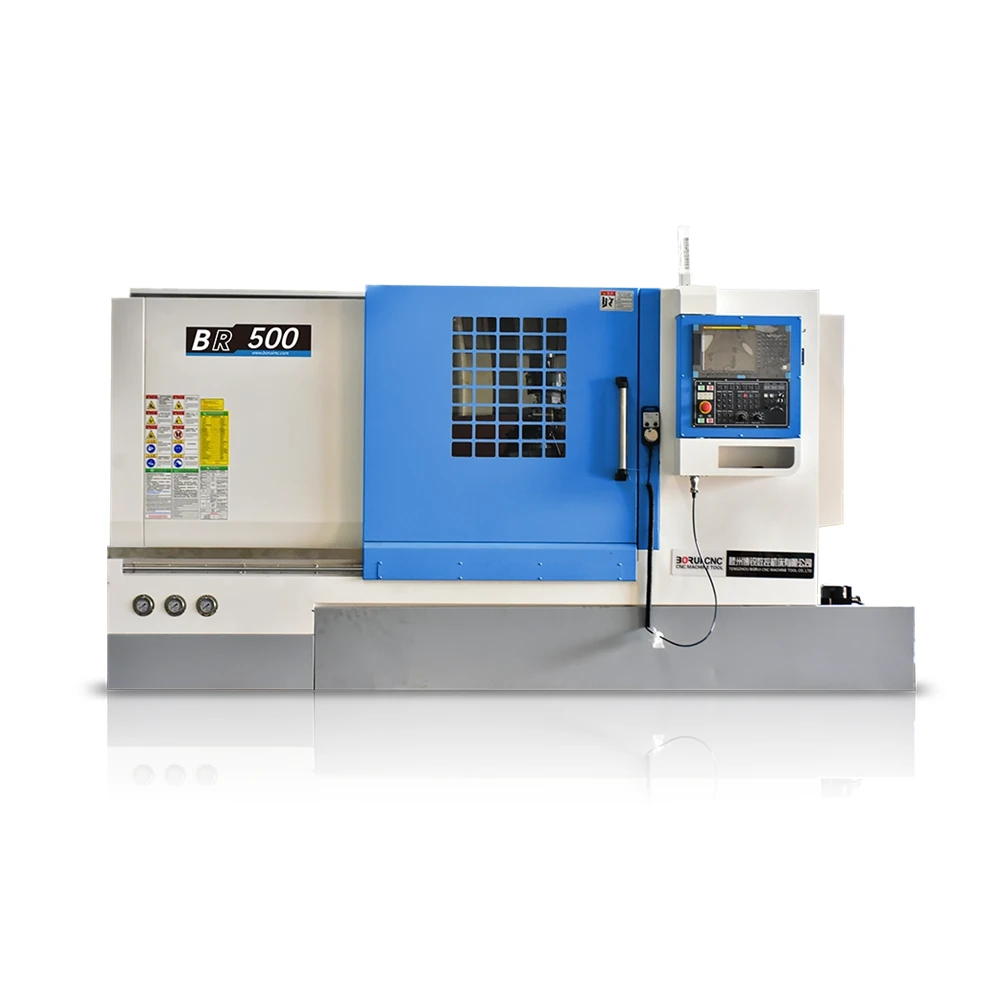
Every part of the BR-500 is specified for repeat production: the servo spindle for stepless speed, the hydraulic chuck and tailstock for fast clamping and support, the servo turret for quick indexing, and enclosed guideway covers and a chip conveyor to keep the cutting zone clear.
Every figure below comes from the machine datasheet. Options are confirmed on the build sheet.
| Parameter | Specification |
|---|---|
| Max turning diameter over bed | Φ500 mm |
| Max turning diameter over slide | 240 mm |
| Cutting length | 450 mm |
| Max disc turning diameter | Φ320 mm |
| Max shaft turning diameter | Φ260 mm |
| Spindle nose | A2-6 |
| Spindle bore | Φ62 mm |
| Chuck | 8-inch hydraulic hollow chuck |
| Spindle speed | Up to 3500 rpm |
| Main motor power | 7.5 kW |
| X-axis rapid traverse | 20 m/min |
| Z-axis rapid traverse | 20 m/min |
| X-axis travel | 210 mm |
| Z-axis travel | 450 mm |
| Guideway type | Taiwan HIWIN / PMI linear guides |
| Turret | 8-station servo turret |
| Tool size | 25 × 25 mm, Φ32 mm |
| Tailstock quill | Φ75 mm, travel L100 mm |
| Tailstock taper | MT4 |
| Positioning accuracy X / Z | 0.01 / 0.01 mm |
| Repeat positioning accuracy X / Z | 0.006 / 0.006 mm |
| Machining accuracy | IT6 |
| Surface roughness | Ra 0.8 µm or better |
| Overall dimensions | 2800 × 1800 × 1600 mm |
| Net weight | 3000 kg |
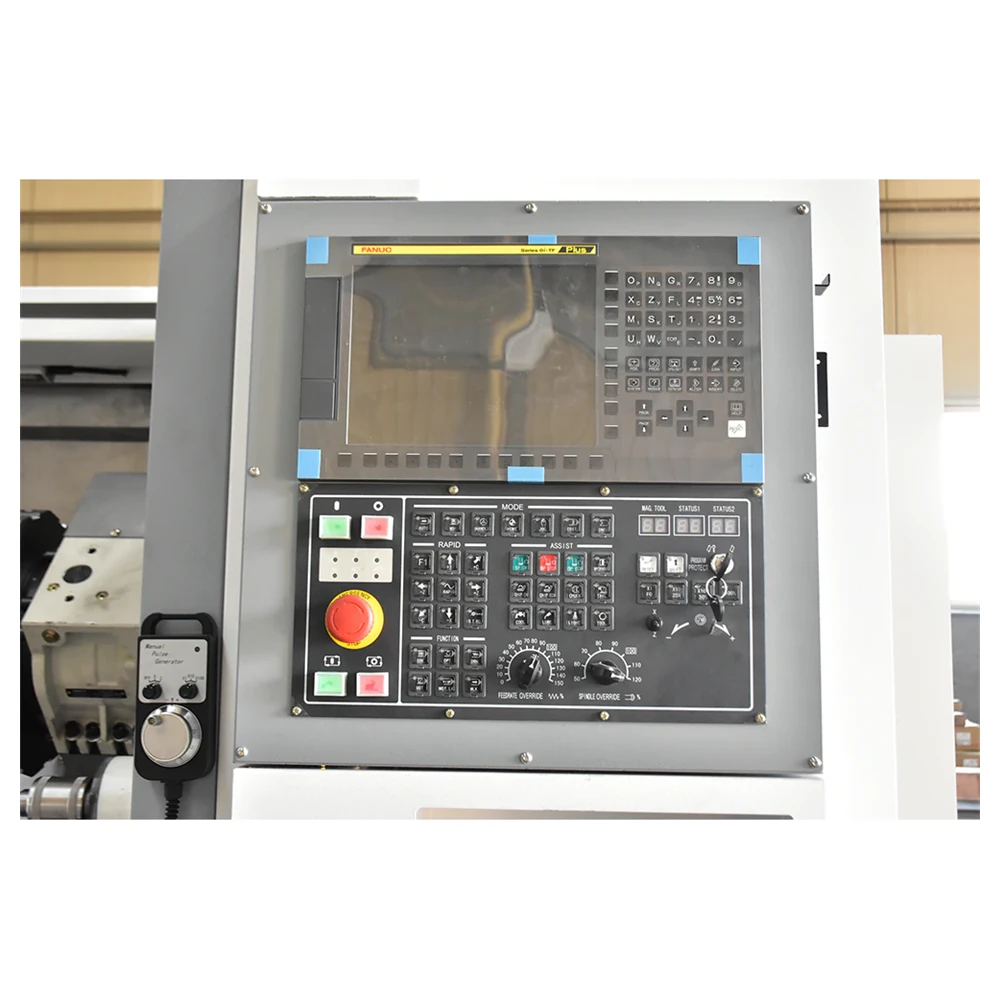
GSK control is standard, with Siemens, Fanuc and Mitsubishi available as options. An optional powered turret with a Y axis converts the machine to a turn-mill platform. Bar feeders, chip conveyors and workholding beyond the standard hydraulic chuck are specified per order.
Four figures that define the platform's production character.
A hydraulic hollow chuck and hydraulic tailstock shorten loading and supporting time on repeat batches.
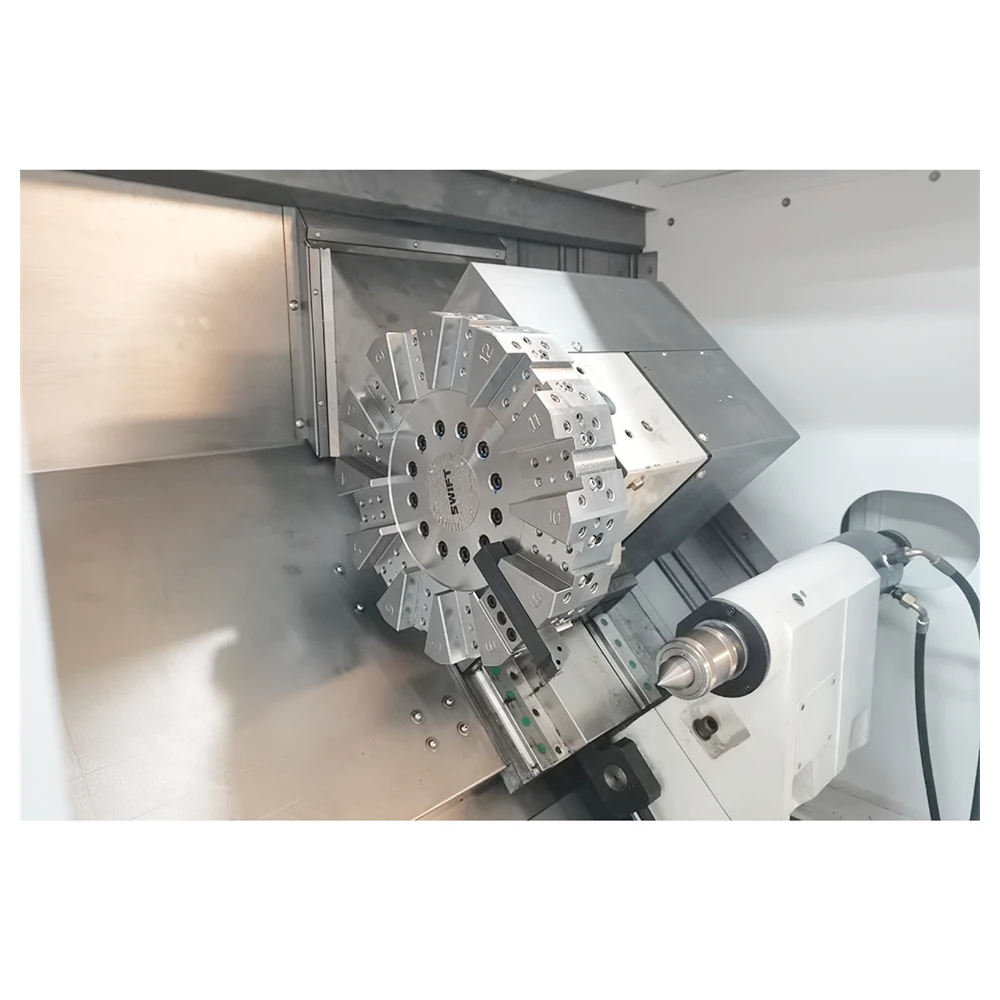
An 8-station servo turret changes tools quickly, which is where a large share of cycle time is won or lost.
The 45° bed and chain-type chip conveyor keep swarf out of the cutting zone and out of the operator's way.
The published accuracy figures are the result of four things working together: the guideways, the ball screws, the spindle unit and the bed structure.
| Accuracy item | Published value | What delivers it |
|---|---|---|
| Positioning accuracy X / Z | 0.01 / 0.01 mm | Preloaded ball screws with servo drives on both axes |
| Repeat positioning accuracy X / Z | 0.006 / 0.006 mm | Enlarged Taiwan HIWIN / PMI linear guideways |
| Machining accuracy | IT6 | Rigid 45° bed with a short, stiff load path |
| Surface roughness | Ra 0.8 µm or better | Spindle unit with high rotational accuracy and low vibration |
| Spindle speed control | Servo driven, stepless | Servo motor and drive, no gear steps to shift |
The 45° bed brings the saddle close to the spindle, so cutting force travels a shorter distance into the structure.
A larger guideway cross-section is what holds repeatability when the machine runs at high rapid rates all shift.
Using a spindle unit rather than separate bearings raises rotational accuracy and keeps it stable over time.
Four design decisions that make this machine comfortable in a high-volume plant.
Chips fall away from the cutting zone, the load path is short and the operator reaches the spindle for fast loading.
A spindle unit gives high rotational accuracy, which shows up directly in roundness and surface finish.
Eight servo-indexed stations take 25 by 25 mm and 32 mm tools, keeping non-cutting time low.
A powered turret with a Y axis adds milling and off-centre drilling, so complex parts need one setup.
Hydraulic workholding and a servo turret keep the cycle tight on repeat batches.
Bar is fed through the 62 mm spindle bore into the hydraulic hollow chuck, or a blank is loaded for disc work.
Set the 8-station servo turret and enter the offsets, with the servo spindle set for the material.
The program turns the profile and threads, with 20 m per minute rapids and fast servo indexing between tools.
Chips are carried out by the chain conveyor, the part is released, and the next cycle starts from a known setting.
Any shop turning the same families of parts day after day will recognise the fit.
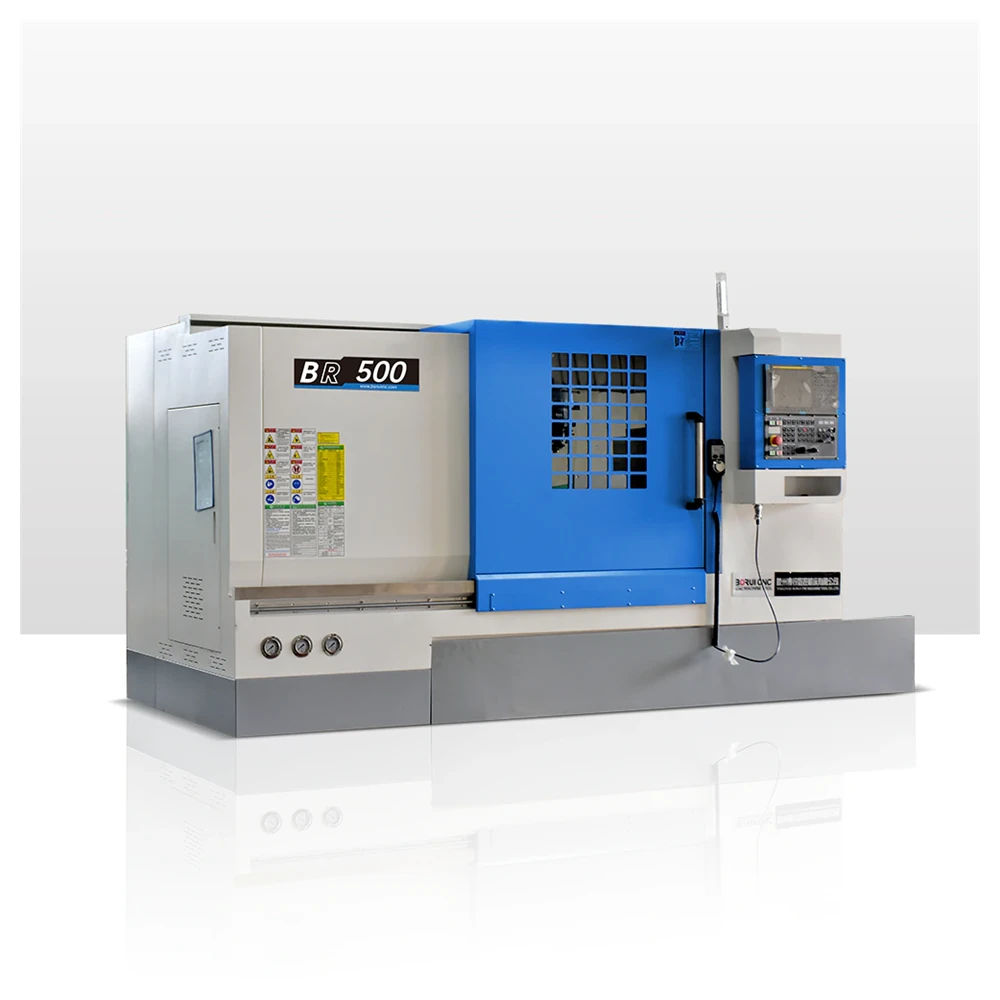
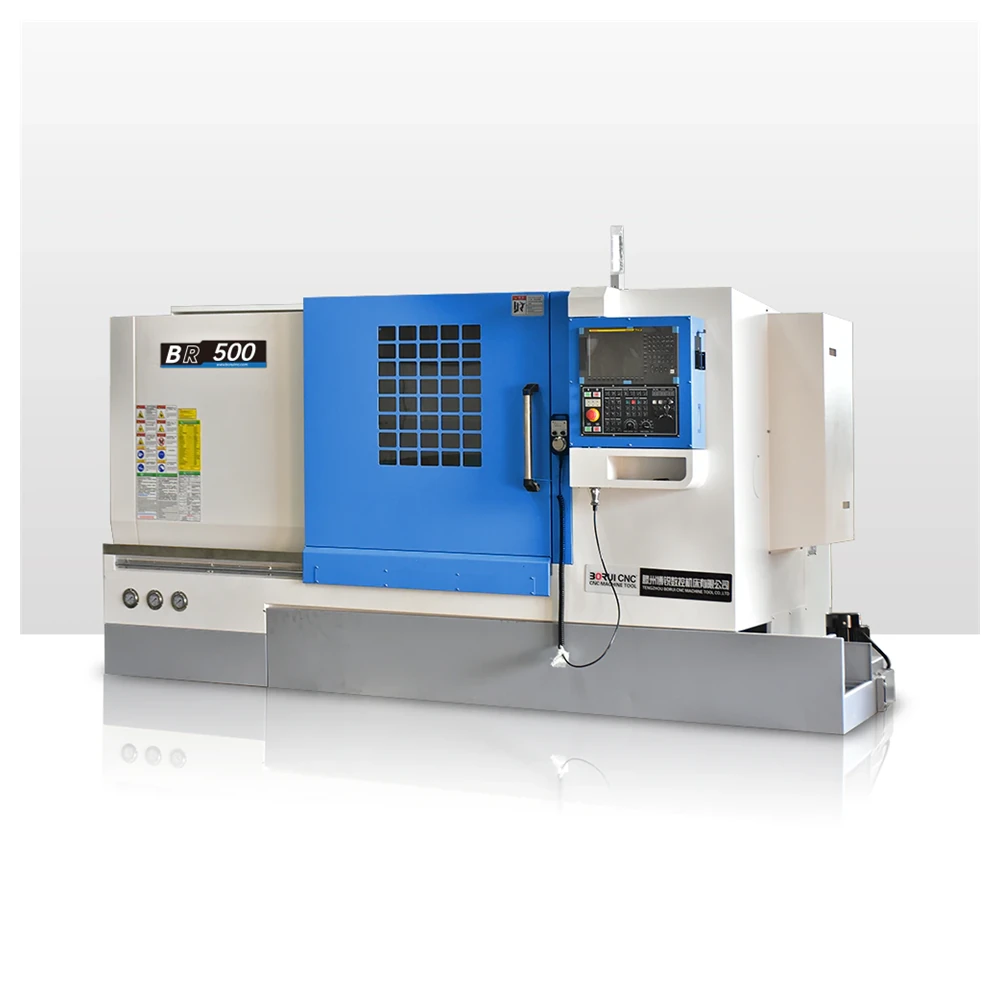
Shafts, bushings and housings turned in volume, where cycle time and consistency across the batch decide the cost.
Bodies, pistons and fittings held to IT6 with a surface finish that seals and bearings can work against.
With the powered turret option, parts with milled flats or off-centre holes are finished without a second machine.
Configuration is agreed before production and support does not depend on shipping the machine back to us.
The machine ships in a container on a braced skid, with the turret, chuck and tailstock secured.
Levelling, turret setting and trial cut are covered by drawings and remote video commissioning.
Parts covered, with free replacement components and lifetime engineering support for the life of the machine.
Bar feeders, part catchers and chip conveyors can be supplied to turn the machine into a lights-out cell.
A 45-degree bed lets chips fall clear of the cutting zone instead of piling up on the ways, and it moves the saddle closer to the spindle so the load path is shorter and stiffer. In practice that means less downtime clearing chips, better rigidity on high-speed turning and easier access for loading parts.
The published figures are 0.01 mm positioning accuracy on both axes and 0.006 mm repeat positioning accuracy, with IT6 machining accuracy and a surface roughness of Ra 0.8 micrometres or better. Those figures come from the combination of enlarged Taiwan HIWIN or PMI linear guideways, preloaded ball screws and a spindle unit built for rotational accuracy.
An 8-inch hydraulic hollow chuck is fitted on an A2-6 spindle nose with a 62 mm bore, so bar can be fed through the spindle and held hydraulically. The turret is an 8-station servo unit taking 25 by 25 mm and 32 mm tools, and a hydraulic tailstock with a 75 mm quill on an MT4 taper is provided for shaft work.
GSK control is standard, with Siemens, Fanuc and Mitsubishi available as options. An optional powered turret with a Y axis turns the machine into a turn-mill platform, adding milling and off-centre drilling to the turning operations without a second setup.
The BR-500 is aimed at high-volume production of disc and shaft parts, with a 500 mm maximum turning diameter over the bed, a 320 mm disc turning diameter, a 260 mm shaft turning diameter and a 450 mm cutting length. The hydraulic chuck, servo turret and fast 20 m per minute rapids keep the cycle short on repeat work.
Standard builds ship in roughly 30 to 45 working days, with control options, the Y-axis powered turret or a bar feeder adding to that. Every machine is assembled, aligned and trial cut before packing, and we provide English manuals, a parameter file, video commissioning and remote operator training, with lifetime support after delivery.
For long shafts a flat bed is the better fit; for smaller high-speed parts compare the TCK6340. Or see all CNC lathes.
45° integral bed with a selectable heavy-cutting or high-speed spindle unit and 24 m/min rapids for small and medium parts.
View model
600 mm swing on a level bed with hardened ways and forced automatic lubrication, for larger discs and long shafts.
View model
The compact flat-bed of the range: 400 mm swing, 52 mm bore and a 4-station tool post for general turning work.
View model