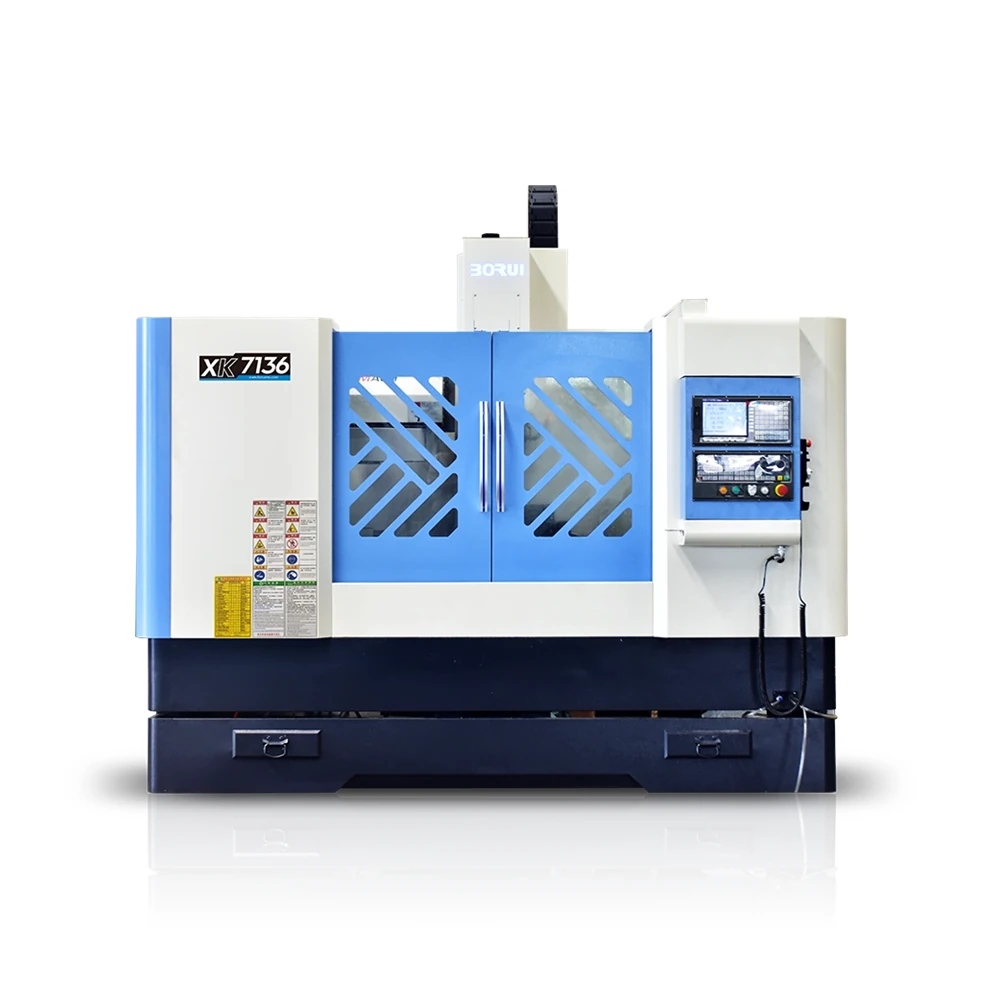
Vertical CNC Milling Machine XK7136
A longer 1250 mm table and 860 mm X travel for elongated parts on the same mill platform.
View modelSome jobs want speed; this one wants stiffness. The XH7132 is built on an A-type bridge column and a large box base, with high-precision hardened box ways and pre-tensioned ball screws, so the machine stays quiet and accurate when the tool is buried in steel or cast iron. A high-strength cast body, a servo spindle rated 5.5 kW and an optional umbrella magazine make it a practical four-axis mill.
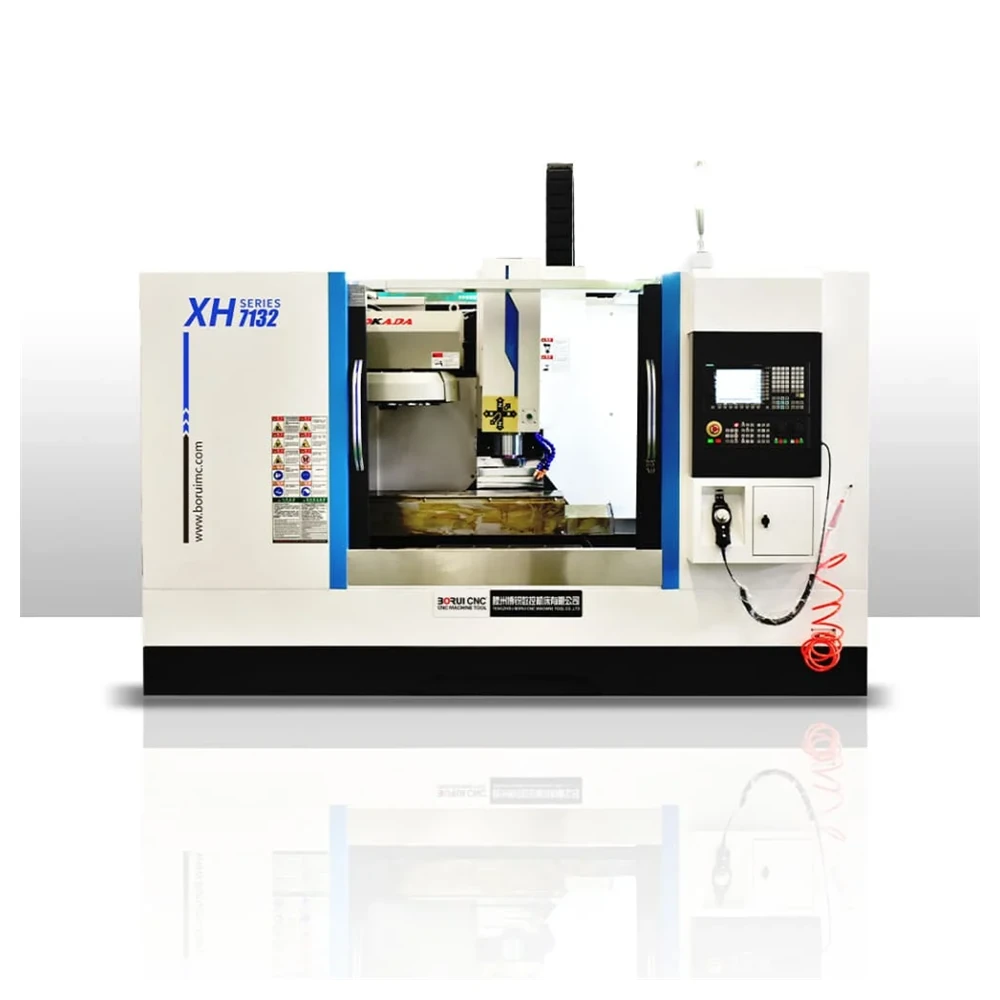
Heavy milling shows up first as vibration. The XH7132 answers it with structure: a stiff column and base, and sliding surfaces that damp the cut rather than transmit it.
Four construction choices decide how this mill behaves when the cutting load is high.
Ground and hardened sliding surfaces give a large load-bearing area and good damping, which is why box ways suit heavy milling.
Precision ball screws are held in pre-tension, so thermal growth does not open up play and the axis stays on position.
Chip guards over the ways and screws keep abrasive swarf out of the sliding surfaces, which protects both accuracy and life.
An intermittent automatic lubrication system prevents the ways from ever running dry, which is the usual cause of premature wear.
Transcribed from the machine parameter table.
| Parameter | Value |
|---|---|
| Table size | 1000 × 320 mm |
| Table load | 300 kg |
| T-slots | 3 − 16 × 75 mm |
| X axis travel | 630 mm |
| Y axis travel | 400 mm |
| Z axis travel | 500 mm |
| Spindle nose to table | 100–620 mm |
| Spindle centre to column | 400 mm |
| Spindle speed | 8000 rpm, 10,000 rpm option |
| Spindle taper | BT40 |
| Main motor power | 5.5 kW servo |
| Rapid traverse X / Y / Z | 20 / 20 / 20 m/min |
| Positioning accuracy | ±0.005 mm |
| Repeatability | ±0.004 mm |
| Tool changer | Optional umbrella 10 / 12 stations |
| Machine dimensions | 2240 × 1840 × 1390 mm |
| Net weight | 2800 kg |
The tool changer is listed in the datasheet as an option, with a VOLIS spindle and 12-station umbrella magazine also available. Control system, spindle speed option and magazine configuration are confirmed before production.
Not every job needs an automatic changer. The XH7132 can be specified to match how many tools your part actually uses.
A 10 or 12-station umbrella magazine from OKADA holds the tool set for a multi-operation part, so drills, taps and end mills follow each other without an operator at the machine. It is compact and sits close to the spindle, keeping change travel short.
For jobs that run one cutter — a face mill, a fly cutter or a single profile tool — the machine can be supplied without a changer, which reduces both the build and the routine maintenance.
The machine earns its keep on work where rigidity in the cut matters more than the fastest possible rapid.
Mould plates and inserts milled to shape, where a stiff column keeps the cavity walls true under load.
Tooling plates and fixture bodies machined four-sided with the rotary axis in a single setup.
Iron and steel castings faced, drilled and bored, where interrupted cuts punish a light machine.
Shafts, plates and brackets for machine builders, run in small batches through the umbrella tool set.
Die plates and forming tools with deep pockets and hardened inserts cut at conservative feeds.
Job-shop milling where the part fits the 1000 mm table and the tolerance fits the machine.
A longer table, a fully enclosed centre, or a machine built for high-speed hole work.
A longer 1250 mm table and 860 mm X travel for elongated parts on the same mill platform.
View model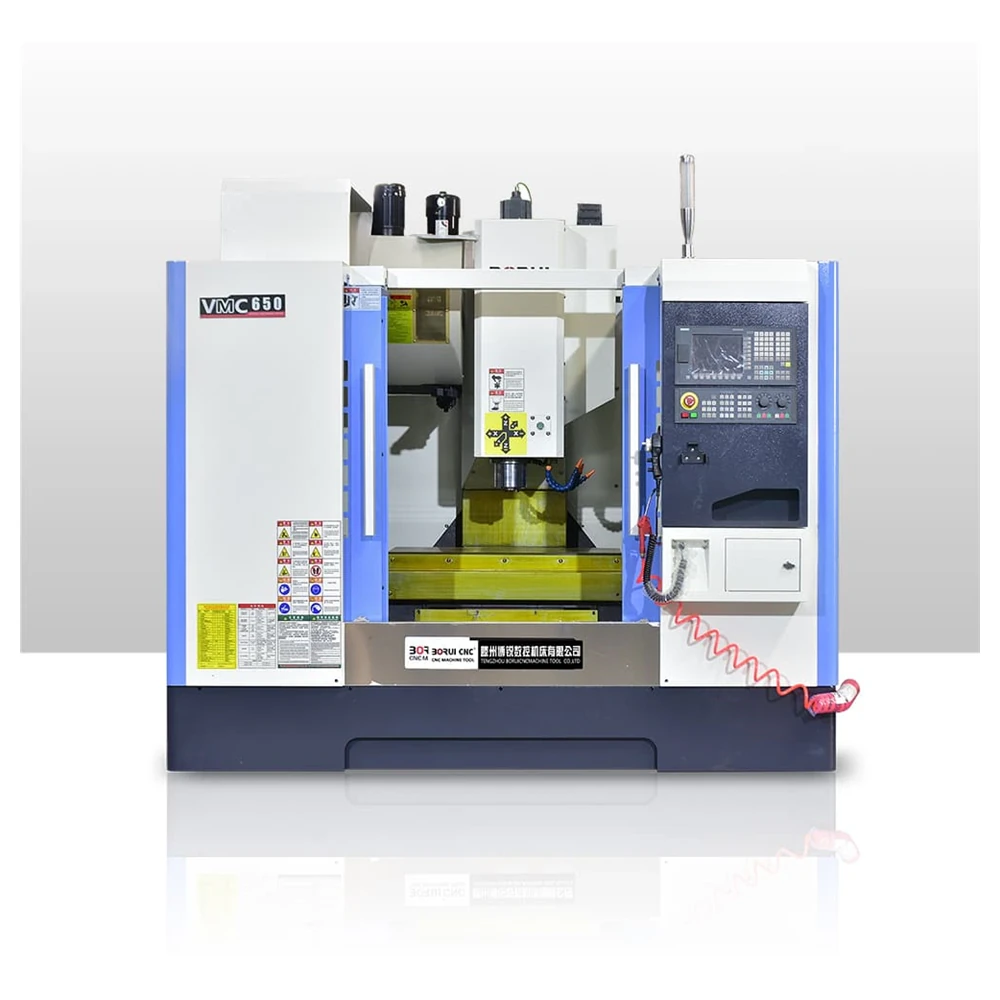
A fully enclosed machining centre with linear guideways and a 16-station disc magazine.
View model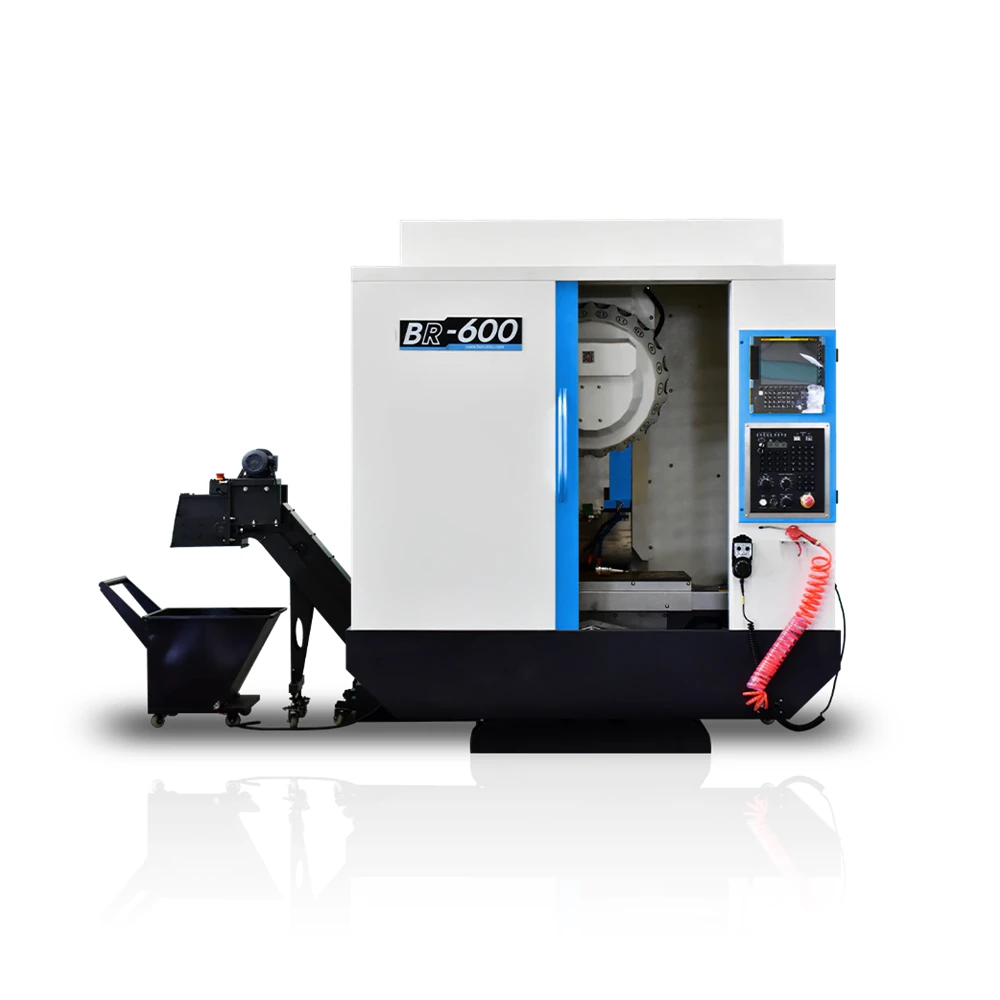
When the job is thousands of holes and threads, high spindle speed beats high structure stiffness.
View modelIt suits parts that reward rigidity over sheer spindle speed: moulds and mould inserts, jigs and fixtures, machined castings and general precision milling. The hardened box ways and A-type bridge column keep the cut stable when the tool is engaged in interrupted or heavy milling, which is exactly where a light linear-guide machine would start to chatter.
Box ways carry the load over a large ground and hardened contact area, so they resist deflection under heavy cutting force and absorb vibration well. They are slower than roller linear guides on rapid moves, but for heavy milling of steel and cast iron the rigidity and damping matter more than the last few metres per minute of traverse speed.
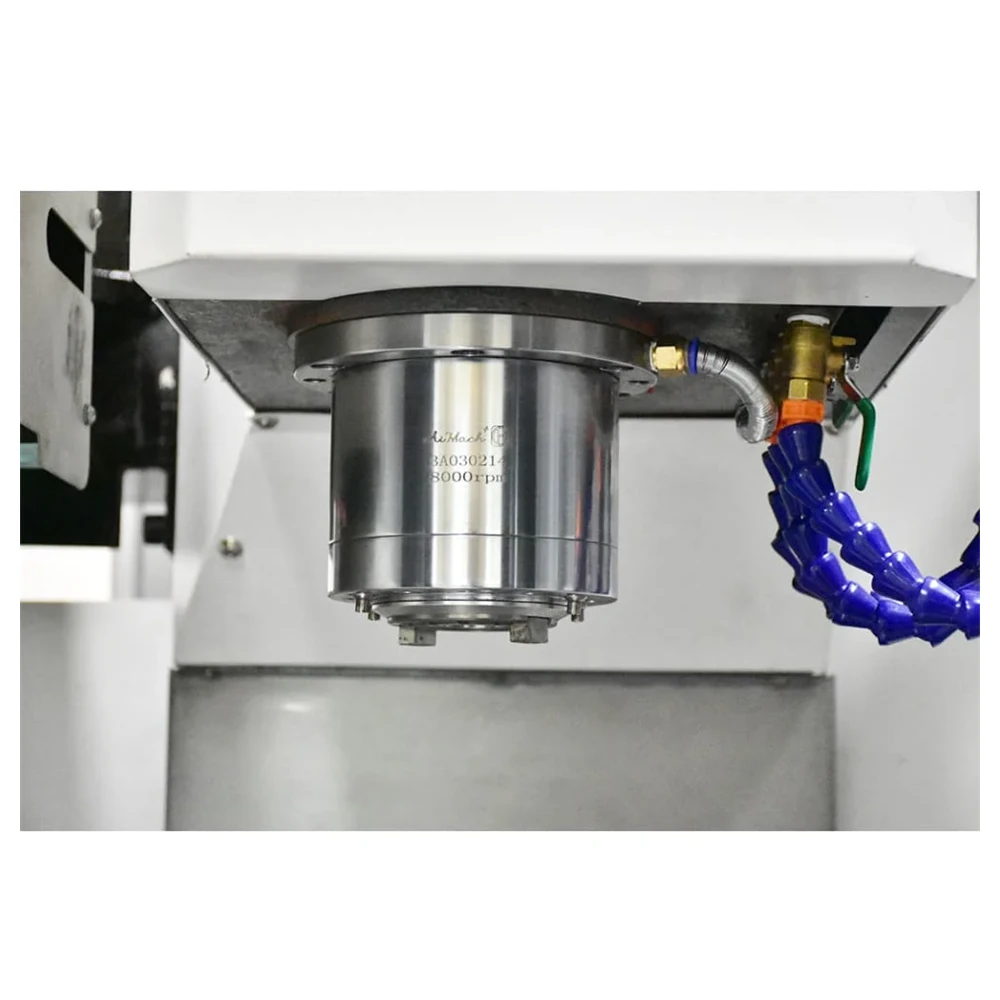
The spindle is a high-speed Taiwan unit with a BT40 taper, running at 8000 rpm as standard with a 10,000 rpm option. An umbrella magazine with 10 or 12 stations from OKADA can be specified, or the machine can be ordered with a VOLIS spindle and a 12-station umbrella magazine. It can also be run without an ATC for single-tool work.
Positioning accuracy is plus or minus 0.005 mm with plus or minus 0.004 mm repeatability. Both figures are supported by the pre-tensioned precision ball screws and by the body casting, which is high-strength iron with a stable microstructure, so the geometry holds over years of service rather than drifting after the first year.
An automatic centralised lubrication system feeds the axes, and the guideways and ball screws are sealed and protected to keep chips and swarf out of the sliding surfaces. An oil-water separation design, a spindle nose cleaning air blast and full enclosure keep the working area clean and the maintenance routine short.
Standard builds ship in 15 to 30 working days after deposit, and customised spindle or control configurations take 30 to 45 working days. Every machine is geometrically checked and run before packing. We provide English manuals, parameter files, video commissioning and operator training, plus lifetime remote support. Volume terms are agreed per order.