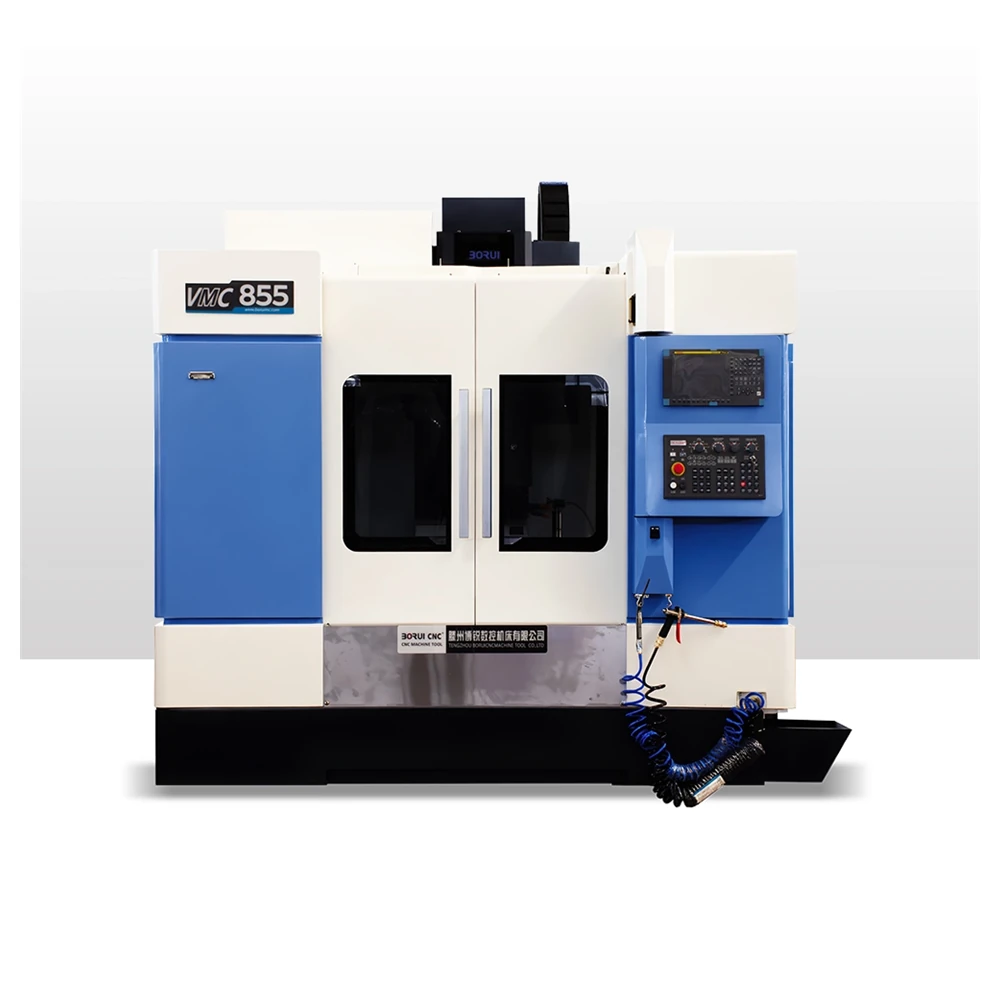
Vertical Machining Center VMC855
A wider 1000×500 mm table, 7.5 kW spindle and a 24-station disc magazine for larger moulds.
View modelA small machine with a serious job: metal mould work. An 800 by 400 mm table, a 650 mm X travel and a fully enclosed BT40 spindle head make the VMC650 quick to set and easy to keep clean, while HIWIN linear guideways and a quenched, vibration-treated bed casting keep it steady in the cut. Add a fourth axis and several faces come off the machine in one setup.
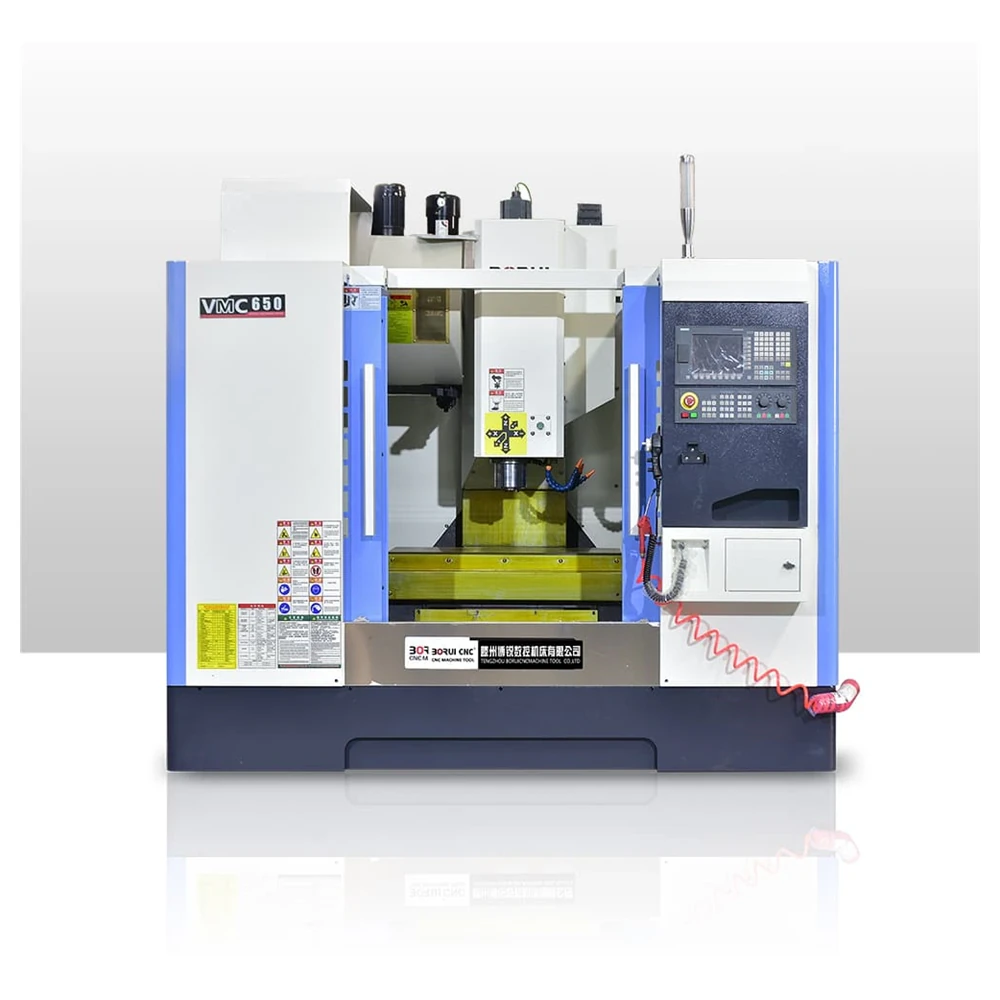
Compact footprint, full enclosure and a table sized for mould plates rather than sheet metal. Three things define how this machine is used.
Full guarding contains chips and coolant, and the quenched, vibration-treated bed with a double-layer saddle keeps noise and vibration low during long cuts.
A rotary fourth axis turns the machine into a four-axis centre, so faces that would need two or three clampings can be finished in a single setup.
HIWIN linear guideways with low clearance and high load capacity, plus 24 m/min rapid traverse, keep the tool in cut and out of the air.
One machine, three spindle speeds and a disc magazine. Choose the rung that matches the tools and the material you actually run.
| Configuration | Spindle speed | Best for | Magazine |
|---|---|---|---|
| Standard | 8000 rpm | General mould and part milling with BT40 tooling | 16-station disc ATC |
| Option A | 10,000 rpm | Smaller cutters and finer surface finish work | 16-station disc ATC |
| Option B | 12,000 rpm | Aluminium and light-alloy finishing at higher speed | 16-station disc ATC |
Spindle speed options and magazine capacity are confirmed on the build sheet. The datasheet describes both a 16-station and a 24-station disc magazine; the parameter table figure is shown above.
Transcribed from the machine parameter table.
| Parameter | Value |
|---|---|
| X axis travel | 650 mm |
| Y axis travel | 400 mm |
| Z axis travel | 500 mm |
| Spindle nose to table | 120–620 mm |
| Spindle centre to column | 550 mm |
| Table size | 800 × 400 mm |
| Table load | 400 kg |
| T-slots | 3 − 18 × 125 mm |
| Spindle speed | 8000 rpm, options to 10,000 / 12,000 rpm |
| Main motor power | 5.5 kW |
| Spindle taper | BT40 (Ø120) |
| Rapid traverse | 24 / 24 / 20 m/min |
| Cutting feed rate | 1–10,000 mm/min |
| Positioning accuracy | ±0.008 mm |
| Repeatability | ±0.005 mm |
| Tool magazine | 16-station disc ATC |
| Machine dimensions | 2400 × 2000 × 2550 mm |
| Machine weight | 4000 kg |
The descriptive text of the datasheet references a 24-station disc magazine while the parameter table lists 16; the parameter table is used above. Control system and spindle option are confirmed before production.
A compact machine only stays accurate if its structure stays still. Three choices in the casting and guideway set do most of that work.
The table size and the fourth axis together decide what this machine is good at.
Mould plates, cavities and cores milled, drilled and finished with BT40 tooling across the full table.
Small inserts and electrodes where the spindle speed option and fine feed control decide the finish.
Tooling plates and fixtures machined four-sided on the rotary axis in a single setup.
Light-alloy housings and brackets cut quickly at the higher spindle speed options.
Mixed part numbers run through one machine, with the disc magazine holding the tools for the whole batch.
Job-shop milling where the part fits the table and the tolerance fits the machine.
Step up in table size with the VMC855, or consider a vertical mill for a different structure at a similar table.
A wider 1000×500 mm table, 7.5 kW spindle and a 24-station disc magazine for larger moulds.
View model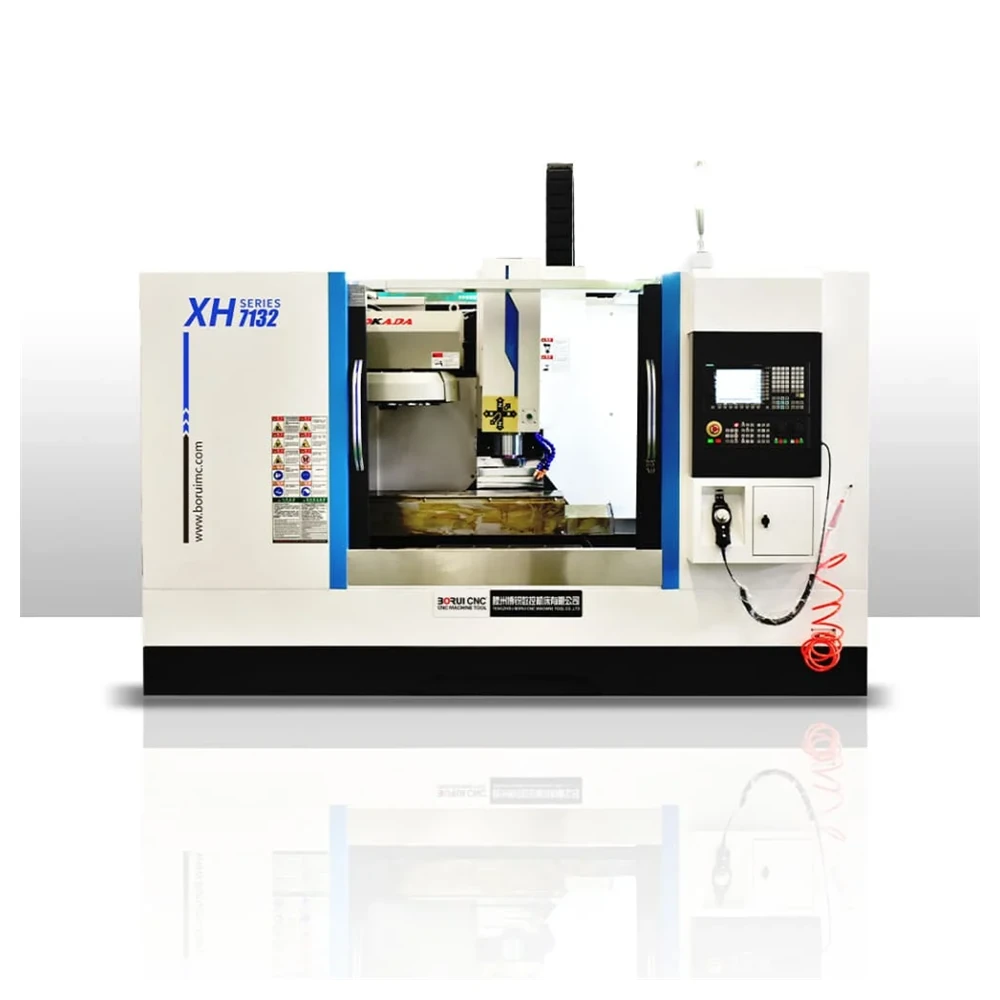
A 1000×320 mm table on a bridge-column mill with hardened box ways for heavy cutting.
View model
When the job is thousands of holes and threads rather than mould surfaces, this is the faster machine.
View modelIt was designed around metal mould work and small to medium machined parts. A 800 by 400 mm table and 650 by 400 by 500 mm travel hold mould plates, inserts, jigs and housings, and the fourth axis option lets several faces be machined in one setup. With a 400 kg table load it also suits small batch production of mixed parts.
The standard spindle is a Taiwan-made unit running at 8000 rpm, with 10,000 and 12,000 rpm options available. It is a BT40 taper with a 120 mm nose. The parameter table specifies a 16-station disc automatic tool changer; the descriptive text of the same datasheet refers to a 24-station magazine, so please confirm the magazine size when ordering.
The bed is a high-density casting that has been quenched twice and vibration treated to stabilise the iron, and the saddle uses a double-layer cast construction that raises the overall stiffness of the bed assembly. That combination is what keeps the machine quiet and low in vibration while holding accuracy through a batch.
Positioning accuracy is plus or minus 0.008 mm with plus or minus 0.005 mm repeatability, and the rapid traverse is 24 m/min in X and Y and 20 m/min in Z, with cutting feeds from 1 to 10,000 mm/min. HIWIN linear guideways with low clearance and high load capacity keep the axes responsive at those speeds.
SIEMENS, KND, FANUC, Mitsubishi and GSK controls are all offered, and the control can be matched to your operators' experience and your programming environment. The selected system ships with an English interface and a parameter set for your parts.
Standard builds ship in 15 to 30 working days after deposit, with customised spindle or control configurations taking 30 to 45 working days. We supply English manuals, parameter files, live video commissioning and operator training, plus lifetime remote support. Volume terms are agreed per order.