Vertical Machining Center VMC650
The compact option for mould plates and small parts in a smaller footprint.
View modelThe VMC855 is the wider, heavier step in the range. A 1000 by 500 mm table and 800 mm X travel take moulds and parts that outgrow the VMC650, while a wide plate-type base, mesh-ribbed castings and roller linear guideways on all five axes keep the machine stable in heavy cutting. It can be ordered three-axis and upgraded, or supplied with fourth and fifth axes for multi-face work in one setup.
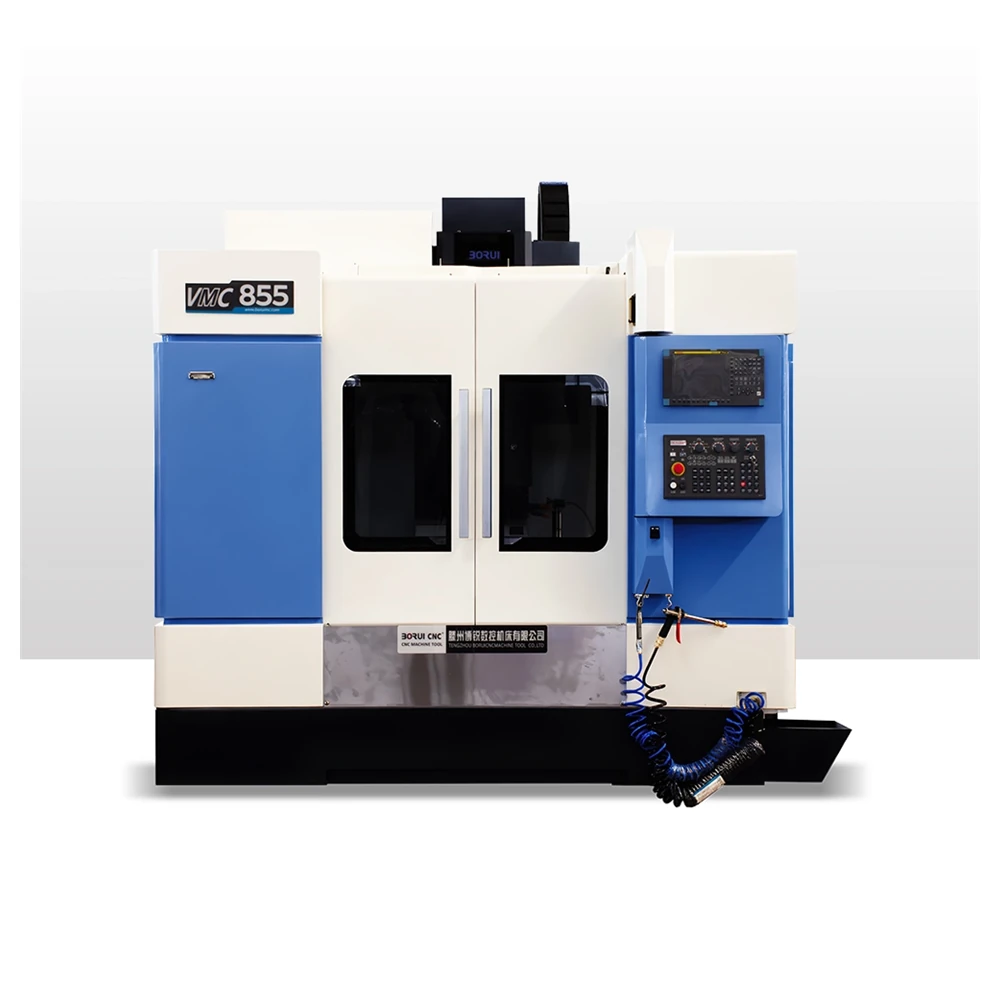
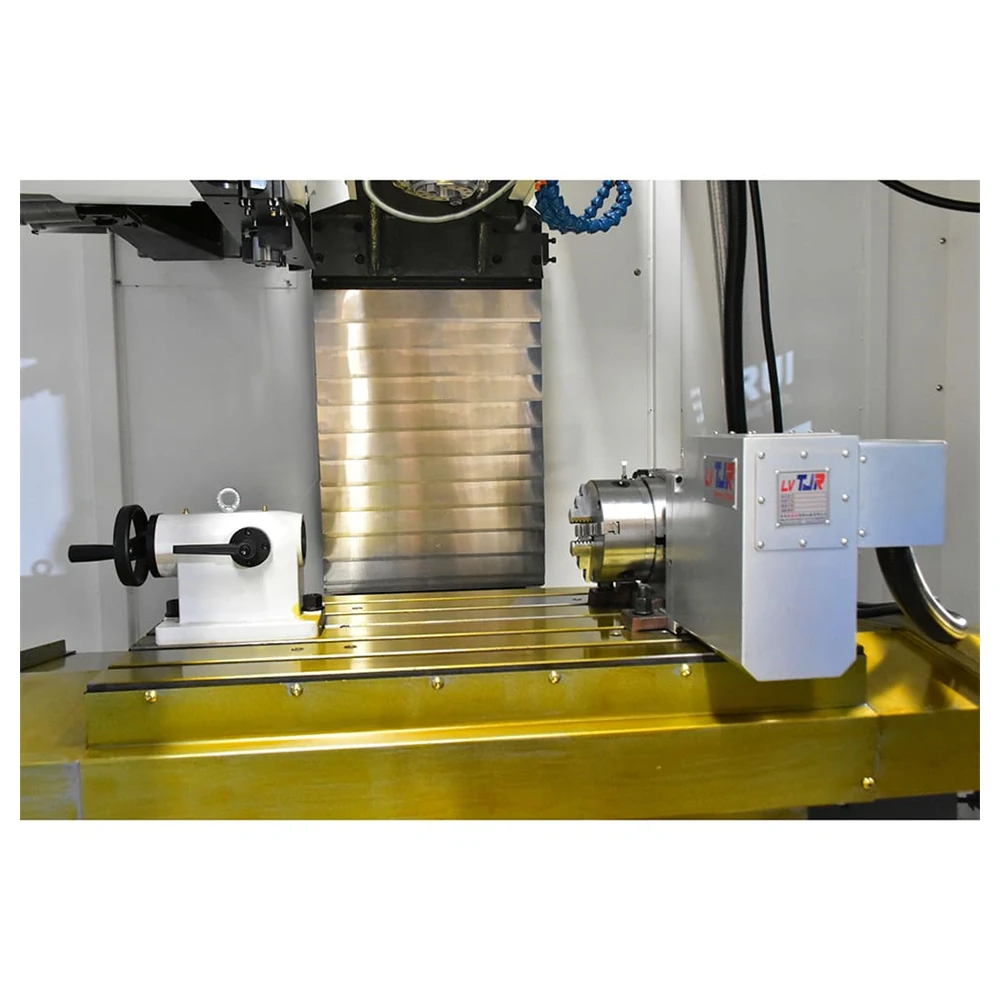
This machine is not a small VMC scaled up. The base, the column and the guideways were chosen at the platform level for five-axis duty, so a three-axis machine ships with the same rigidity that a five-axis job needs.
Three structural decisions separate this machine from a lighter VMC. Each one exists to stop a specific kind of deflection.
The five major castings carry an internal mesh-rib structure, which raises stiffness without adding mass and damps vibration at its source.
Casting in resin sand and tempering produces a uniform iron structure, then vibration and natural aging release the stress that causes long-term drift.
Water at the front, oil at the back, with hidden internal piping. Coolant is handled cleanly and the working area stays clear of exposed lines.
Transcribed from the machine parameter table.
| Parameter | Value |
|---|---|
| X axis travel | 800 mm |
| Y axis travel | 550 mm |
| Z axis travel | 550 mm |
| Spindle nose to table | 140–640 mm |
| Spindle centre to column | 590 mm |
| Table size | 1000 × 500 mm |
| Table load | 500 kg |
| T-slots | 3 − 18 × 130 mm |
| Spindle speed | 8000 rpm, options to 10,000 / 12,000 rpm, stepless |
| Main motor power | 7.5 kW |
| Spindle taper | BT40 (Ø150) |
| Axis servo motors | 2 × 2 × 3 kW |
| Rapid traverse | 24 / 24 / 20 m/min (up to 48 m/min on five-axis rapid positioning) |
| Cutting feed rate | 1–10,000 mm/min |
| Positioning accuracy | ±0.008 mm |
| Repeatability | ±0.005 mm |
| Tool magazine | 24-station disc ATC |
| Machine dimensions | 2600 × 2300 × 2580 mm |
| Machine weight | 5000 kg |
The datasheet lists both a general axis rapid traverse and a higher five-axis rapid positioning figure; both are shown. Control system, spindle speed option and axis configuration are confirmed on the build sheet before production.
The value of a fourth and fifth axis is not the axes themselves — it is the setups that never happen.
The part is set on the table or the rotary fixture and datumed a single time for the whole job.
The rotary axes bring each face to the spindle, up to 48 m/min between positions on five-axis rapid moves.
Faces, holes, pockets and profiles that would each have needed their own fixture are cut in one continuous program.
No re-datuming, no re-clamping error and no queue time waiting for a second machine to finish the part.
One multi-face setup replaces two or three single-face setups, so fixture cost and setup time both fall.
Features cut from one datum hold their relationship to each other far better than features cut across separate clampings.
Longer single-setup cycles mean more spindle-on time and less time spent at the bench re-fixturing parts.
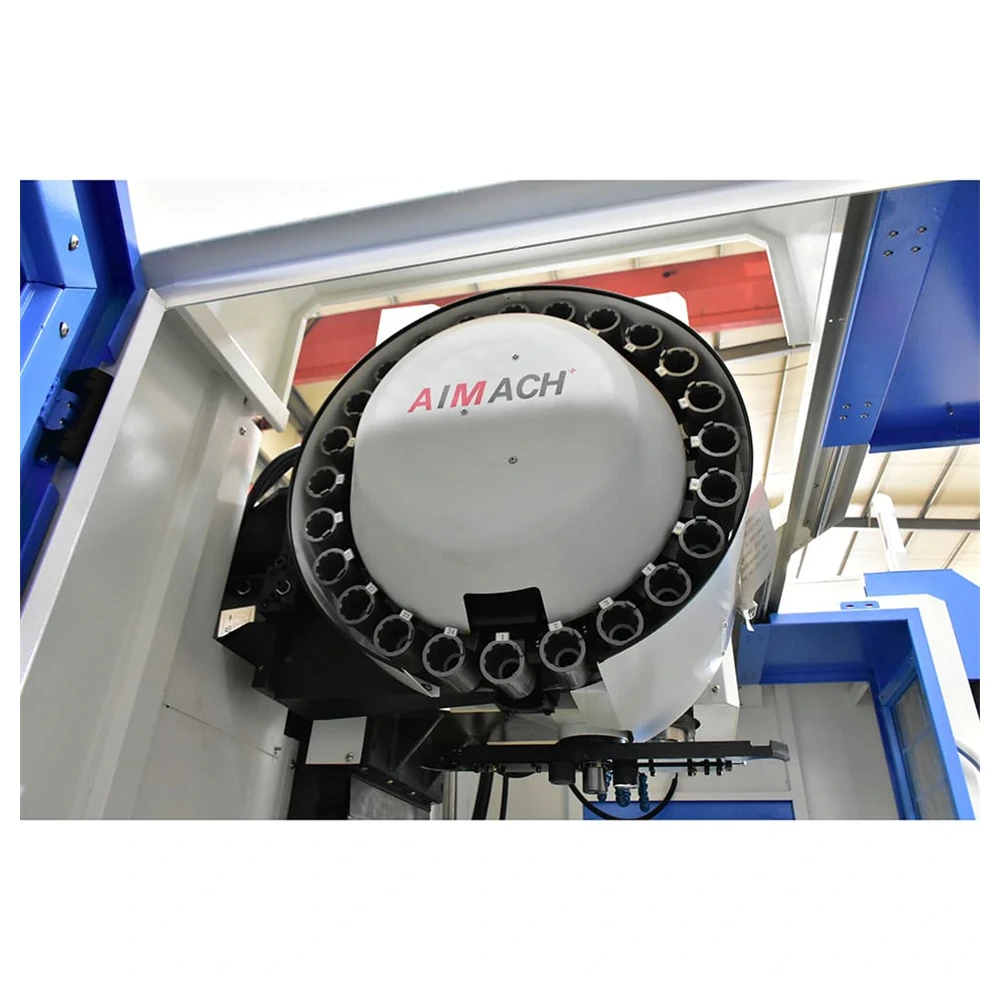
Complex parts need many tools, and every tool change is time the spindle is not cutting. A 24-station magazine with a 1.9 second change keeps that dead time small.
Parts that are one size up from what a compact VMC can hold, or that need several faces at once.
Larger moulds, cavities and cores that outgrow a 800 by 400 mm table but do not need gantry capacity.
Machined housings, bracketry and frame components needing multiple faces and hole patterns.
Drivetrain and structural parts machined in small to medium batches with the full tool set resident.
Tooling plates and fixtures machined on several faces, which is where the rotary axes pay back fastest.
Valve bodies and manifold blocks with bores and ports on multiple faces at a single datum.
Mixed subcontract work where the machine has to move between part numbers quickly.
A smaller table, a longer table, or a machine built for holes rather than surfaces.
The compact option for mould plates and small parts in a smaller footprint.
View model
A 1250 mm table for elongated parts on a vertical mill platform rather than a machining centre.
View model
A high-speed machine for parts defined by hole count and thread count rather than by surface.
View modelThe machine is built on a five-axis-capable platform: all five axes use roller linear guideways, the base is a wide plate type and the column is a heavy one-piece casting. It can be supplied with a fourth and fifth axis fitted so that multiple faces are machined in a single setup, or ordered as a three-axis machine and upgraded later.
Roller types have a larger contact area than the ball type commonly used on machines at this size, so they carry heavier loads with less deflection and stay stable in heavy cutting. The guideways are supplied by Taiwan PMI or HIWIN, which keeps accuracy and rigidity consistent across the whole axis set.
The castings are poured to the HT300A+ formula, moulded in resin sand and tempered, then vibration aged and naturally aged to release internal stress. Released stress is what would otherwise show up as slow distortion over the first years of service, so the aging process is what protects long-term accuracy and part consistency.
The body uses an oil-water separation design with water at the front and oil at the back, and the piping is routed internally rather than across the outside of the machine. That keeps the bed area clear, makes cleaning simpler and reduces the chance of leaks or damage to exposed lines.
The VMC855 uses a 24-station disc automatic tool changer with a change time of 1.9 seconds. A larger magazine means fewer interruptions on complex jobs, and the short change time keeps the non-cutting portion of the cycle small on parts that need many different tools.
Standard builds ship in 15 to 30 working days after deposit, and customised axis or control configurations take 30 to 45 working days. The machine arrives with English manuals and a parameter set, and we support levelling, commissioning and operator training on site or over video. Volume terms are agreed per order.