Vertical Machining Center VMC650
A compact four-axis machining centre with HIWIN linear guideways and a 16-station disc magazine for moulds and metal parts.
View modelWhere a general machining centre spends its cycle moving, the BR600 spends it cutting. A 20,000 rpm direct-drive spindle, a 1.6 second tool-to-tool change and 1.3 G acceleration on all three axes turn a part with dozens of holes and threads into a short, repeatable cycle. It is a compact machine with a high-end FANUC 31i-B control, built for aluminium, copper electrodes and small steel parts.
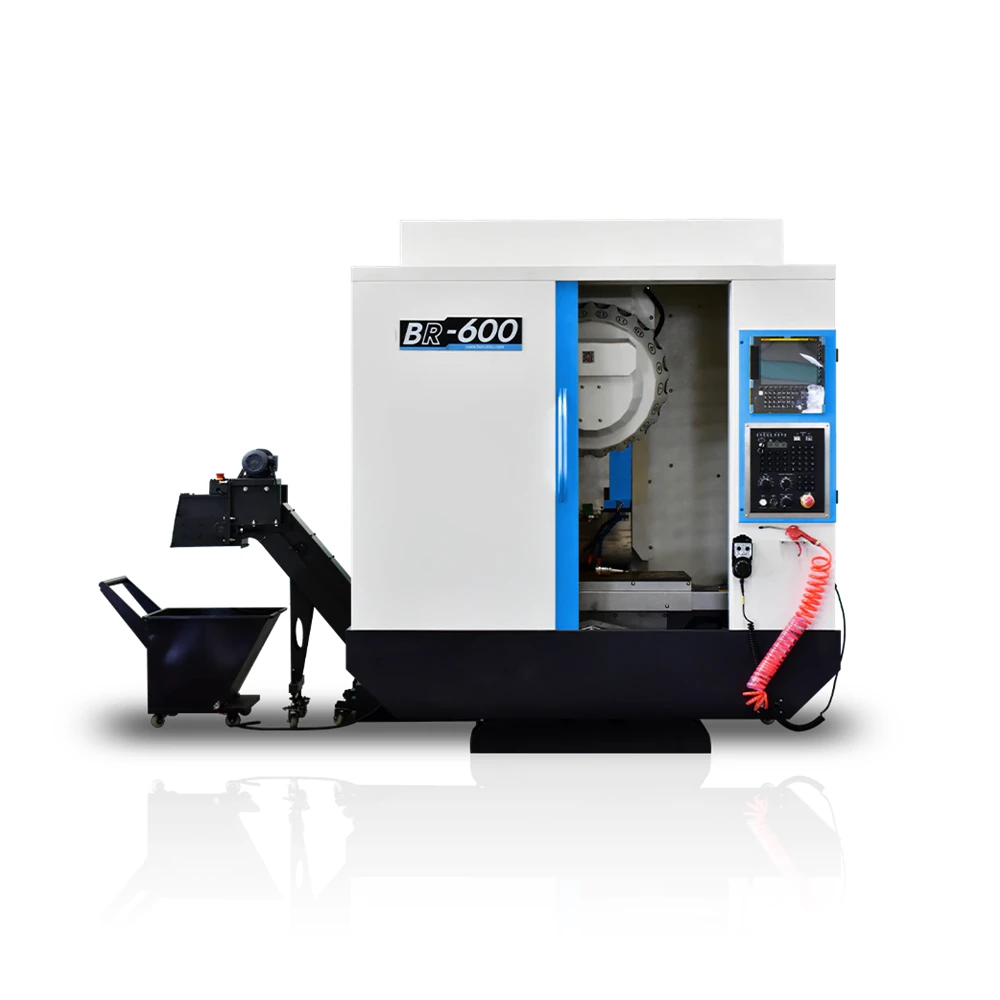
Small parts are won or lost on cycle time. A part with forty holes and twenty tapped threads spends almost all of a conventional cycle accelerating, decelerating and waiting for tool changes. The BR600 was laid out to remove exactly that lost time.
The datasheet prints the two builds in one table. The BR600 is listed below with the larger BR700 alongside it, in case your part grows.
| Parameter | BR600 | BR700 |
|---|---|---|
| X axis travel | 600 mm | 700 mm |
| Y axis travel | 400 mm | 400 mm |
| Z axis travel | 350 mm | 350 mm |
| Spindle nose to table | 135–485 mm | 135–485 mm |
| Spindle speed | 20,000 rpm | 20,000 rpm |
| Tool magazine capacity | 16 (21 optional) | 16 (21 optional) |
| Max tool diameter | 50 mm (120 mm adjacent) | 50 mm (120 mm adjacent) |
| Max tool length | 250 mm | 250 mm |
| Max tool weight | 3 kg | 3 kg |
| Tool change (T-T) | 1.6 s | 1.6 s |
| Spindle power (30 min duty) | 3.7 / 5.5 kW | 5.5 / 7.5 kW |
| Axis motor power X/Y/Z | 1.5 / 1.5 / 3.0 kW | 1.5 / 1.5 / 3.0 kW |
| Table size | 700 × 420 mm | 700 × 420 mm |
| Table T-slots | 3 × 14 × 125 mm | 3 × 18 mm |
| Table load | 300 kg | 300 kg |
| Rapid traverse X/Y/Z | 48 / 48 / 48 m/min | 48 / 48 / 48 m/min |
| Cutting feed rate | 5–20,000 mm/min | 5–20,000 mm/min |
| Positioning accuracy | ±0.003 / 300 mm | ±0.003 / 300 mm |
| Repeatability | ±0.005 / 300 mm | ±0.005 / 300 mm |
| Machine weight | 3500 kg | 4500 kg |
| Power requirement | 20 kVA | 20 kVA |
| Coolant tank | 210 L | 210 L |
| Compressed air | 6–8 kg/cm² | 6–8 kg/cm² |
| Dimensions | 2220 × 1900 × 2300 mm | 2320 × 1900 × 2300 mm |
Figures above are transcribed from the machine parameter table. The descriptive text of the same datasheet also refers to 10,000 rpm and 24,000 rpm spindle variants and an 11 kW / 3.7 kW spindle rating, while the parameter table lists a single 20,000 rpm figure and the 3.7 / 5.5 kW rating used above. Please confirm the spindle option and control version for your order.
Four figures set the beat of the cycle, and four steps repeat for every hole on the part.
Nano-level encoder feedback locates the part origin, and AI thermal compensation applies the correction before the first hole.
1.3 G acceleration and 48 m/min rapid put each drill at the next position in a fraction of a second, with cutting feed to 20,000 mm/min.
A 1.6 s tool-to-tool change brings the tap in, and the raised low-speed torque drives it cleanly through steel and aluminium alike.
AI contour control II and HRV control smooth the surface on any light milling, contouring or chamfering that the cycle also requires.
Four points that separate this machine from an entry-level drill-tap centre.
A FANUC 31i-B system rather than an entry-level 0i class control, giving far greater program capacity at fine unit precision.
Motor-to-spindle direct coupling with high-speed, low-heat bearings and grease lubrication for minimal maintenance.
Three-axis AI thermal-displacement compensation is standard, holding tolerance through long unattended runs.
Real four and five-axis simultaneous machining, not the indexing systems some drill-tap centres market as multi-axis.
High-speed three-dimensional machining of small parts, moulds and electrodes, plus deburring and chamfering of castings.
Copper electrode and mobile-phone mould machining, where high spindle speed and fine interpolation produce sharp internal corners.
High-speed, high-accuracy 3D machining of resin patterns, precision components and small mould inserts.
Aluminium and other light metals cut at speed, together with electrical parts and small stainless components.
Magnesium injection mouldings, die castings and forgings cleaned up, deburred and chamfered as a finishing operation.
A BR600 is configured to your part, then tested before it leaves the factory.
Sea and air freight with full export packing, trackable from the factory door and arranged to your destination port.
Control version, spindle option, tool magazine size, coolant and chip handling confirmed on a signed build sheet.
24-month warranty on core components, with lifetime remote engineering support for the life of the machine.
English manuals, parameter files and live video commissioning, with operator training on the FANUC control.
The BR600 is built for parts with many holes and threads on a compact footprint: aluminium and light-metal housings, mobile-phone moulds and copper electrodes, precision 3D parts and moulds, and small stainless components. It also deburrs and chamfers magnesium injection mouldings, die castings and forgings.
Tool-to-tool change time is 1.6 seconds, and all three axes accelerate at up to 1.3 G with a 48 m/min rapid traverse. Combined with high-speed control and optimum-torque acceleration, the machine spends more of each cycle cutting and less of it repositioning.
It runs a FANUC 31i-B CNC system. With the unit precision set to 0.001 mm the program capacity is several times larger than on a basic control, and the minimum setting unit can be 0.0005 mm. Options include nano interpolation, AI contour control II, impact control, NURBS interpolation, nano smoothing and a high-speed data server.
Yes. The spindle is rated 3.7 kW continuous and 5.5 kW for 30-minute duty from the parameter table, with a direct-drive connection to the spindle. The datasheet also quotes a torque increase of 32 percent in the low-speed range, from 53 N·m to 70 N·m, which supports short roughing and boring passes between drilling and tapping operations.
Three-axis AI thermal-displacement compensation corrects the growth of the spindle and feed axes, and a high-resolution pulse encoder interpolates and feeds back at nanometre level. Positioning accuracy is plus or minus 0.003 mm per 300 mm with plus or minus 0.005 mm repeatability, and the structure is designed for 24-hour, 30-day continuous running.
Standard builds ship in 15 to 30 working days after deposit. Every machine is geometrically tested and run before packing. We supply English manuals, the parameter file, live video commissioning and operator training, plus lifetime remote technical support. Volume terms are agreed per order.
If the part is larger than a drilling and tapping centre can hold, step up to a vertical machining centre or a gantry mill.
A compact four-axis machining centre with HIWIN linear guideways and a 16-station disc magazine for moulds and metal parts.
View model
A bridge-column vertical mill with hardened box ways and a pre-tensioned ball screw drive for stiffer heavy cutting.
View model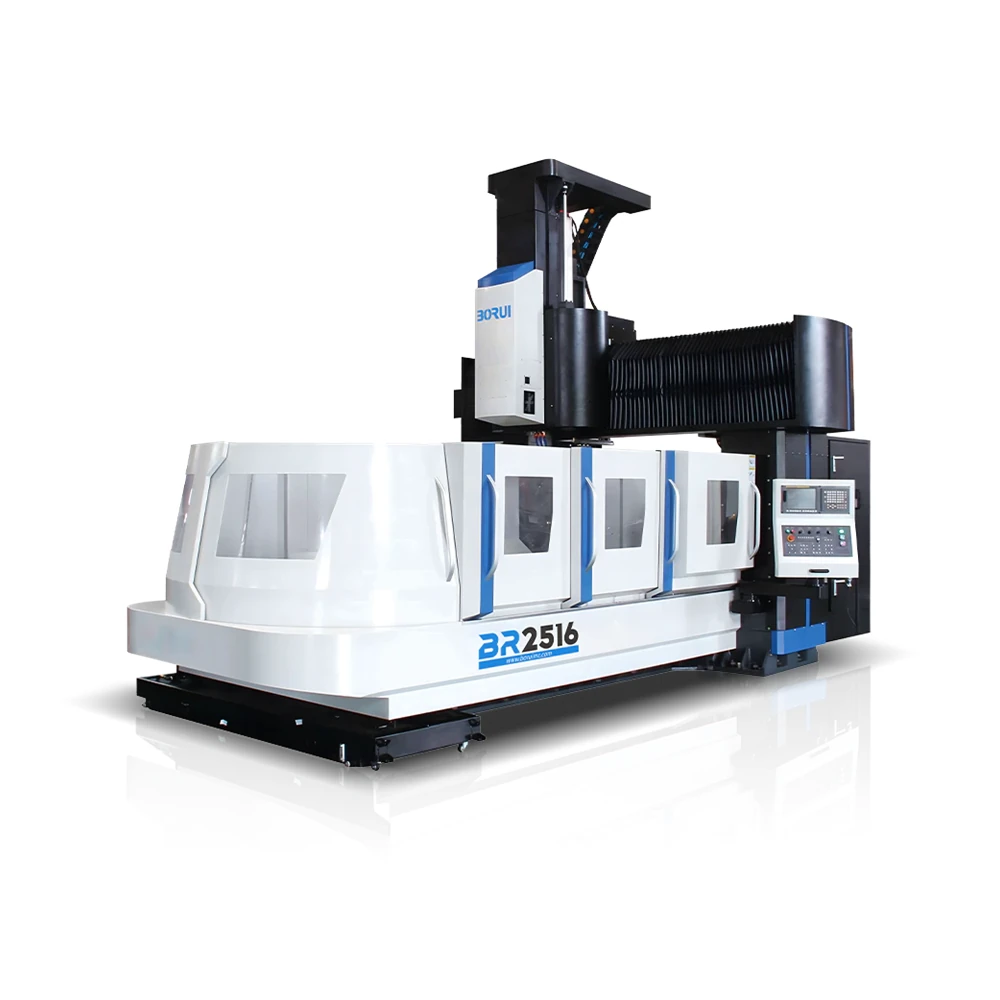
A 2500 mm gantry bed carrying 5 tonnes, with a 24-station disc ATC and 15/18.5 kW BT50 spindle for large parts.
View model