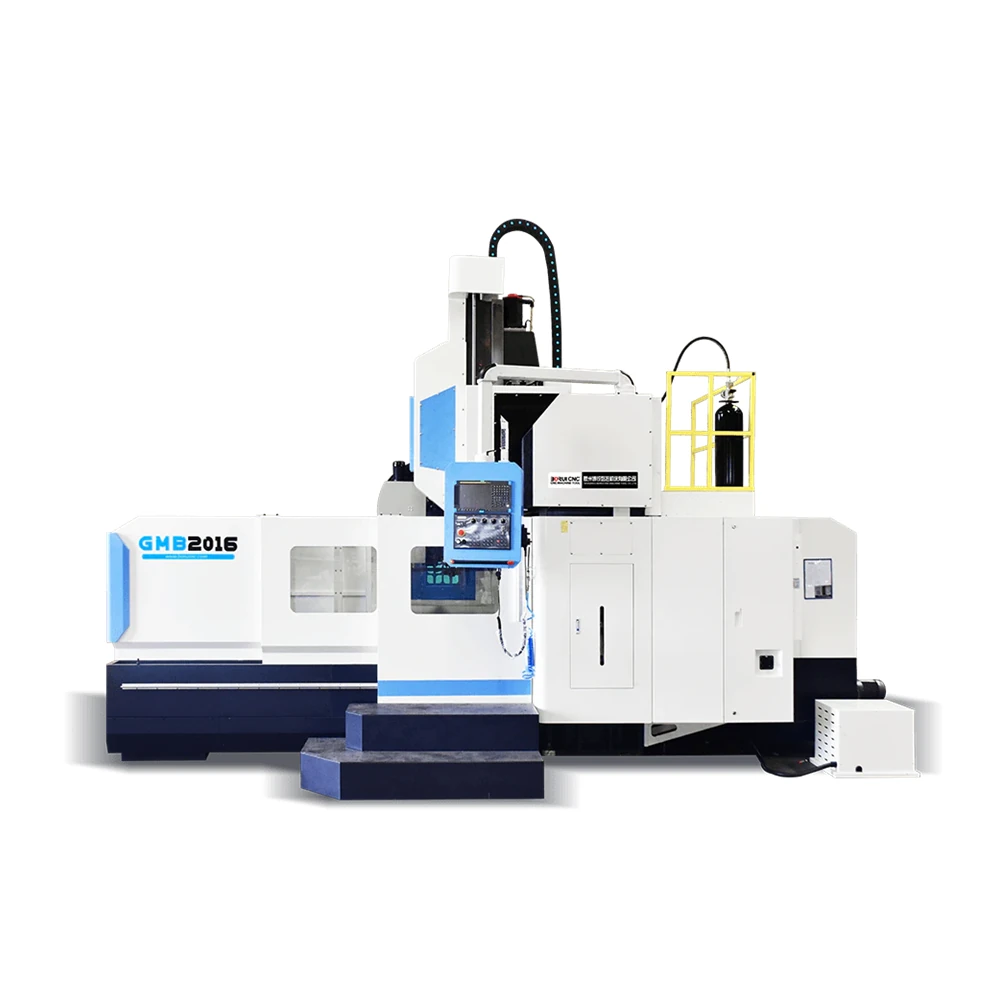
Gantry CNC Milling Machine GMB2016
A moving-column gantry with 3000 and 4000 mm table builds and a 24-arm tool changer for even larger work.
View modelWhen the part is too heavy to sit on a moving table, the table stops moving. The BR2516 fixes a 2500 by 1300 mm bed and carries the spindle over it on a double-column bridge, so a five-tonne casting stays clamped exactly where it was set. A resin-sand cast, hand-scraped structure, a 15/18.5 kW BT50 spindle and a 24-station disc changer handle milling, boring and drilling in one setup.
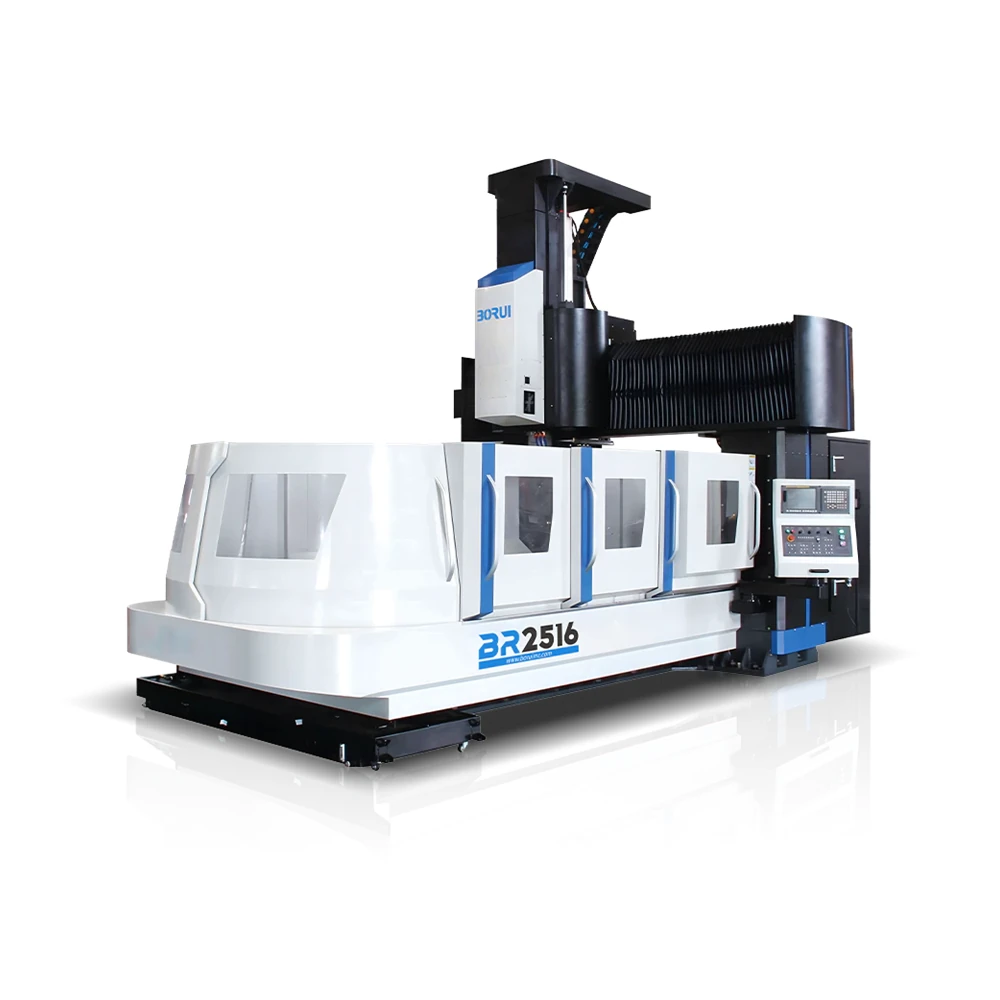
Column machines move the workpiece; gantry machines move the tool. That single change is what allows the BR2516 to hold a five-tonne casting without the table sagging, deflecting or losing its datum between operations.
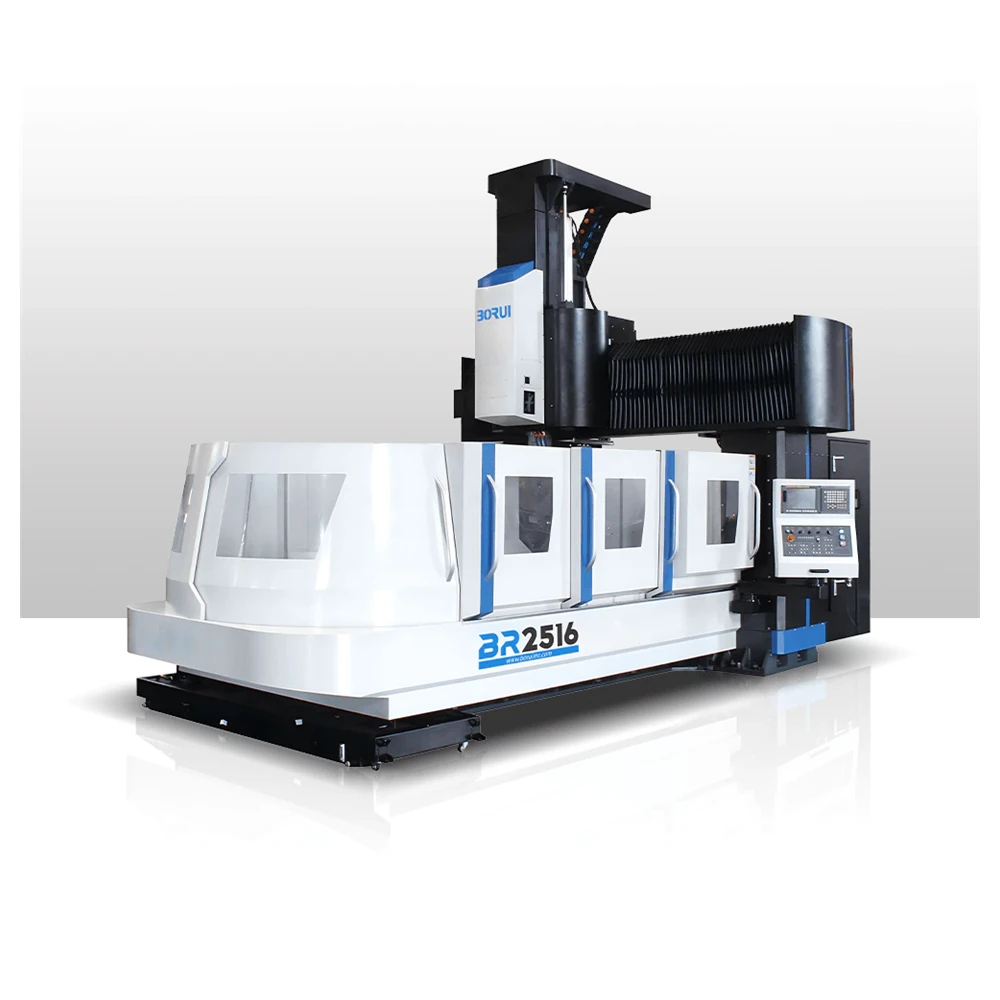
On a gantry mill the numbers that decide capacity are not just travel — they are the distances between the columns, the ram cross-section and the rail class.
A 1650 mm Y travel across a 1300 mm table lets a single long part be repositioned for several setups without leaving the machine.
The Z axis runs on a hard-way T-slot ram rather than a rail, which is the stiffer choice for plunging cuts into cast iron and steel.
X and Y use paired 55 mm roller guides in P class, quality-hardened and precision-ground for rigidity and long service under heavy loads.
Every figure below is transcribed from the machine parameter table.
| Parameter | Value |
|---|---|
| X axis travel | 2500 mm |
| Y axis travel | 1650 mm |
| Z axis travel | 750 mm |
| Spindle nose to table | 150–900 mm |
| Table size | 2500 × 1300 mm |
| Table load | 5 t |
| T-slots | 22 × 180 × 7 mm |
| Spindle speed | 6000 rpm, stepless within range |
| Spindle taper | BT50 |
| Spindle power | 15 / 18.5 kW |
| Spindle torque | 236 N·m |
| X / Y guideway | 55 × 2 roller guide, P class |
| Z axis | T-slot ram on hard ways |
| Ball screw accuracy | C3 class |
| Ball screw diameter X/Y/Z | 63 / 50 / 50 mm |
| Screw lead, all axes | 10 mm |
| Motor coupling | Direct coupled |
| X / Y axis motor | bis 40 N·m |
| Z axis motor | bis 40 N·m with brake, nitrogen balanced |
| Rapid traverse X / Y / Z | 15,000 / 15,000 / 12,000 mm/min |
| Cutting feed rate | 0–10,000 mm/min, three axes simultaneous |
| Max tool length / diameter / weight | 300 mm / Ø100 mm / 15 kg |
| Tool change time | 6 s |
| Positioning accuracy | 0.010 / 1000 mm |
| Repeatability | 0.006 / 1000 mm |
| Minimum input increment | 0.001 mm |
| Power capacity | 55 kVA |
| Net weight | 19 t, double-layer structure |
| Packing size | 7200 × 3900 × 3500 mm |
The datasheet lists the tooling figures (300 mm length, Ø100 mm diameter, 15 kg, BT50) as options. Control system, spindle option and tooling package are confirmed against your drawing before production.
The three axes are not built the same way. This is deliberate — each one is chosen for the load it actually carries.
| Axis | Guideway | Ball screw | Motor | Rapid |
|---|---|---|---|---|
| X (gantry travel) | 55 × 2 roller guide, P class | Ø63 mm, C3, 10 mm lead | bis 40 N·m servo | 15,000 mm/min |
| Y (cross rail) | 55 × 2 roller guide, P class | Ø50 mm, C3, 10 mm lead | bis 40 N·m servo | 15,000 mm/min |
| Z (ram) | T-slot ram on hard ways | Ø50 mm, C3, 10 mm lead | bis 40 N·m servo with brake | 12,000 mm/min |
Ball screws are directly coupled to the servos with preloaded bearings at each end — six on X, six on Y and five on Z — removing backlash and keeping the screw in tension.
A lubrication circuit feeds every drive, cutting friction and wear, while the scraped ways hold oil in their pockets so the guides stay lubricated through long cuts.
A nitrogen balance cylinder offsets the weight of the spindle head, so the Z servo works against cutting force rather than gravity, which is what protects high-speed, high-accuracy Z moves.
Gantry work is rarely delicate. The structure and the tooling package are sized for roughing as much as finishing.
Enough stiffness to resist cutting and torsional loads, with the structural damping that keeps a heavy cut from marking the surface.
Hand scraping produces a wider, more accurate bearing surface, so the machine holds geometry under load instead of deflecting into the cut.
The X, Y and Z servos interpolate together, so contours, radii and large bores are cut in one continuous pass.
AI contour control, nano smoothing and arc-corner functions produce a surface that needs less hand finishing after the machine.
Work that is defined by size and weight rather than by tolerance alone.
Base castings, slide beds and machine frames milled, drilled and bored flat in a single clamping.
Large mould bases, bolster plates and die plates with many drilled, tapped and bored stations across the face.
Fabricated frames and weldments machined after welding, when distortion makes re-clamping on a small machine impractical.
Gearbox housings, bearing pedestals and heavy plant components typical of the energy and heavy-equipment sectors.
Long structural components that need several faces and hole patterns machined to a common datum.
Subcontract machining where the machine has to accept whatever arrives next, from a plate to a casting.
Smaller parts are faster on a vertical machine; even larger work suits the moving-column GMB2016.
A moving-column gantry with 3000 and 4000 mm table builds and a 24-arm tool changer for even larger work.
View model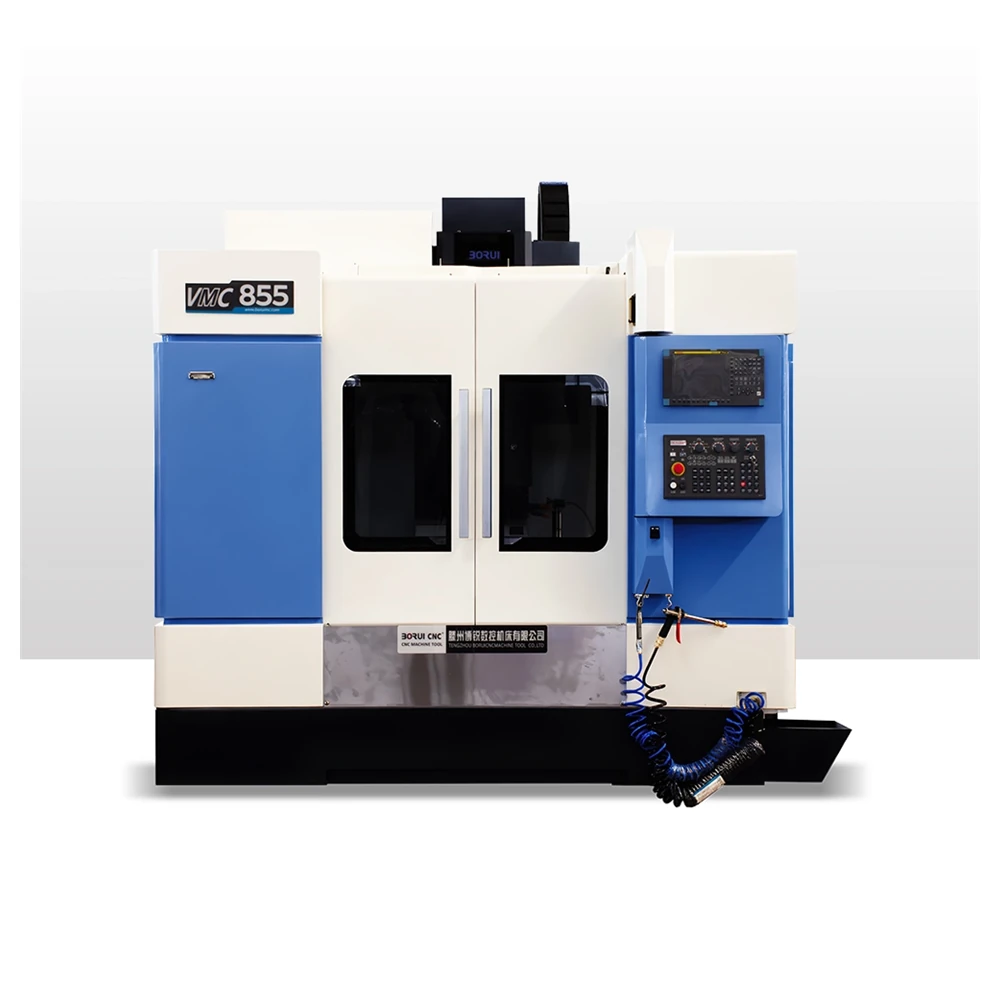
A faster, compact alternative for parts up to about 800 mm that do not need the gantry bed.
View model
The opposite end of the range: a high-speed machine for small parts with many holes and threads.
View modelThe table measures 2500 by 1300 mm and is rated to a 5 tonne load, with travel of 2500 mm in X, 1650 mm in Y and 750 mm in Z. The spindle nose reaches from 150 to 900 mm above the table, so tall castings and weldments fit as well as large plates. Parts that would be too heavy or too large to clamp on a column machine belong here.
Resin-sand casting gives a dense, uniform iron structure that absorbs cutting vibration, and the hand-scraping of the guideways produces a large, accurate contact area between the sliding surfaces. The scraped surface also holds lubricating oil in fine pockets, which keeps the guideways lubricated, reduces friction and extends their working life under heavy cutting loads.
The spindle is a BT50 unit rated 15 kW continuous and 18.5 kW peak, delivering up to 236 N·m of torque at speeds up to 6000 rpm with stepless variation across the range. A 24-station disc automatic tool changer swaps tools in about 6 seconds and accepts tools up to 300 mm long, 100 mm in diameter and 15 kg in weight.
The machine can be supplied with SIEMENS, KND, FANUC, MITSUBISHI or GSK controls depending on your preference and your operators' experience. The configuration shown in the datasheet uses FANUC 0i MF Plus with AICC2, nano smoothing, arc corner and mirror machining functions, and a bilingual 10.4 inch colour display.
At a net weight of 19 tonnes in the double-layer structure, the machine is packed to 7200 by 3900 by 3500 mm and shipped by sea freight. We supply the full export documentation, and our engineers support the levelling, commissioning and accuracy verification on site or over video.
Standard gantry builds ship in 30 to 45 working days after deposit, and more heavily customised travel or spindle configurations take longer. Each machine is geometrically checked and test cut before packing, and the inspection record ships with it. Volume terms are agreed per order.