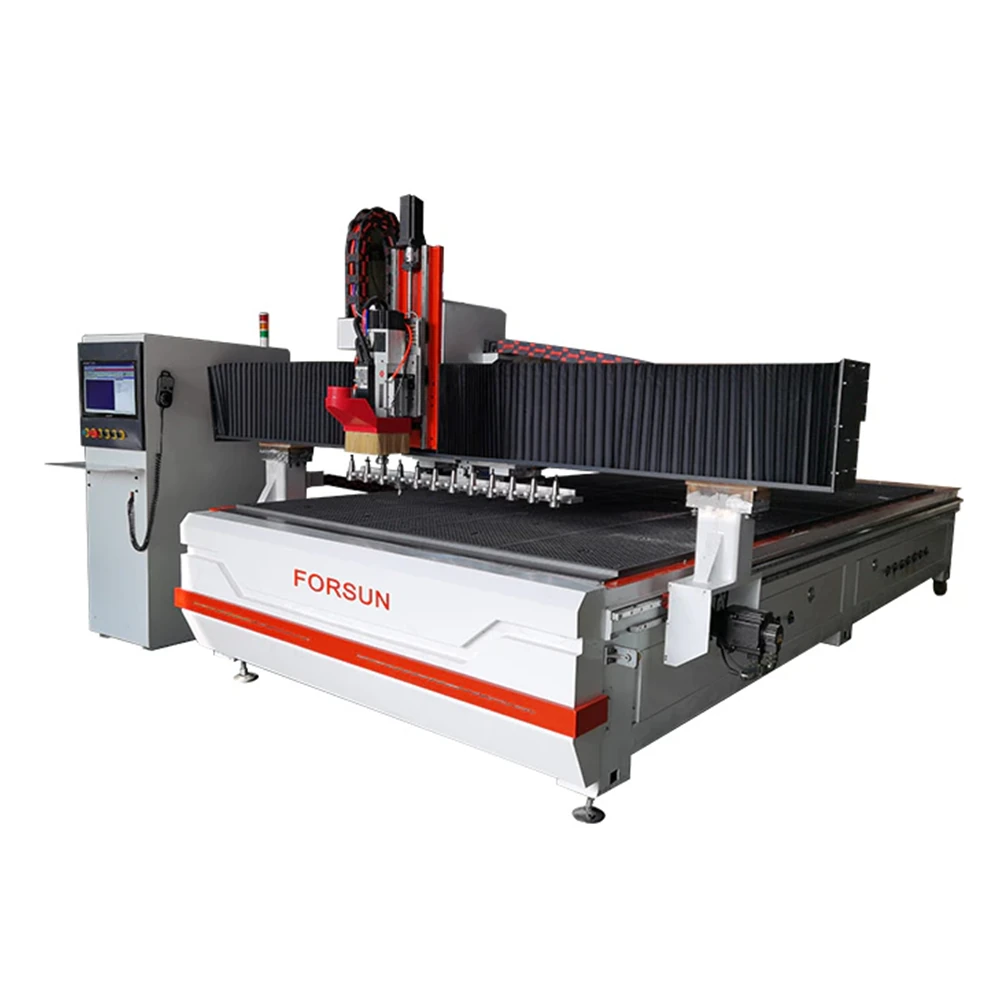
Woodworking ATC CNC Router
The same ATC platform with a 2000×4000 mm table for larger sheets and full-height door panels.
View modelThe 1300 by 2500 mm sheet is the format most workshops buy their board in, and it is the format this machine is built around. A 9 kW automatic tool change spindle, a 10-station linear magazine and a combination vacuum and T-slot table let a nested job be engraved, cut, milled, grooved and hollowed in one automated sequence — without an operator stopping the machine to swap a cutter.
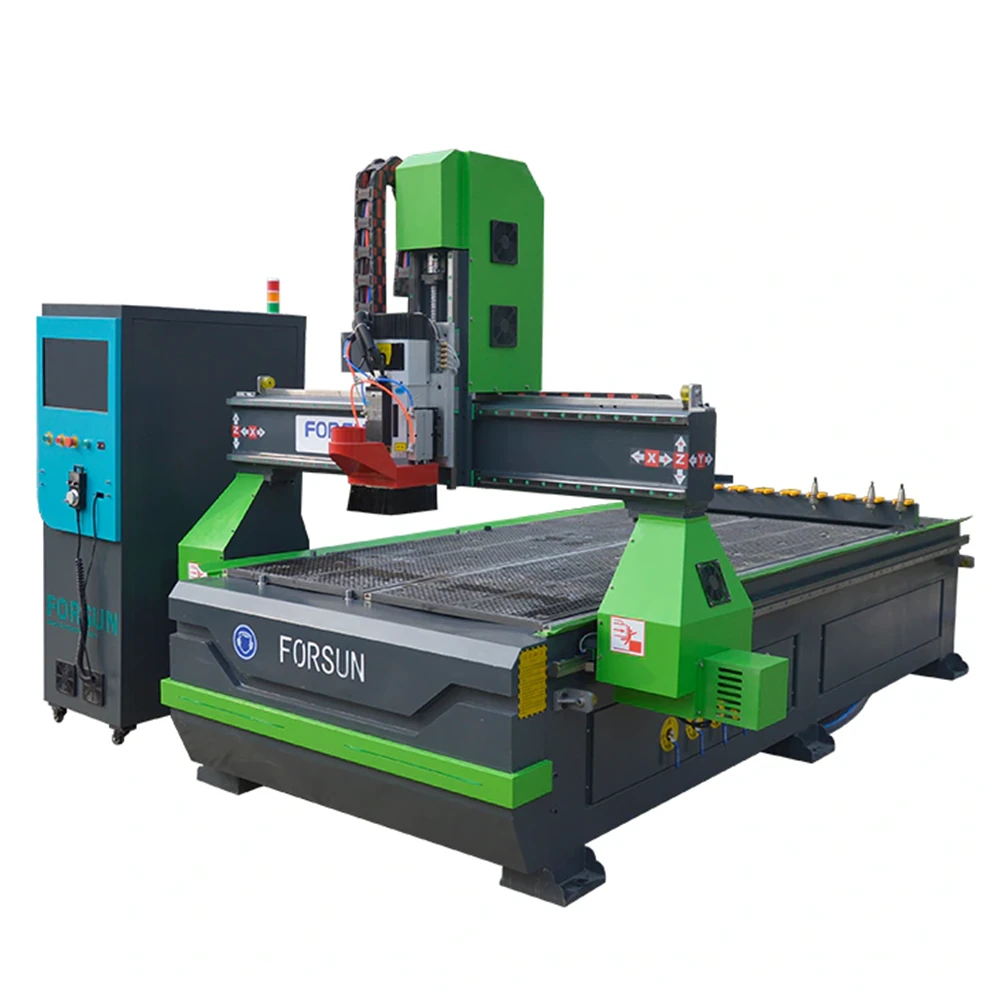
Automatic tool change is often the feature that pushes a router out of reach. This machine puts it on the standard 4 by 8 foot platform, using the same spindle, magazine and drive set as the larger models.
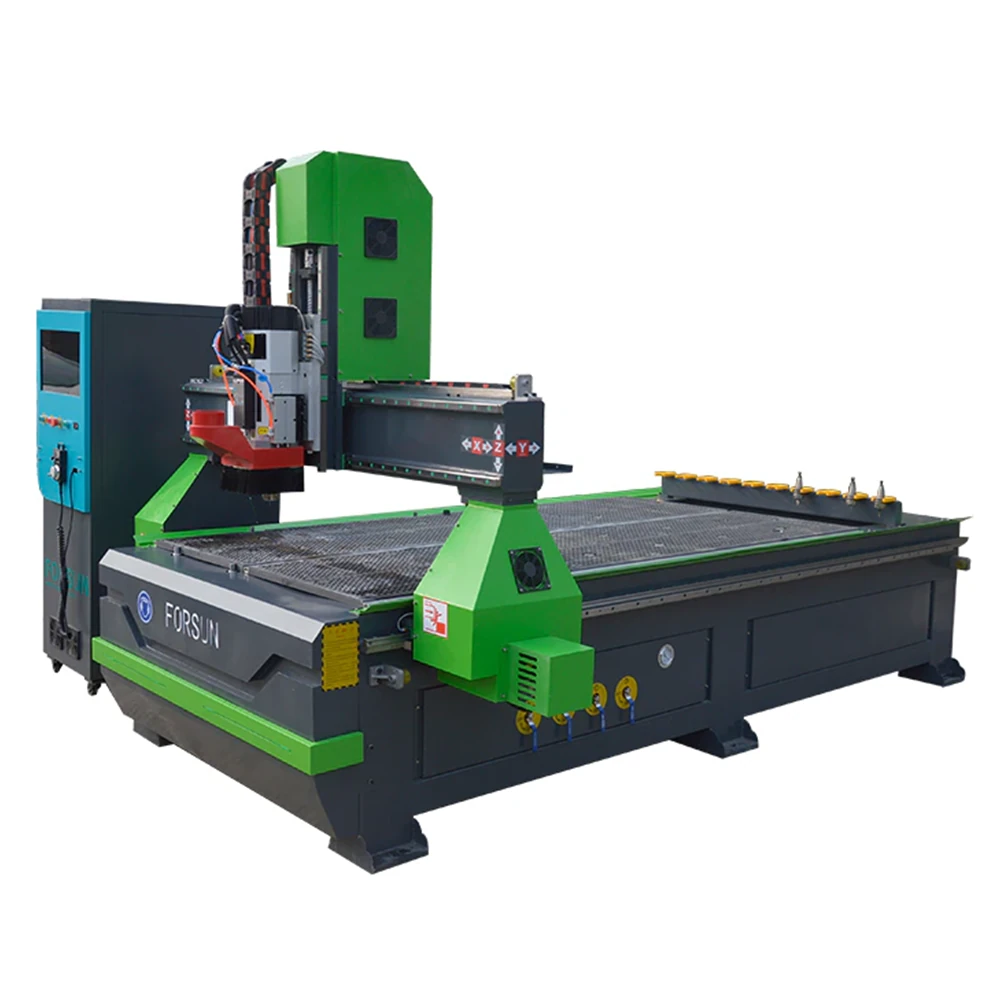
Two clamping systems in one table. Which one you use follows directly from the material on the bed.
For nested sheet work. Vacuum suction holds full panels flat and evenly across the bed, so thin boards do not lift or chatter, and the whole sheet can be released and changed in seconds. Suction cups can be repositioned quickly for different panel sizes.
For solid parts, thicker blocks and jigs that cannot be held by suction. Standard T-slot clamps and a machined aluminium T-slot plate give a rigid mechanical hold, so heavy cutting on solid stock is secure without vacuum pumps running.
Transcribed from the machine parameter table.
| Parameter | Value |
|---|---|
| X and Y travel | 1300 × 2500 mm (4 × 8 ft); options 2000 × 3000 mm, 1500 × 3000 mm, 2000 × 4000 mm |
| Z travel | 200 mm; options 300 / 400 / 500 / 600 mm |
| Spindle | 9.0 kW ATC, 24,000 rpm, ISO30, ER32 |
| Tool magazine | 10-station linear ATC; disc magazine option |
| Automatic push-off | Available as an option |
| Axis motors | YAKO servo motors |
| Reducer | Japanese Shimpo reducer |
| X and Y drive | Helical rack and pinion |
| Z drive | High-precision ball screw |
| Guideways | HIWIN / THK linear rails and blocks |
| Body structure | Cast steel table structure with side supports |
| Table | Combination vacuum and T-slot table, aluminium T-slot plate |
| Voltage | 220V or 380V, 50–60 Hz three phase |
| Command language | G code and M code |
| Control | DHTN; options Syntec / SIEMENS / DSP |
| Lubrication | Automatic |
| Tool setting | Automatic tool sensor |
| Dust extraction | 3.0 kW dual-bag system |
| Collets | ISO30, 4 / 6 / 1/8 / 1/9 in |
| Maximum rapid | 80,000 mm/min |
| Maximum machining speed | 45,000 mm/min |
| Repeatability | ±0.04 mm / 300 mm |
| Machining accuracy | ±0.03 mm / 300 mm |
| Gross weight | 2500 kg |
Table size, Z travel, magazine type and control system are confirmed before production, and the automatic push-off device is an option. Design files from Type3, Ucancam, Artcam, Alphacam, Vectric, EnRoute, Mastercam and Cabinet Vision are supported.
Four steps replace what would otherwise be an operator, a spanner and a lost ten minutes per tool change.
The program calls the next tool. The spindle moves to the linear magazine and picks it up from its numbered position.
The previous cutter is placed back in its own station, so the magazine stays organised and every offset stays valid.
Engraving, cutting, milling, grooving or hollowing runs at the speed and feed stored for that tool.
The sequence continues until the part is complete, so the whole nested job runs unattended from one sheet to the next.
The tool magazine is separate from the spindle, so tool positions do not depend on the head position.
Every change is commanded by the job program, which keeps the sequence consistent between operators and shifts.
A disc magazine can be fitted instead of the linear unit where floor space or tool layout makes it the better choice.
Work where the sheet format fits the bed and the tool list fits the magazine.
Large panel engraving, solid wood furniture, solid wood artistic lettering and carved components.
MDF paint-free door engraving, cabinet door and window carving produced from nested sheets.
Wooden patterns, aviation patterns, propellers and automotive foam models carved from board.
Acrylic, two-colour plate, PVC, ABS and aluminium composite engraving and cutting, plus signs and badges.
Gifts, ornaments, wooden toys, metal relief work and copper and aluminium lettering.
Pattern engraving for musical instruments, and cutting and processing of plastic and timber for packaging.
What is fixed, what can be changed and what to confirm before the build starts.
Standard 1300 by 2500 mm, with larger working areas available where the sheet or the part demands it.
10-station linear magazine as standard, with a disc magazine available as an alternative.
Two-year warranty on main components, with remote engineering support for the life of the machine.
Video commissioning and operator training, with English documentation and the software settings for your parts.
Step up in table size, or move to a twin-head or rotary machine for a different production pattern.
The same ATC platform with a 2000×4000 mm table for larger sheets and full-height door panels.
View model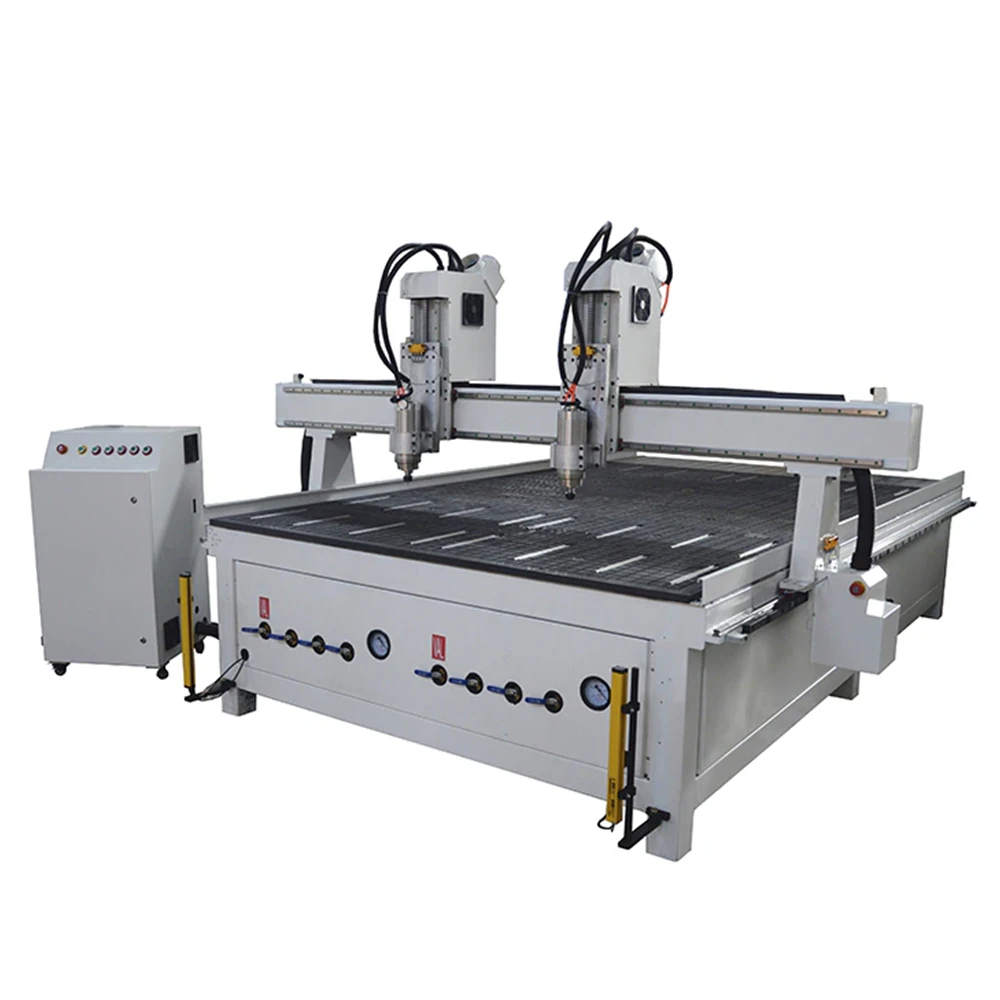
Two heads cutting at once when throughput matters more than automatic tool change.
View model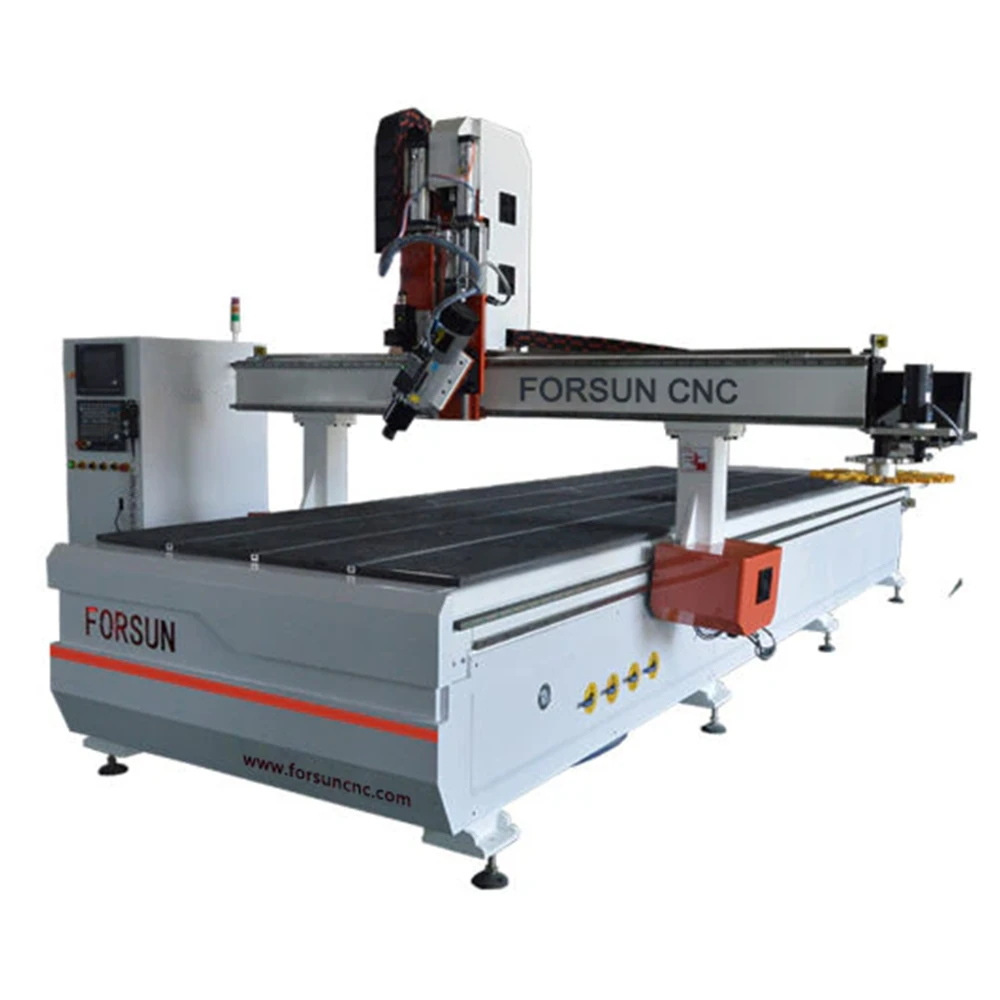
A rotary head for curved and cylindrical work instead of flat sheet production.
View modelWorking area and cost. The 1325 works a 1300 by 2500 mm sheet, which is the standard 4 by 8 foot panel that most cabinet and signage workshops buy their board in, and it uses the same 9 kW ATC spindle, 10-station linear magazine and drive system as the larger machines. It is the value-focused way onto an automatic tool change platform.
It removes the manual tool change from the middle of the cycle. The machine picks up each cutter from the 10-station linear magazine, machines its operation, returns it and picks up the next one, all from the program. Engraving, cutting, milling, grooving and hollowing are completed in a single automated sequence instead of a series of stopped and restarted steps.
The table provides both vacuum clamping and T-slots. Vacuum holds large flat panels firmly and evenly, which is what a nested sheet job needs, while the T-slots allow mechanical clamps for solid parts, jigs and thicker blocks that vacuum cannot grip. One machine therefore handles both sheet material and solid stock without a separate fixture.
X and Y use helical rack and pinion, Z uses a high-precision ball screw, and the axes run on HIWIN or THK linear rails, driven by YAKO servo motors with a Japanese Shimpo reducer. The standard control is DHTN, with Syntec, SIEMENS and DSP also available. G code and M code are supported.
Wood and board stock including plywood, softwood, hardwood, MDF and particle board; plastics such as acrylic, ABS, HDPE, PVC and UHMW; stone and ceramics; soft metals including aluminium, brass, copper and low carbon steel; and composite panels. The tooling and feeds are matched to the material on the machine program.
Standard builds ship in 15 to 30 working days after deposit, with customised table sizes or control configurations taking 30 to 45 working days. Main components carry a two-year warranty, and production capacity is 30 sets per month. Volume terms are agreed per order.